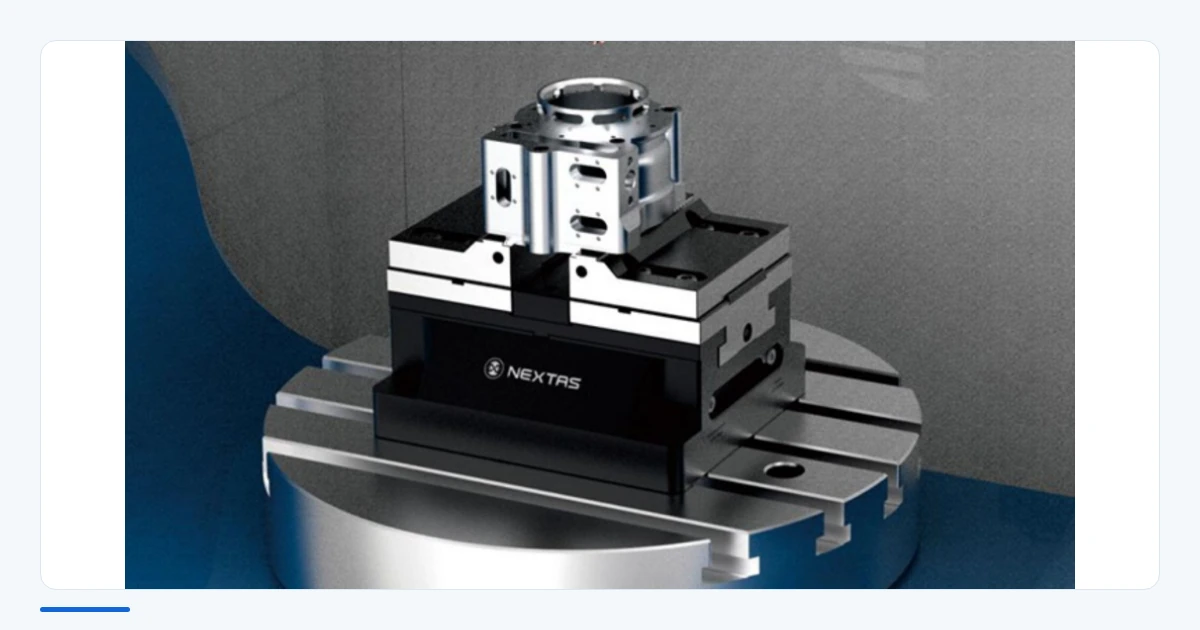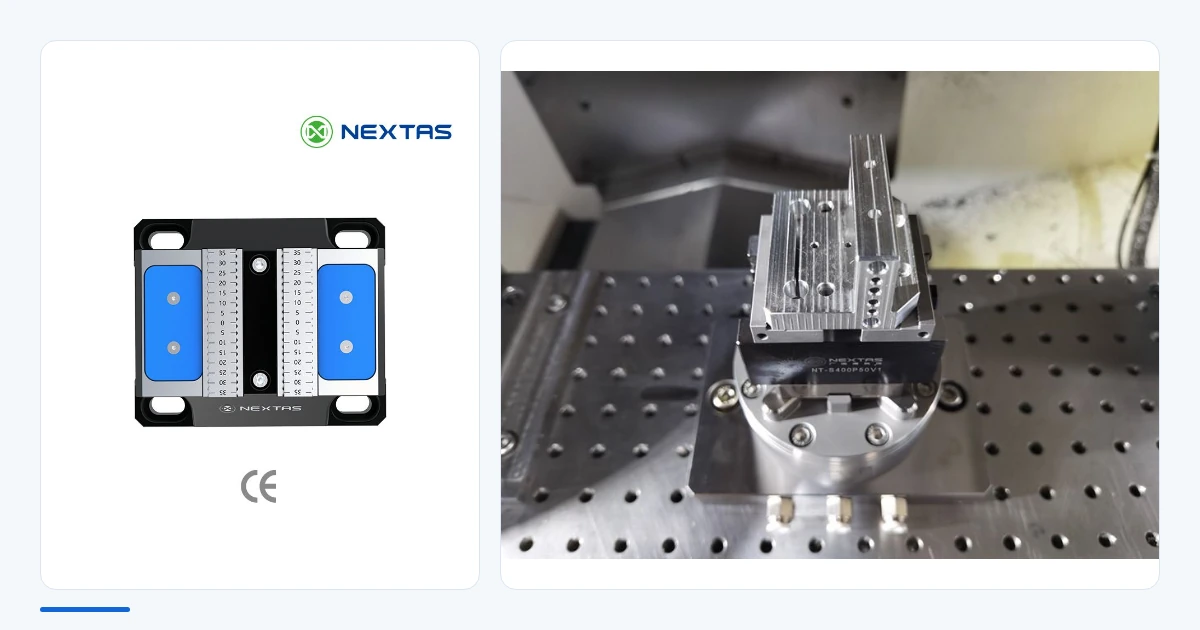
Draw the clamp sketch first
Start with the part drawing and the stock size that actually arrives. Mark what hits a jaw, what must stay clear, how much the stock size can wander, and the room left for the cutter and the probe.
A self-centering vise moves both jaws toward the middle. That helps the centerline when the blank changes size. The finished datum still comes from the jaw faces and the contact you actually have.
If the stock runs large on one side, the jaws still have to close on it, and the probe still needs a path to the face you will use. Put that on the sketch before you compare P75 with P110.
P75, P110, and P150
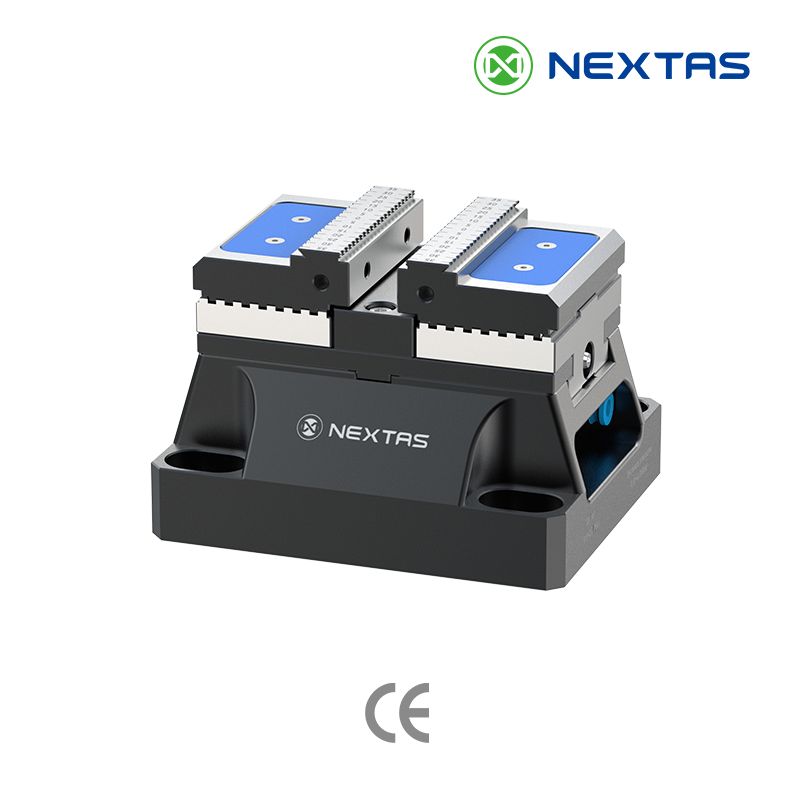
The pneumatic vise page lists these three models. The same figures are here.
| Series and model | Clamping range | Clamp force | Working pressure | Weight |
|---|---|---|---|---|
| P75 — NT-S75P75V1 | 0–125 mm | 4,200 N | 0.5–0.8 MPa | 7 kg |
| P110 — NT-S110P110V1 | 0–200 mm | 12,000 N | 0.5–0.8 MPa | 23.2 kg |
| P150 — NT-S150P150V1 | 0–250 mm | 20,000 N | 0.5–0.8 MPa | 41.6 kg |
Repeat clamping accuracy <0.01 mm is the body spec on these three models. It is not the tolerance of the finished part.
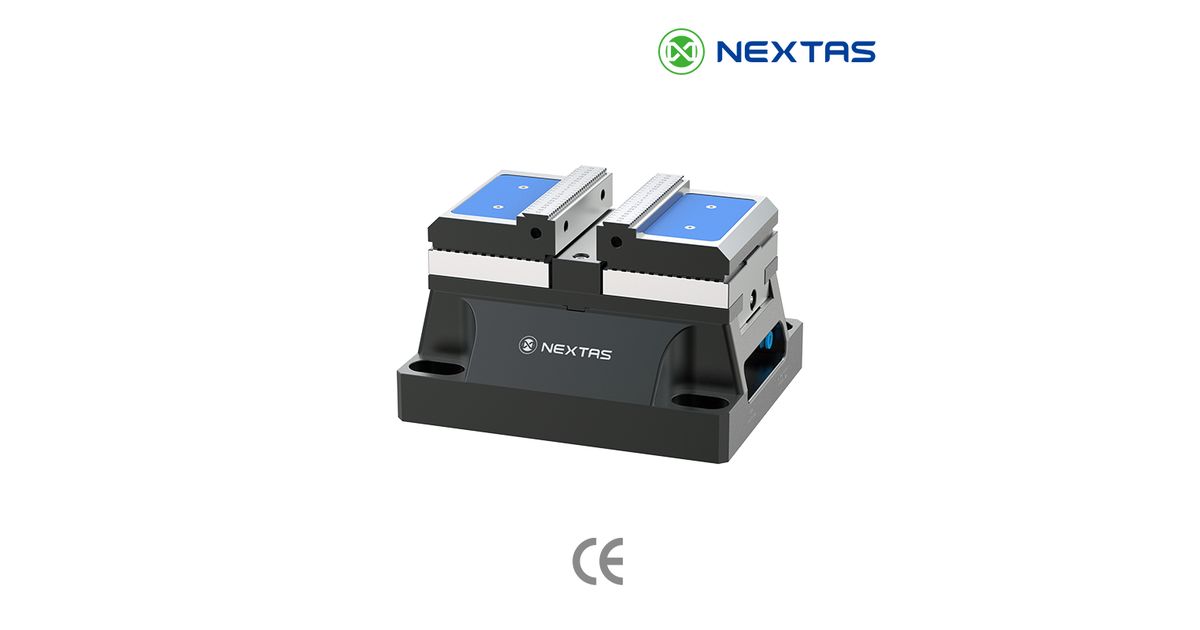
Choose the row whose opening and force fit the sketch. A larger body can get in the way of a short tool.
A 28-second product view of a NEXTAS pneumatic vise; use the page specifications and engineering review for force, pressure, and integration decisions.
Watch on YouTube
A 28-second look at the vise.
Enough force, read at the inlet
The force has to hold the cut without crushing a thin wall. Use the lowest force that already passed a real cut on this part.
Read the pressure at the vise inlet. The catalog range is 0.5–0.8 MPa.
A valve command means the valve moved. It does not mean the part is clamped.
Information for your quotation request
Send the details you already have; mark anything still to be confirmed:
- the part and the jaw contact
- the machine table
- the tool path
- the inlet pressure
- whether loading is manual or automatic
- the feature you will accept the job on
The model table is on the pneumatic vise page. The quote form is on the contact page.
V2 is hydraulic, not a second air vise
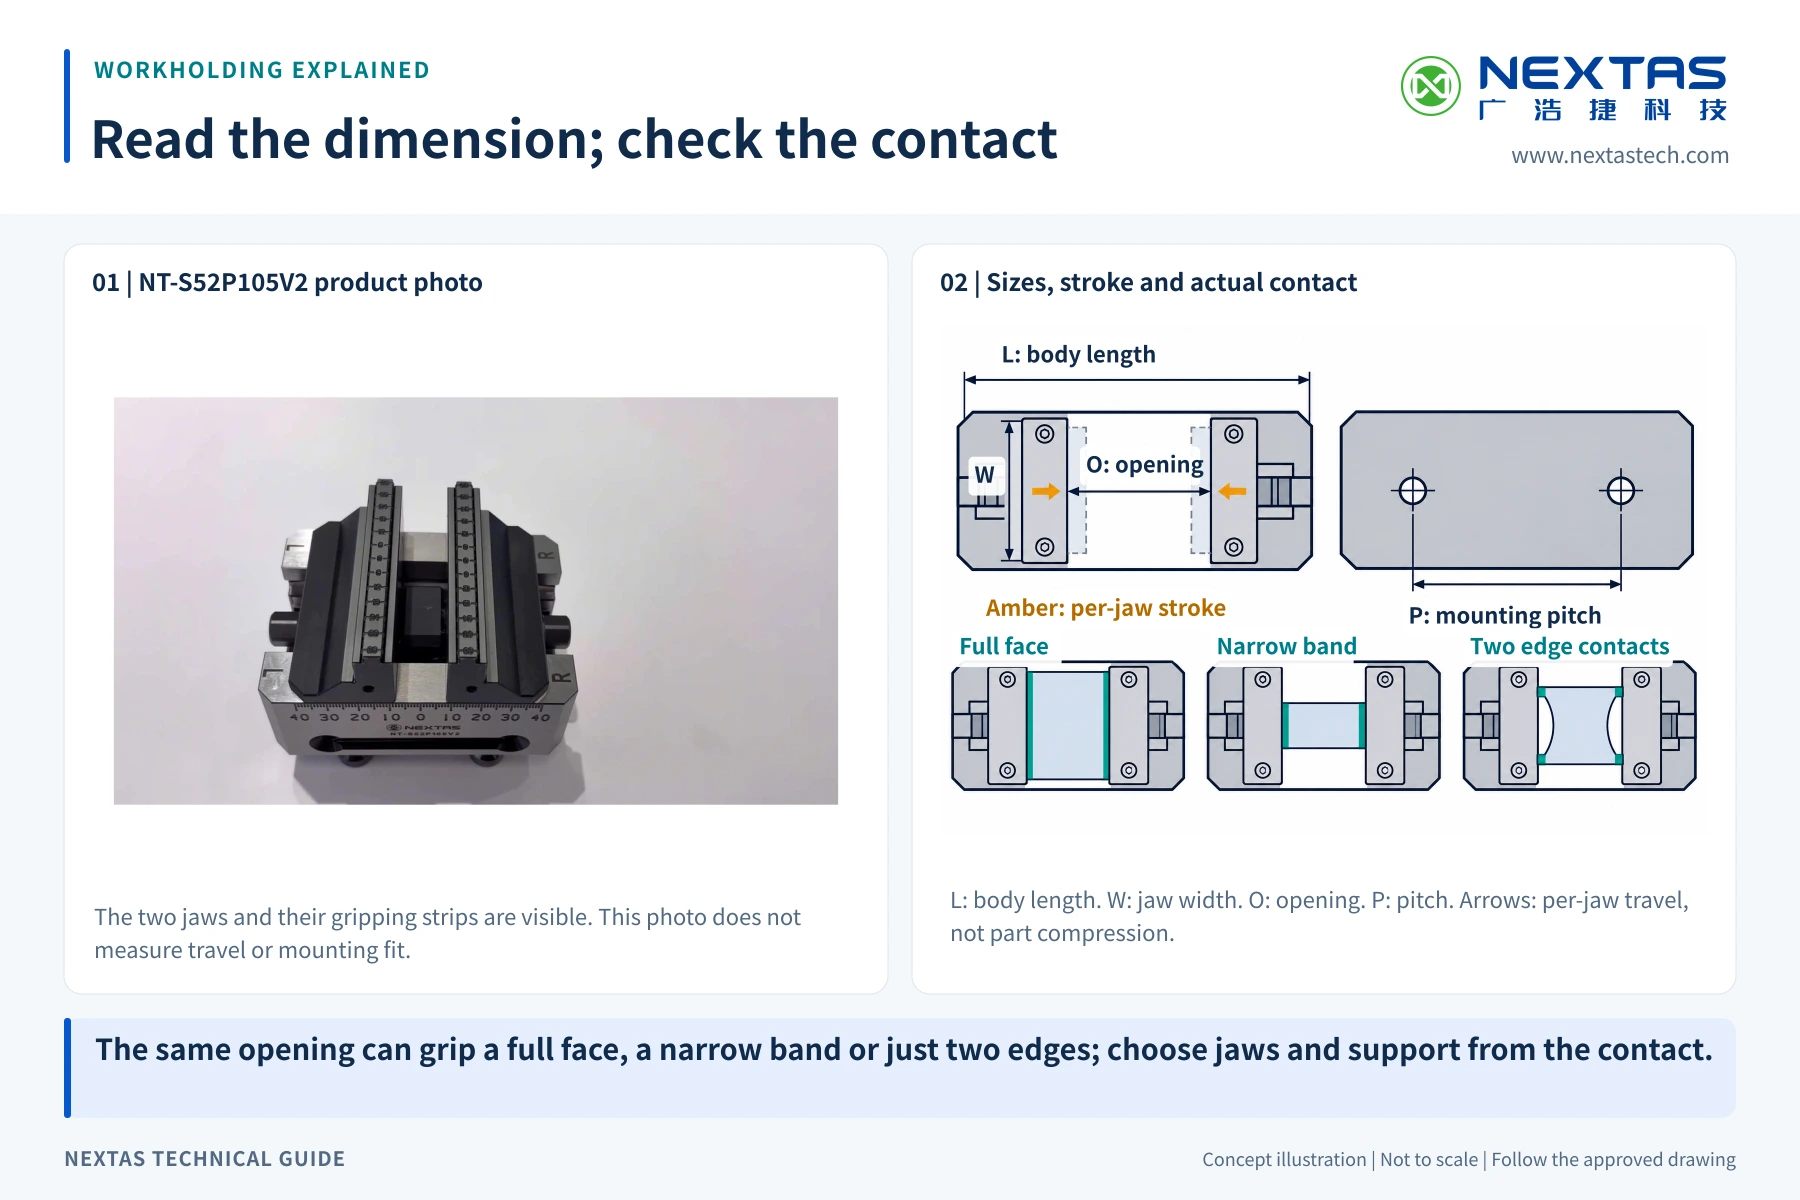
V1 is pneumatic at 0.5–0.8 MPa. V2 is hydraulic at 6 MPa, with the same three body sizes and corresponding jaw openings. Catalogue page 40 lists 2.5 mm stroke per jaw; this is jaw travel, not compression of the part.
| Model | Actuation | Force | Pressure | Weight |
|---|---|---|---|---|
| NT-S75P75V2 | Hydraulic | 9,000 N | 6 MPa | 7.4 kg |
| NT-S110P110V2 | Hydraulic | 30,000 N | 6 MPa | 24.9 kg |
| NT-S150P150V2 | Hydraulic | 45,000 N | 6 MPa | 42 kg |
Jaw contact before the first cut
Draw the jaw contact and check the machine and tool clearances before choosing a body size. On a long or ribbed part, mark whether the jaws contact a full face, a band or two edges. If contact is too short, review the jaws or supports before moving to a larger vise.
The window is not the contact
Use the jaw-opening range to check whether the blank fits. Then use the contact sketch to check where clamping force reaches the part and whether the cutter can reach the required faces. Select force and operating pressure from the same exact V1 or V2 model row.
Before production release, record the accepted contact sketch, pressure measured at the vise port and exact V1 or V2 model. Check seating and clamping on the first piece. A manifold gauge or valve command does not replace these checks.
Find the right pneumatic vise for your part
Tell us your machine model and what you need to hold. Add a part sketch, drawing or photo if available; NEXTAS can help narrow the vise size and jaw arrangement before preparing a quotation.
Discuss my vise setupOr open the pneumatic vise page first.
Selection and quotation questions
Is <0.01 mm the finished-part tolerance?
No. Repeat clamping accuracy <0.01 mm is the body spec on P75, P110, and P150.
Where do I read the air pressure?
At the vise inlet. The catalog working pressure is 0.5–0.8 MPa.
Does a valve command mean the part is clamped?
No. The valve moved. The part still has to be seated and held.