
Frequent fixture changes
Zero-Point Clamping Systems
Prepare the next fixture off the machine. Swap complete setups on a shared receiver-module interface.
Explore zero-point systemsCNC workholding manufacturer · Zhuhai, China
Reduce setup time with zero-point systems, 5-axis vises and custom fixtures. Our engineers review your machine, part and inspection requirements to recommend a practical configuration.
View all products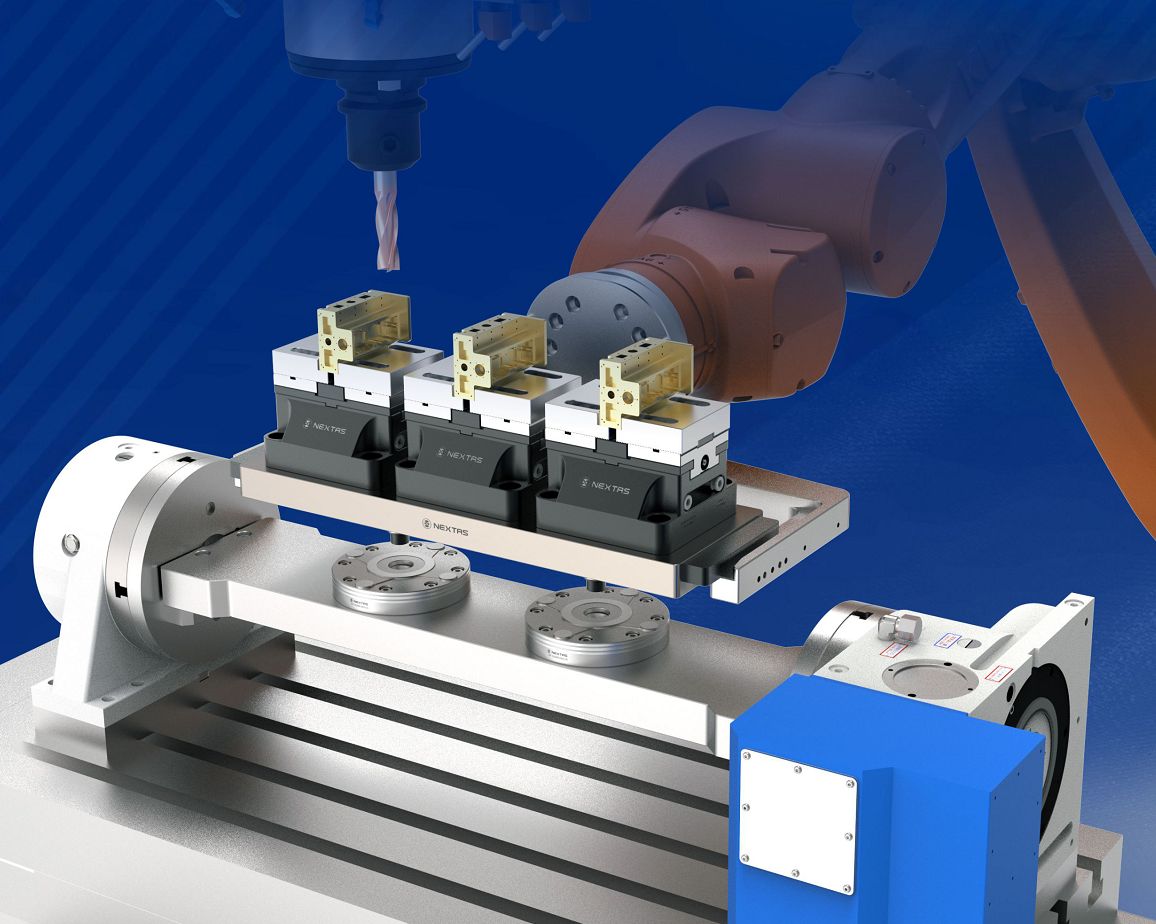
12 core products
Choose a clamping interface, match the workpiece, then plan pallet transfer and automation.
Prepare the next fixture off the machine. Swap complete setups on a shared receiver-module interface.
Explore zero-point systems
Give your tools room to work. Hold suitable parts on the vise centerline with access around the jaws.
Compare vise sizes
Keep the base mounted. Swap the fixture above it with manual locking and less rebuilding between jobs.
See plate layouts
Put fixture release into your automation sequence with an air-released plate selected for your setup.
Review automation options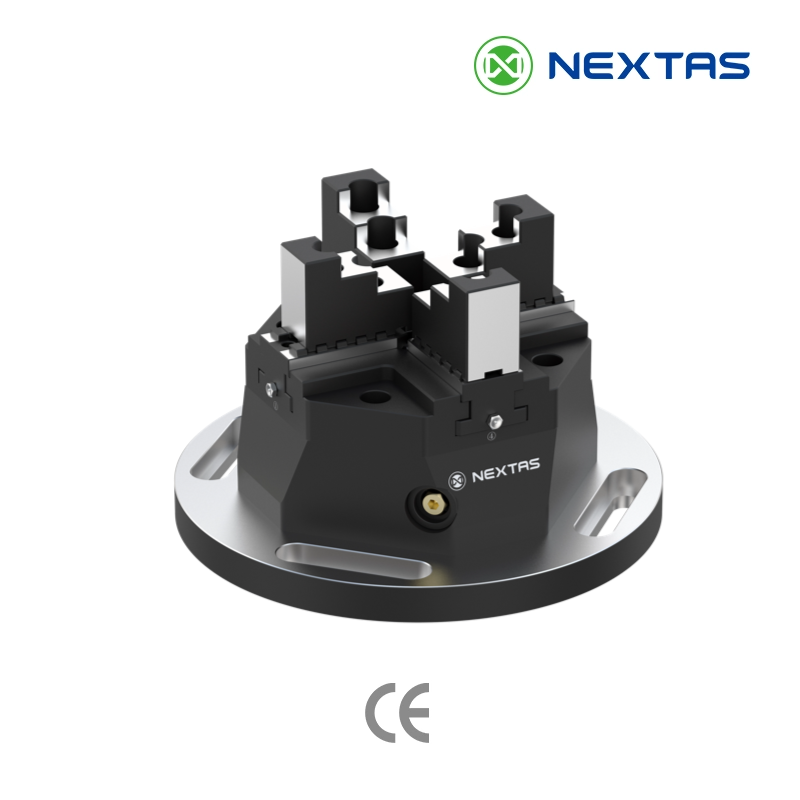
Bring four floating contact points onto irregular blanks with one lead screw.
See chuck capability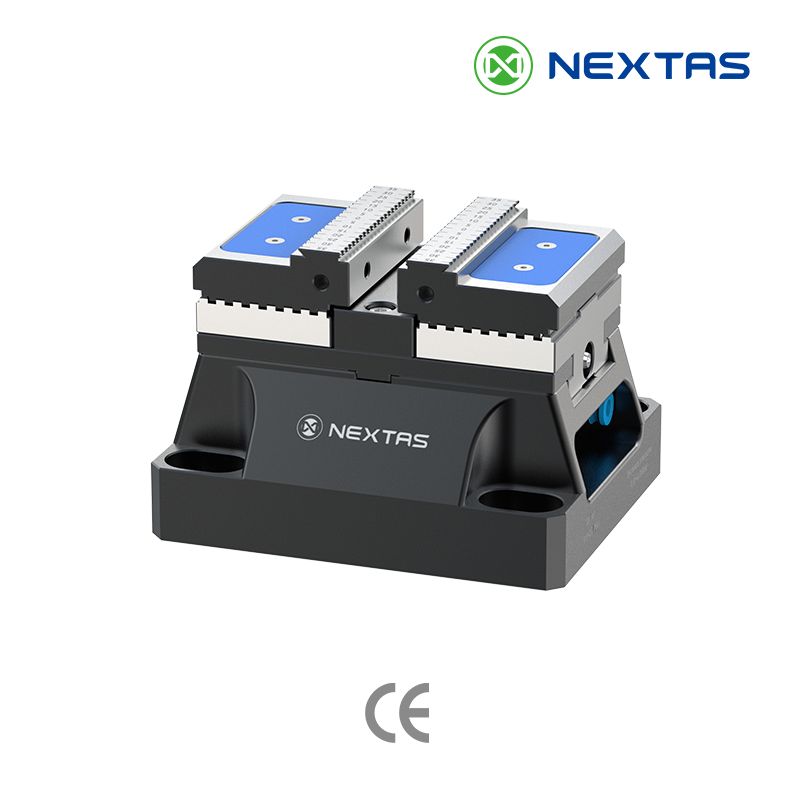
Compare pneumatic V1 and hydraulic V2 clamping. Match the model, supply pressure and jaws to your part and loading cycle.
Check clamp force
Carry electrodes and workpieces between EDM, milling and inspection on a shared datum.
Explore E-Series
Carry a stable reference through CNC, EDM and inspection. Match the chuck, holder and mounting interface to your process.
Explore R-Series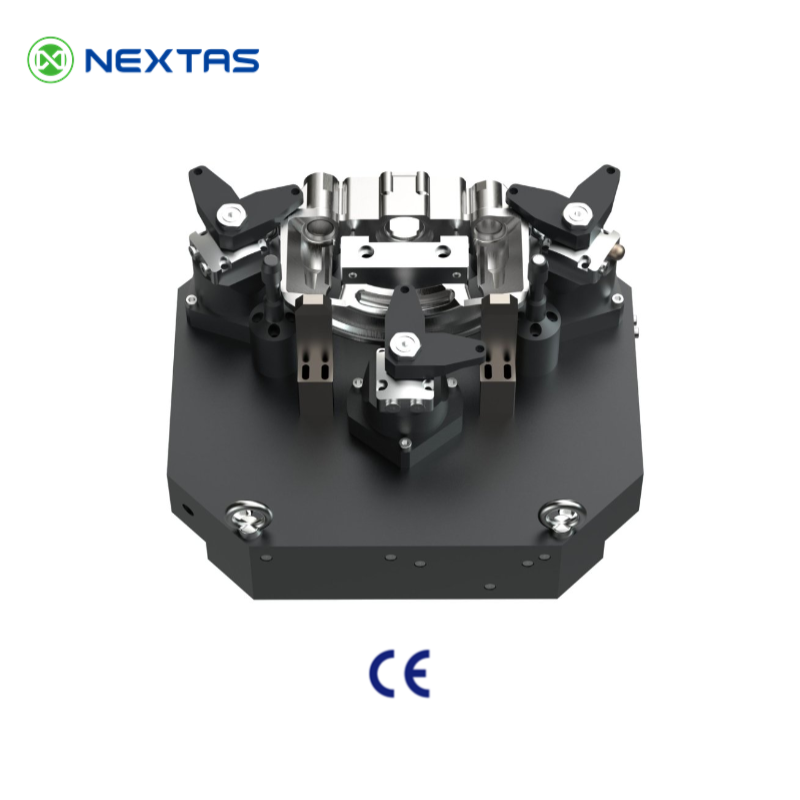
Build the fixture around your part. Develop the locating, support and clamping layout for repeated production.
Discuss a custom fixture
Prepare the next job while the current one runs. Compare manual and automatic transfer for your machine and load.
Compare specs & request quote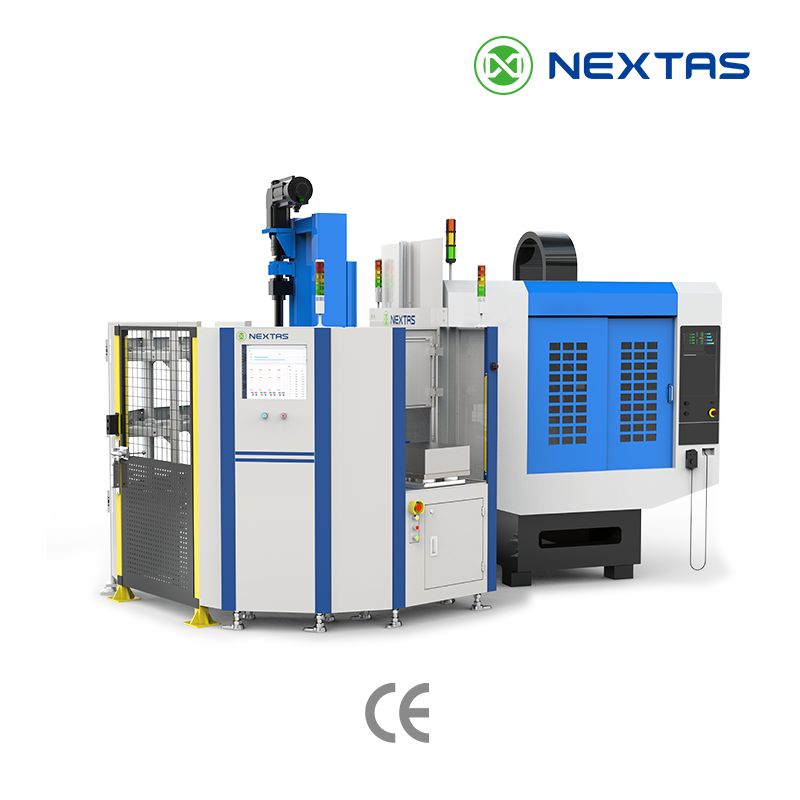
Keep the next pallet ready. Connect storage, robotic transfer and clamp-state feedback around your production flow.
See automation layouts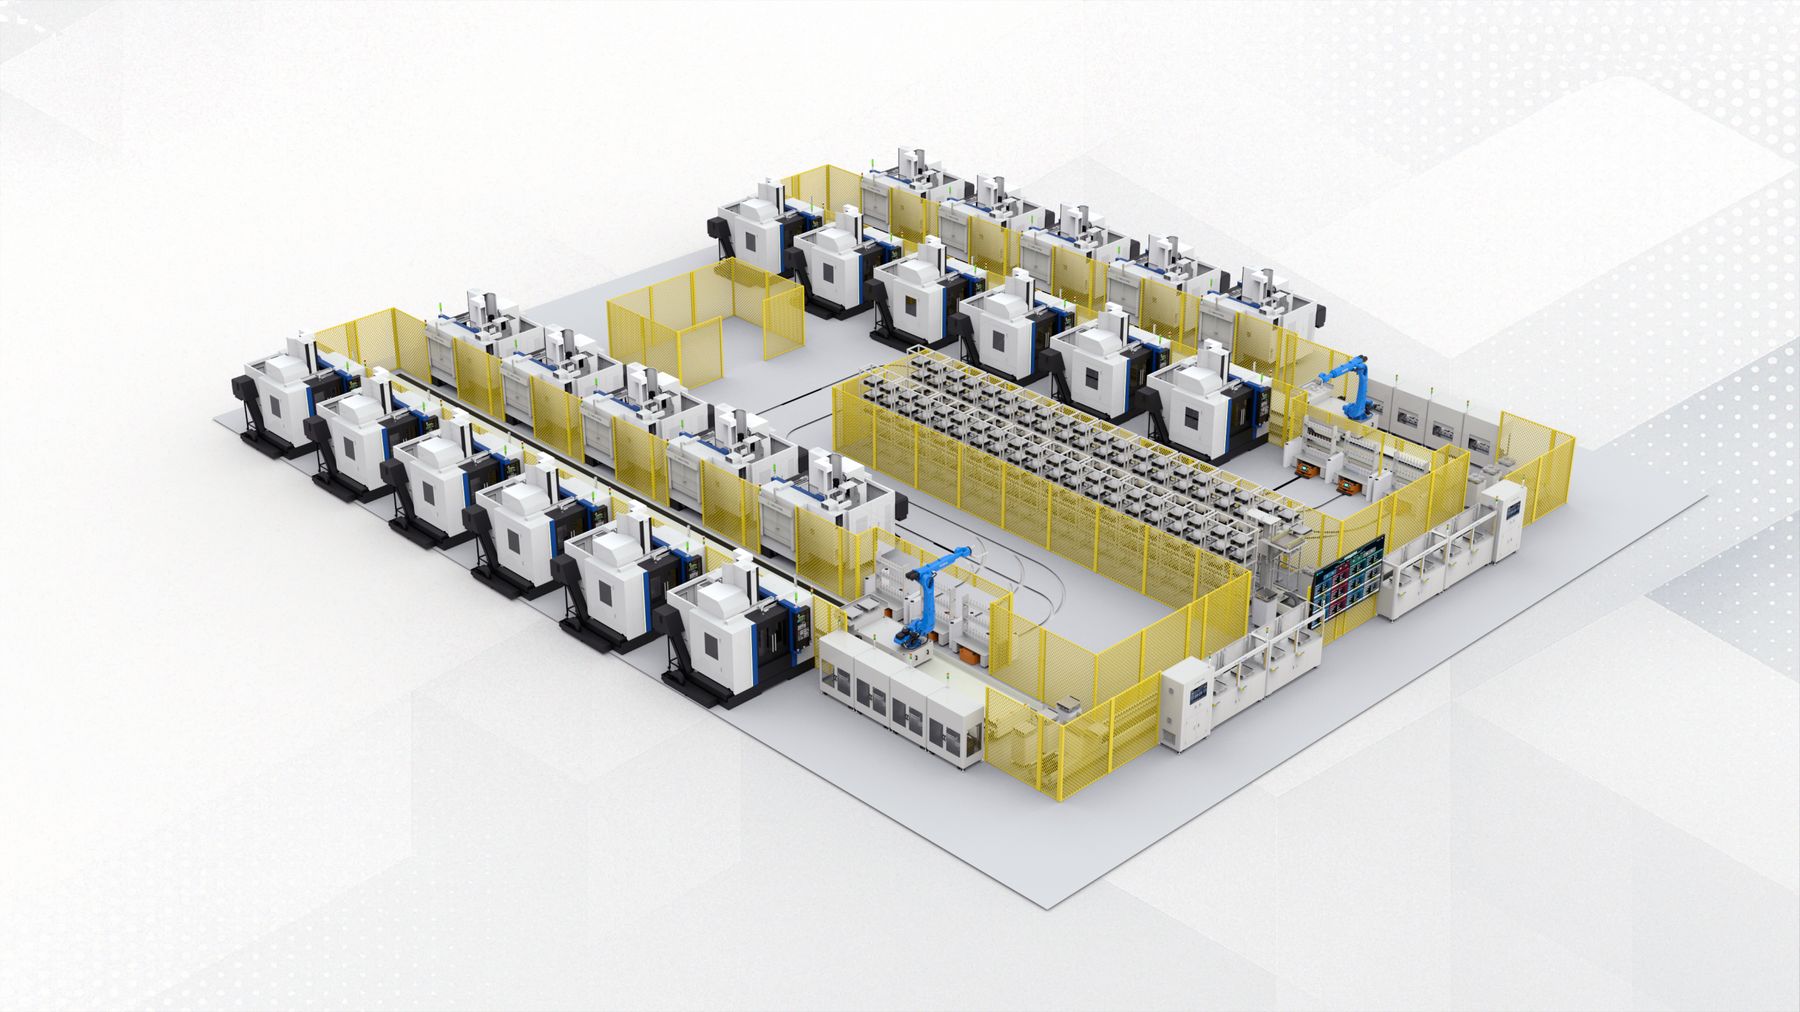
Coordinate scheduling, production status and traceability across your CNC cell.
Explore FMSPublished shop cases
Two published shop cases. See the NEXTAS setups behind each result.
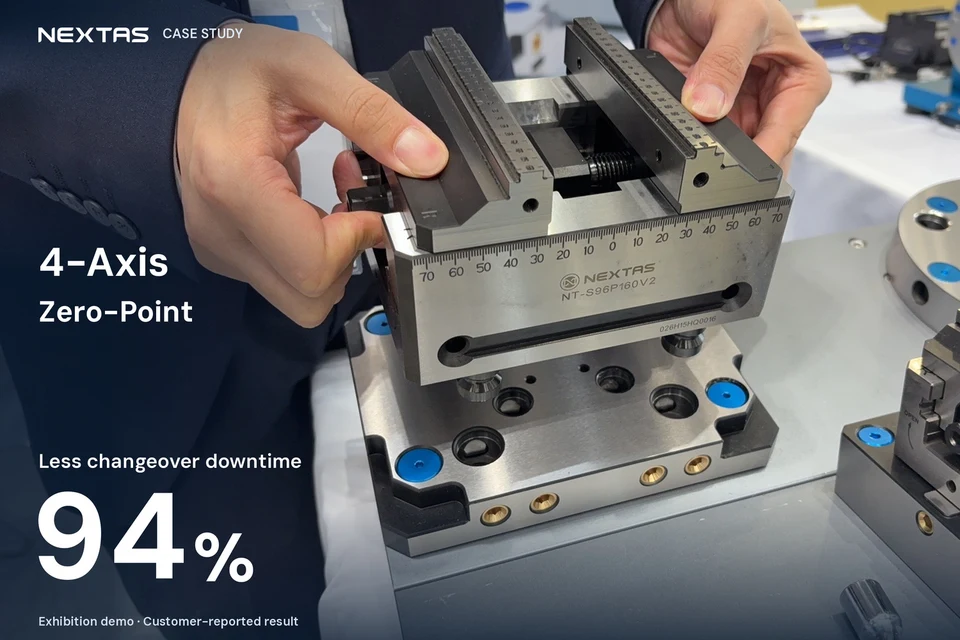
94% less changeover time
96 mm zero-point bridge with NT-S96P160V2 vises.
See the setup behind the result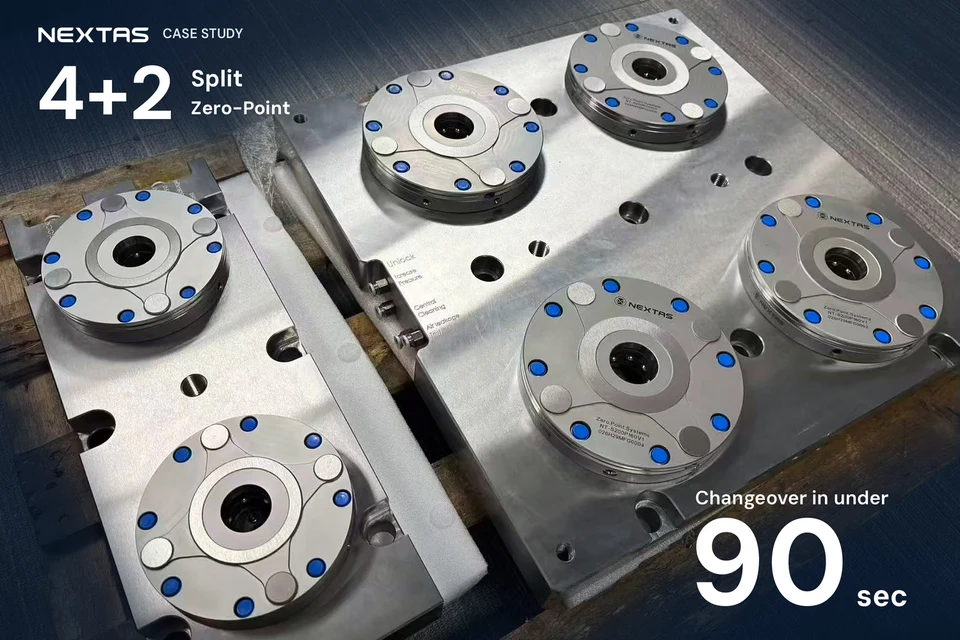
Under 90 seconds
Split pneumatic zero-point zones for flexible fixture changes.
See the setup behind the resultFixture selection
Start with your machine model and a photo of the setup. Tell us where time is being lost; we can work from there and request drawings as the layout takes shape.
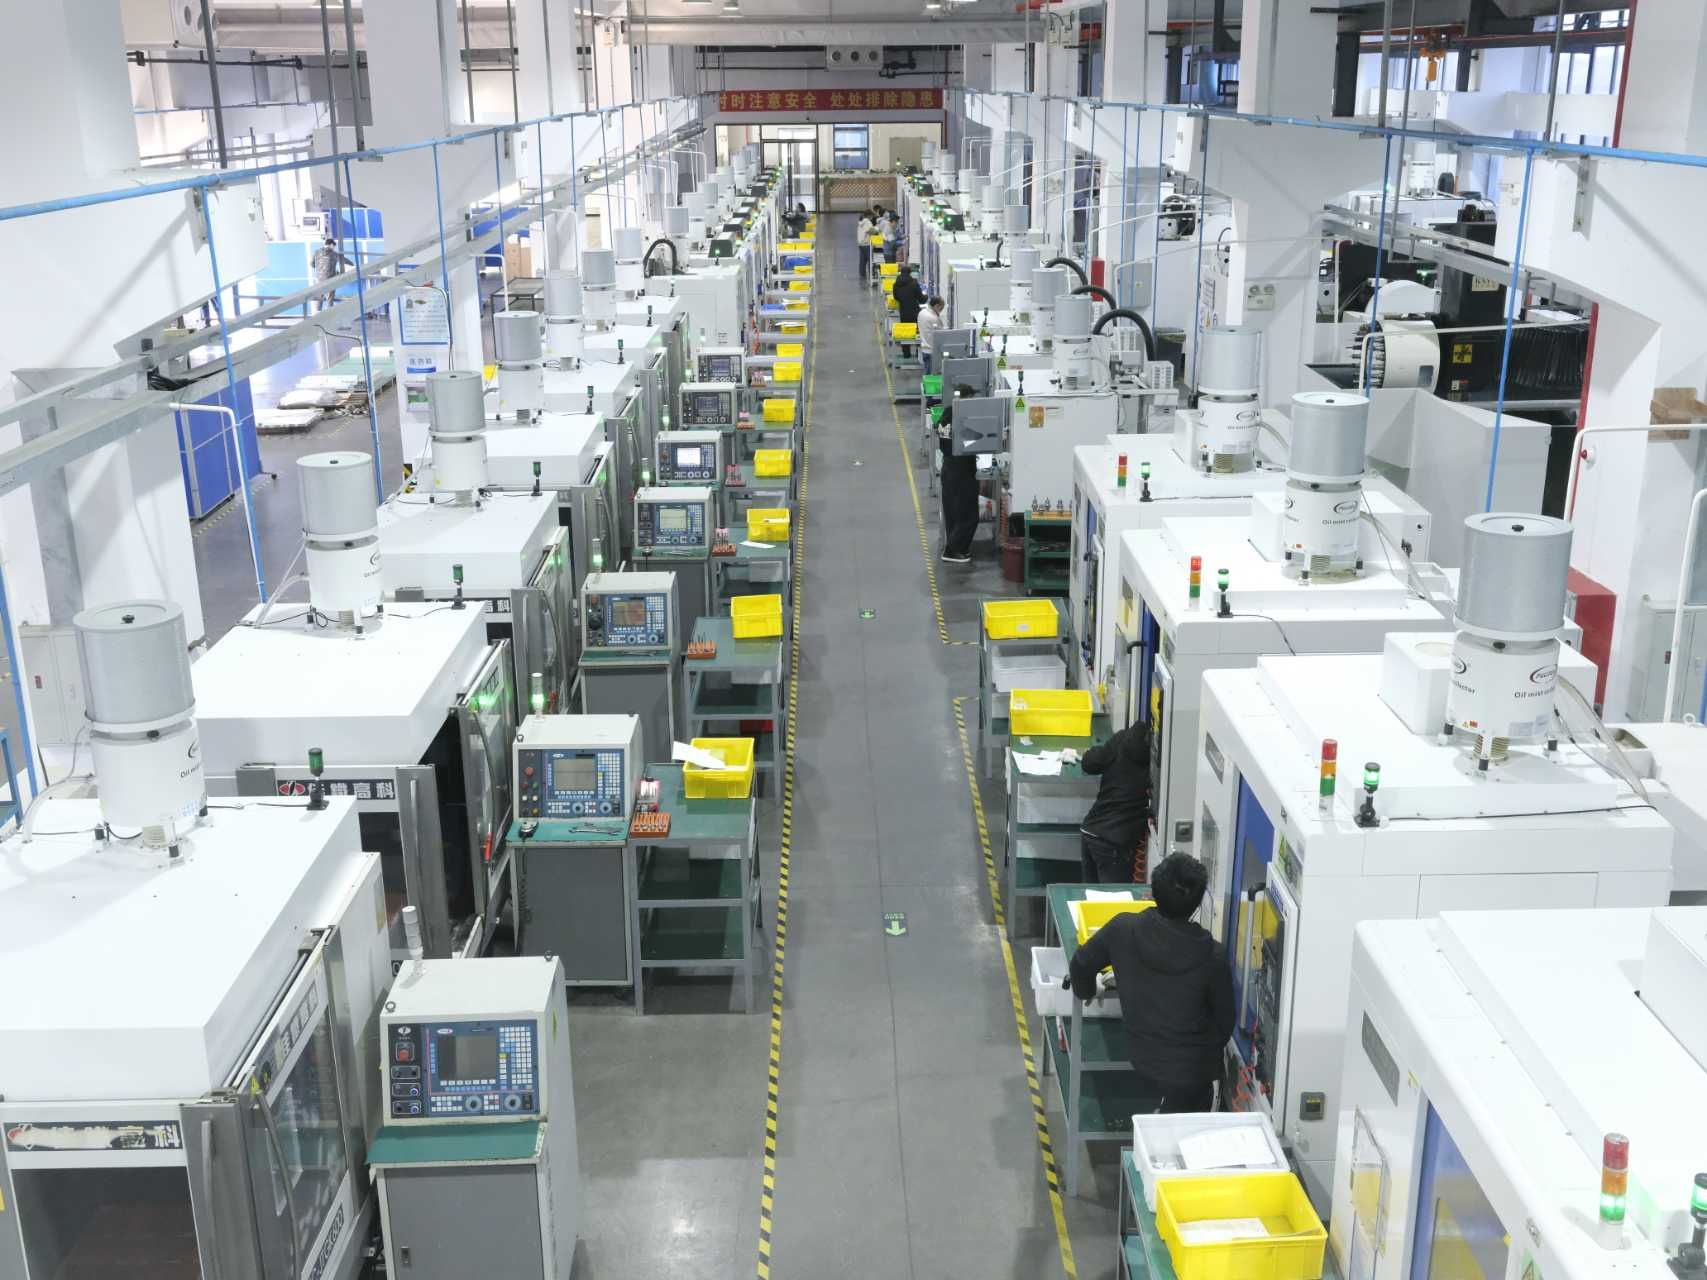
MIC-ASI2411114 · · Zhuhai site
45-second company overview
See the people, production environment and core workholding products at NEXTAS in Zhuhai, China.
Explore our factory View supplier assessmentSemiconductor datum transfer
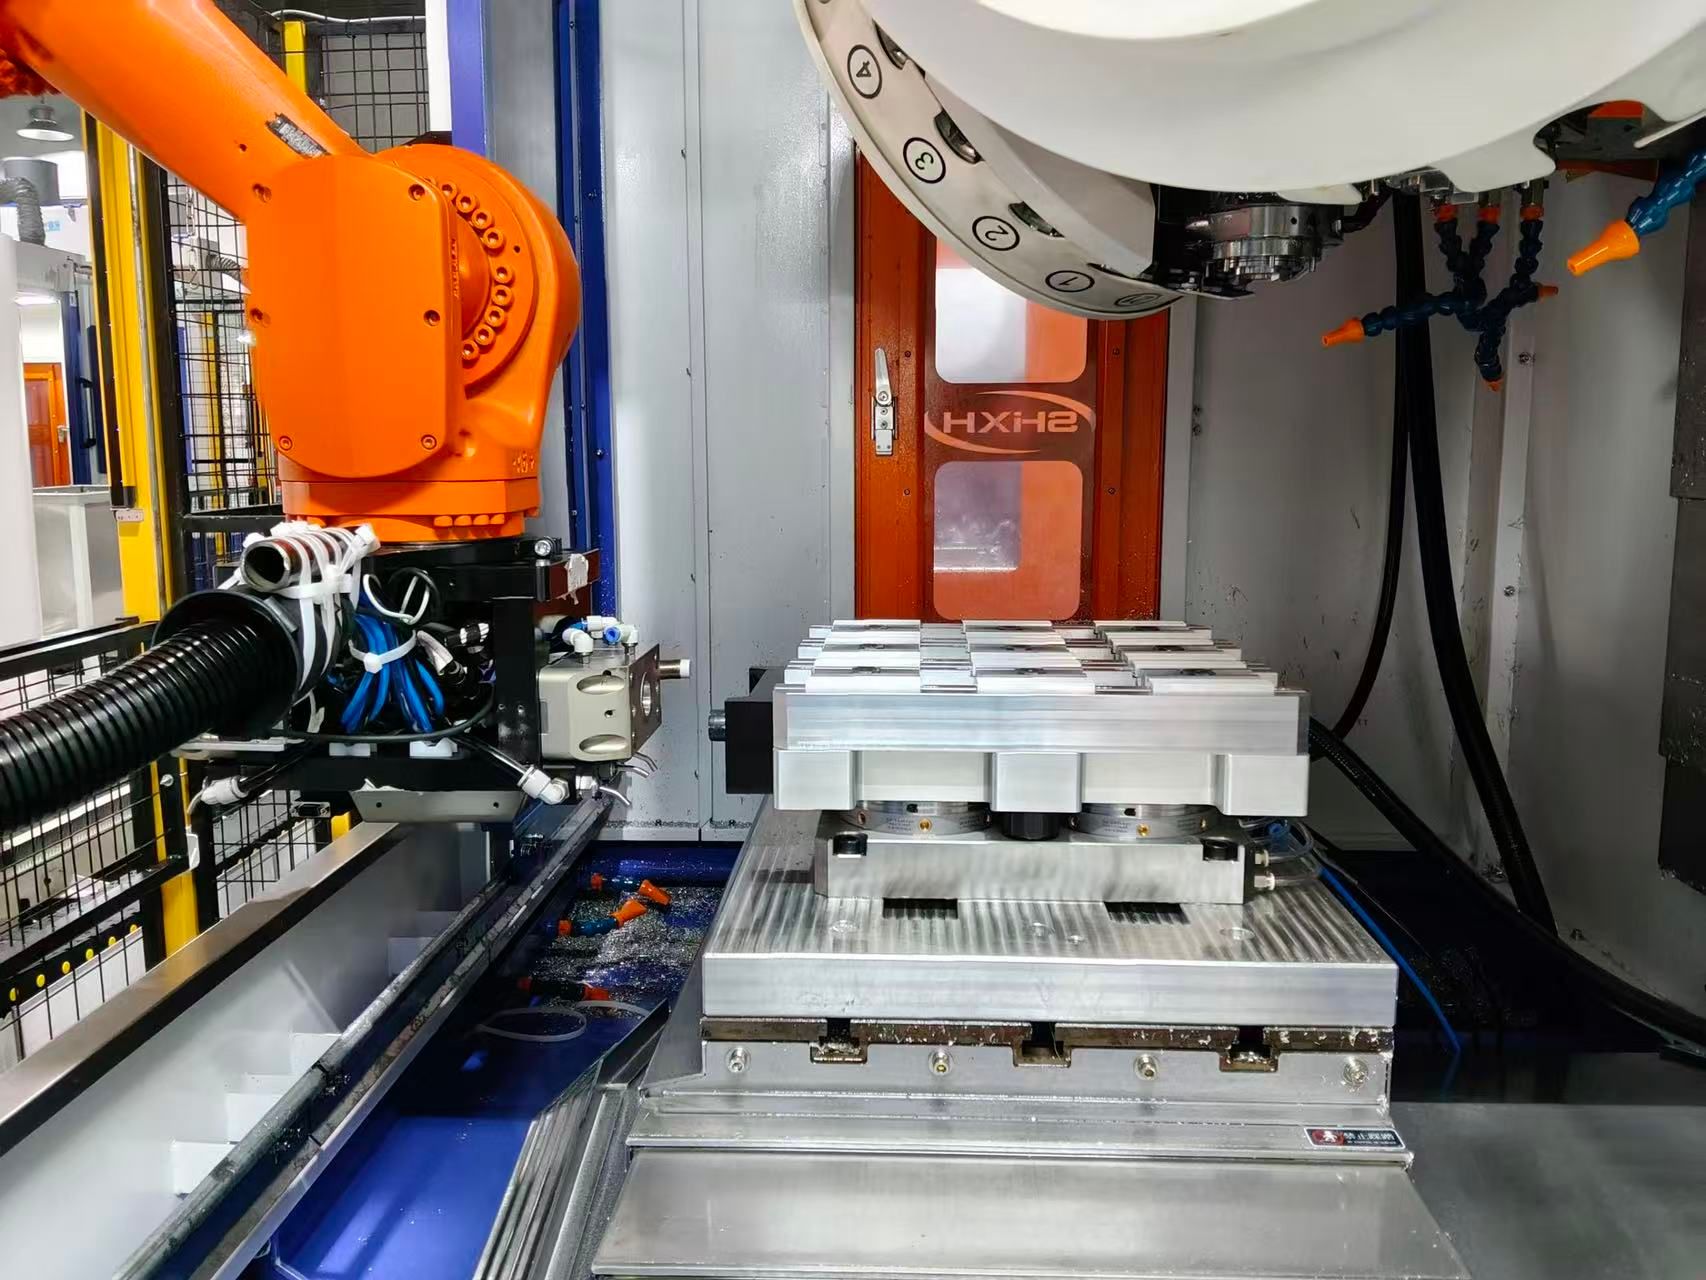
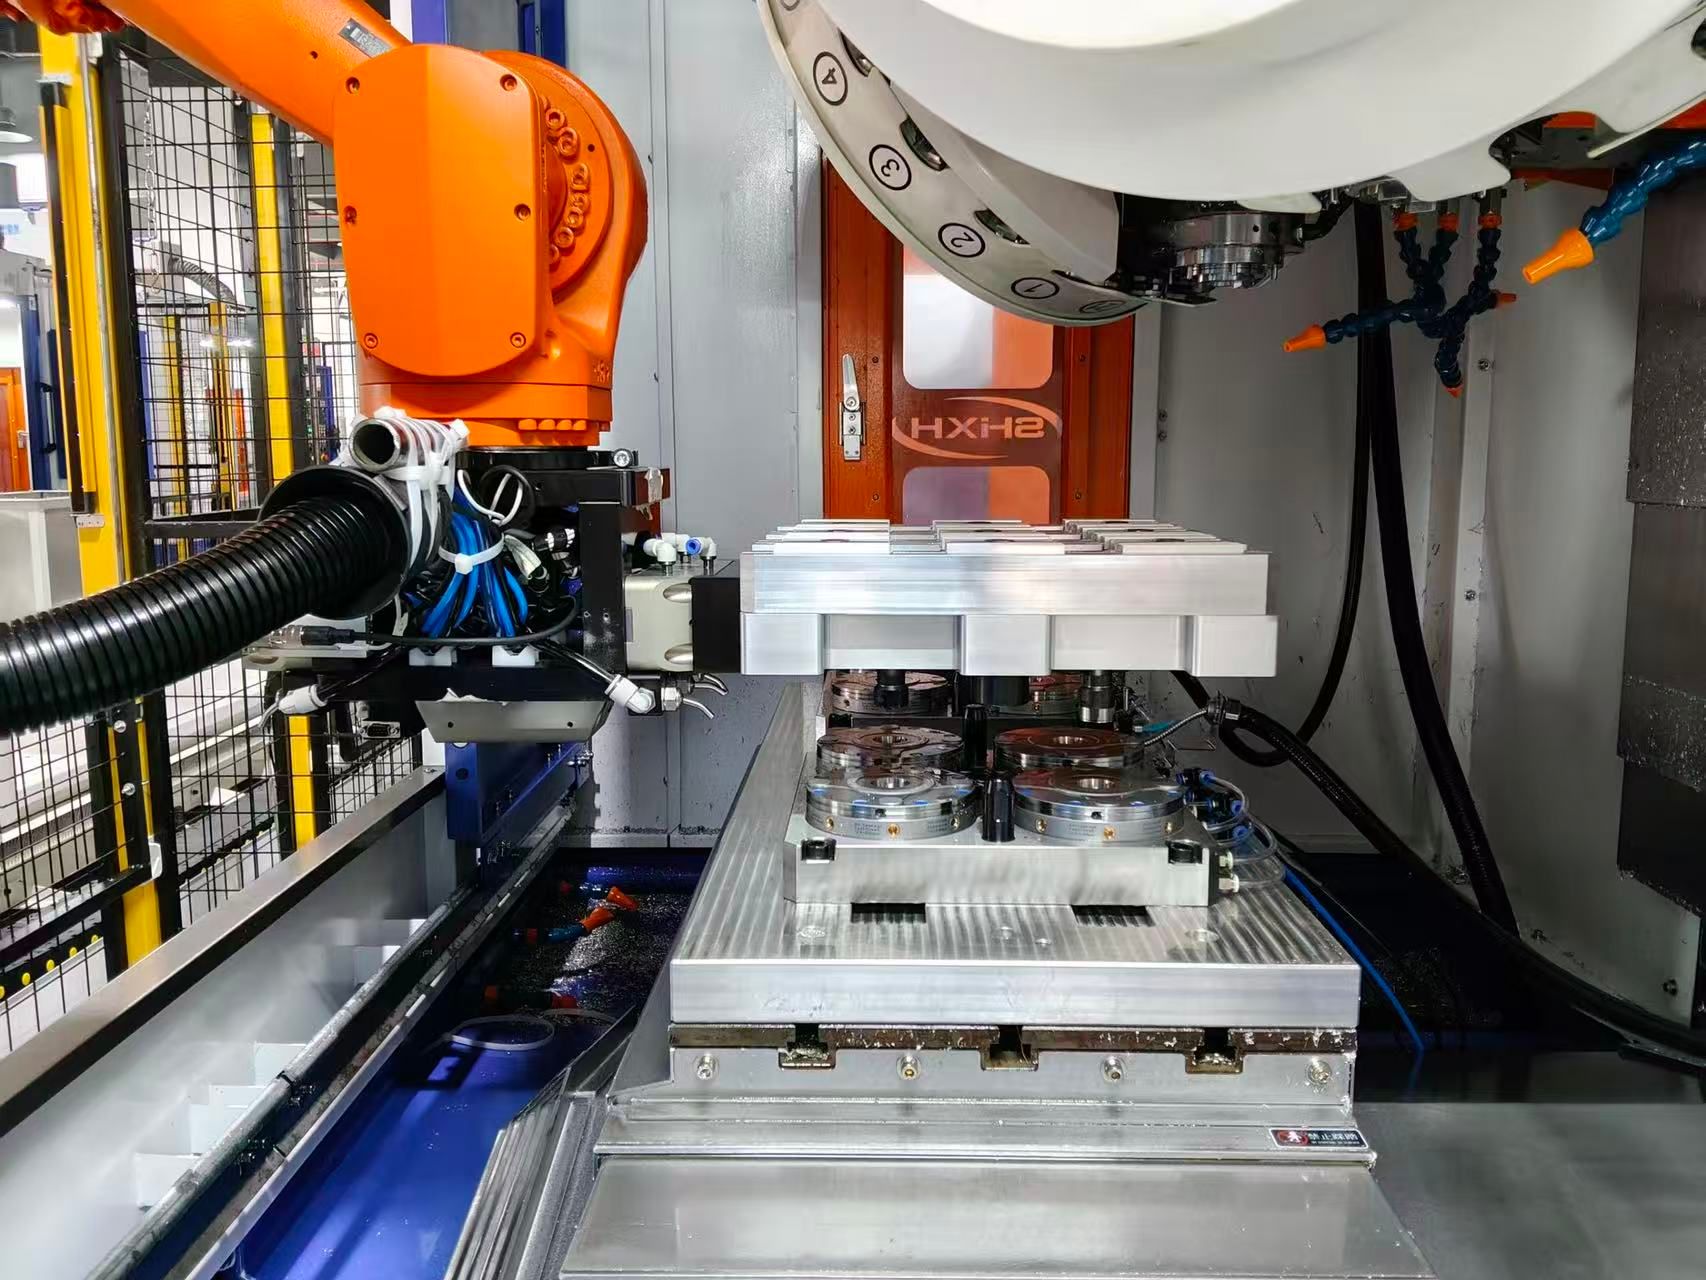
Find out whether the shift comes from receiver reseating, the station handoff, or the upper fixture before changing hardware.
Engineering resources
Workholding architecture guide
Choose the clamp and decide whether it needs a quick-change base.
Read guide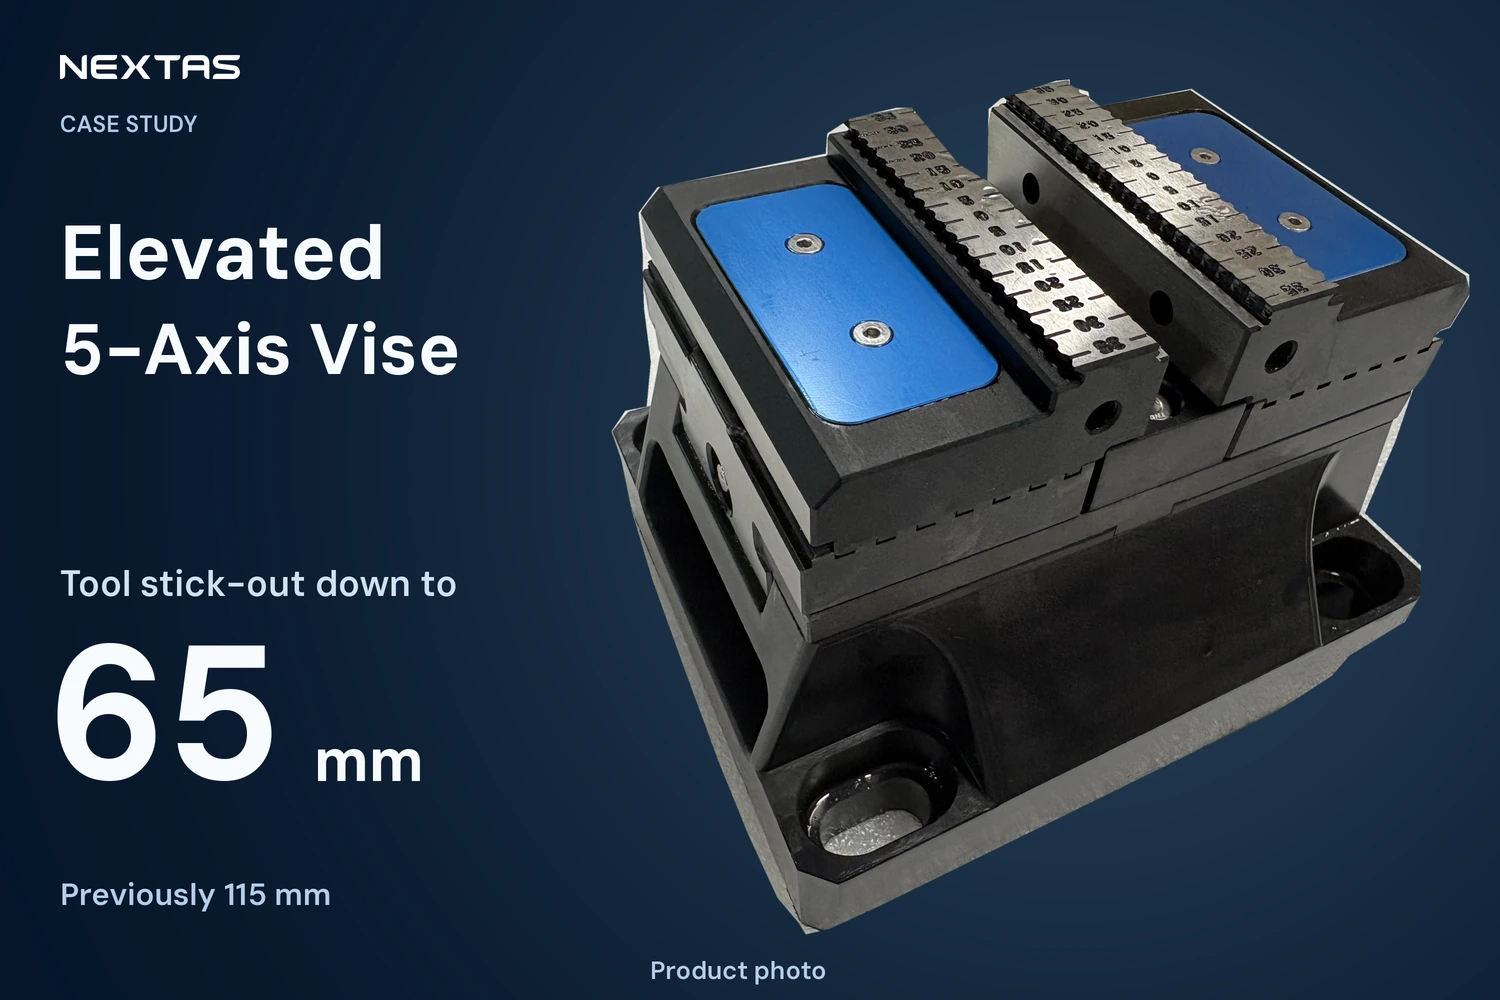
Shop case
An integrated riser shortened tool stick-out and reduced chatter during bracket machining.
Read article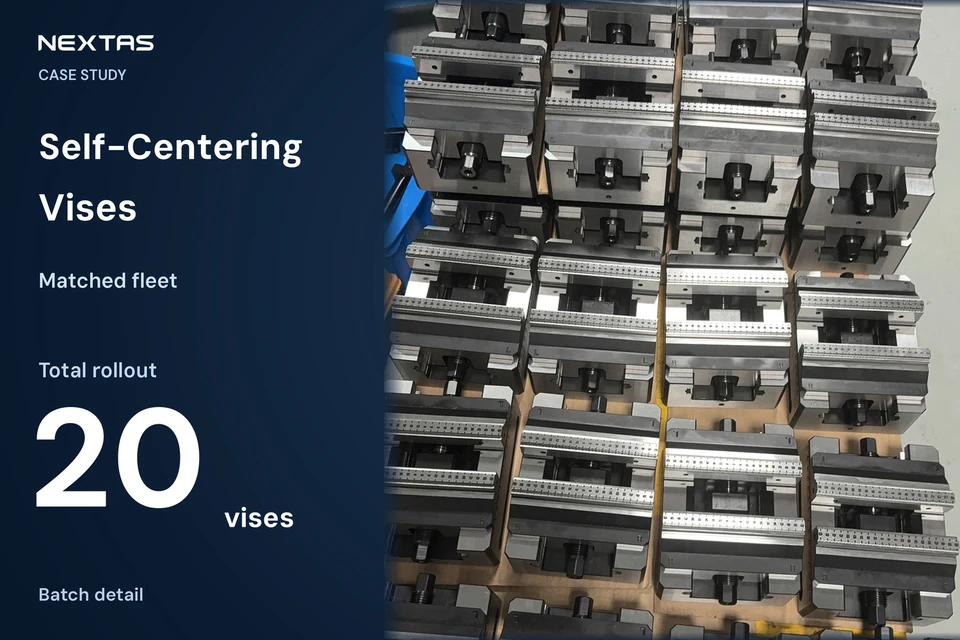
Shop case
Matching jaw heights and centerlines let the shop stage its next 5-axis pallet while the spindle kept cutting.
Read articleWorkholding buyer FAQ
Send your current model numbers, drawings or setup photos. Our engineers will identify which components can be retained, recommend matching hardware and outline any changes, so you can plan the upgrade before ordering.
Share your current tooling model and interface drawing. We will review the mating dimensions, pull studs and working height, then provide selection advice for your setup.
Start with the setup step that costs the most machine time. Share your machine model, part, production volume and any target budget. Our engineers can compare standard and custom options, develop the fixture concept and manufacture the hardware, with the inspection scope defined in your quote. Detailed drawings can follow as the layout develops.
Selected zero-point system series publish repeatability down to <0.003 mm. The applicable inspection method, acceptance criteria, and measurement records are confirmed for the quoted model and project before order.
Material, heat treatment and hardness vary by model and component. Send us the model and component number so our engineers can check the selected drawing and available material, heat-treatment and inspection records with you.
On selected E-Series chuck configurations equipped with air-blast channels, compressed air clears chips and coolant from the seating interfaces during unclamping. Confirm that the selected model includes this function and meets your air-supply requirements.
Dovetail fixtures can provide five-side tool access with a small gripping area. Confirm the selected model-specific dovetail geometry, stock allowance, clamping load and part-distortion limits against your drawing and machining process.
The catalogue lists repeat-clamping accuracy below 0.02 mm for the S52/S96 series. Follow the selected model’s maintenance instructions and recheck the datum after jaw changes or abnormal readings; agree the measurement method and acceptance criteria for your setup.
Yes. This is the dedicated international website for NEXTAS workholding solutions, engineering support and manufacturing capabilities.
Share your machine model, part and setup bottleneck for a quotation review. Complete drawings can follow.
