CNC Workholding
Systems

Explore CNC workholding from NEXTAS in Zhuhai, China. Compare zero-point systems, vises, chucks and custom fixtures, then work with our engineers to match the configuration to your machine, part and production goals.

Product directory

Compare products

Search by product, process or production goal.

Showing all 22 products.

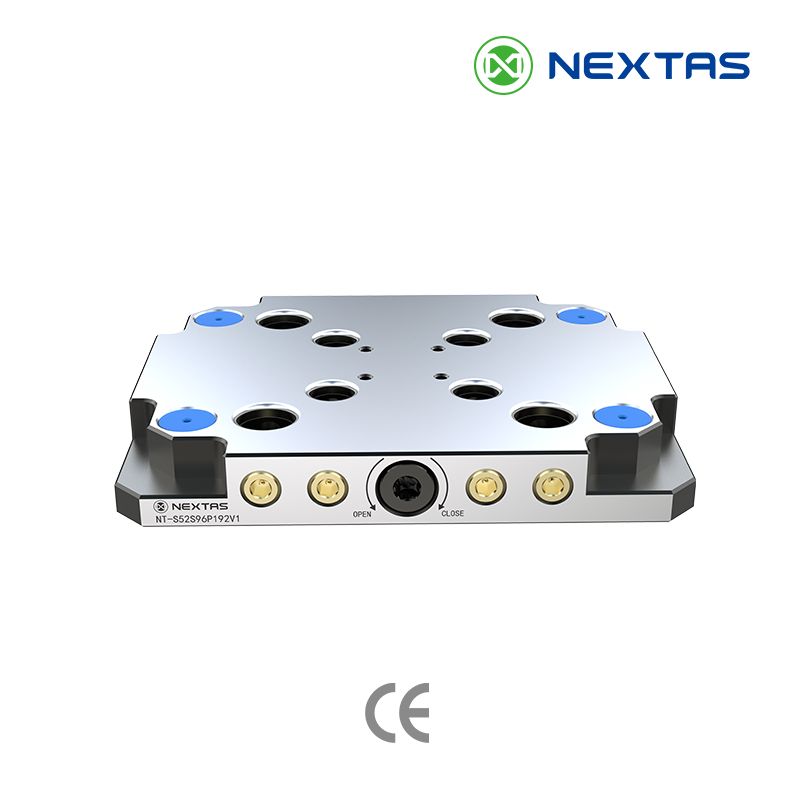
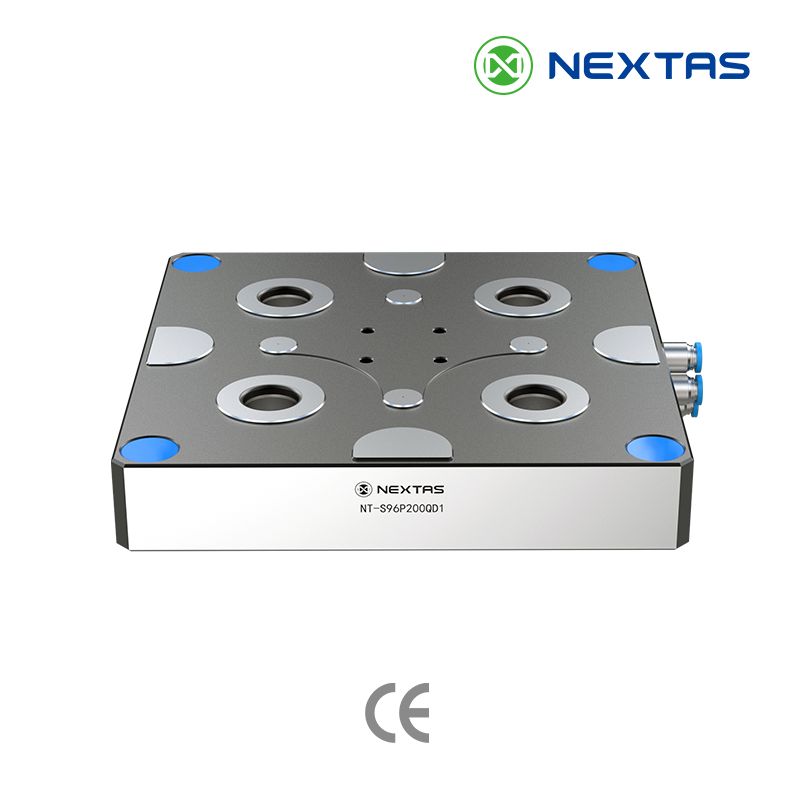
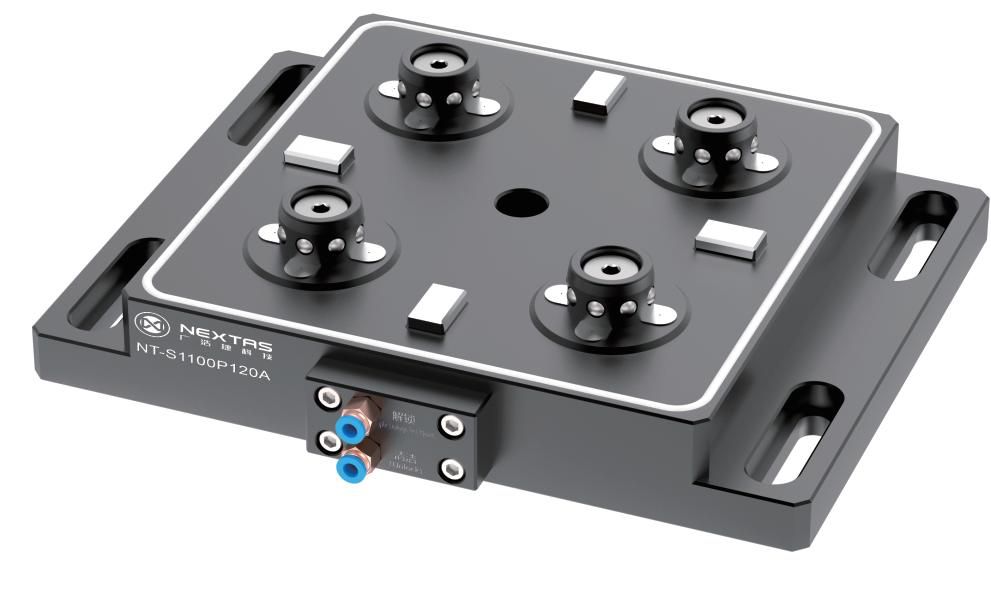
Zero-Point Systems

Vises & Fixtures

Chucks

Automation & FMS

Custom Engineering

Need help choosing a product family?

Quick selection guide

Match the product family to the production goal

Compare the receiver, plate and upper fixture as one stack. Confirm the machine interface, part geometry, tolerance and the operator or robot loading path.

Reduce setup time across several machines

Standardize the datum for fixture and pallet changes. Verify receiver and pull-stud pairing and check the datum at each station.
VMC · HMC · 5-axis

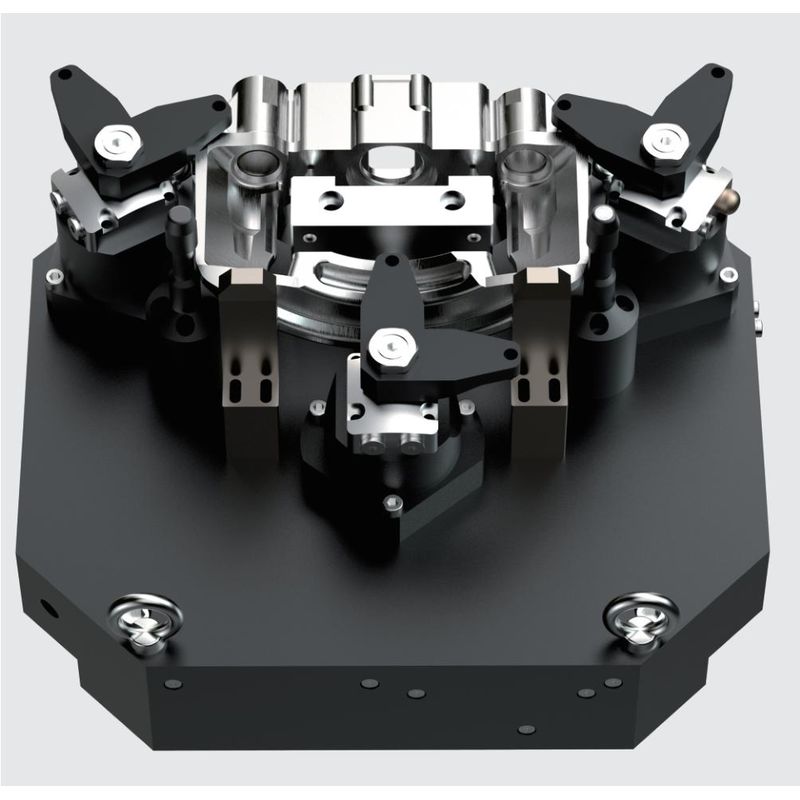
Reach five sides of a complex part

Choose low-profile holding, jaw access, and part support before comparing footprints.

5-axis milling

Prepare a cell for unattended production

Plan the clamp signal, pallet hand-off, storage, and recovery sequence as one system.

Robot · Pallet · FMS

Carry one datum through EDM and inspection

Choose the holder ecosystem and transfer chain before choosing a chuck body.

EDM · CNC · CMM

Stabilize a dedicated production cycle

Engineer the locating, clamping sequence, chip clearance, and acceptance checks around the part.

High-volume production

Published shop cases

Shorter changeovers. More time cutting.

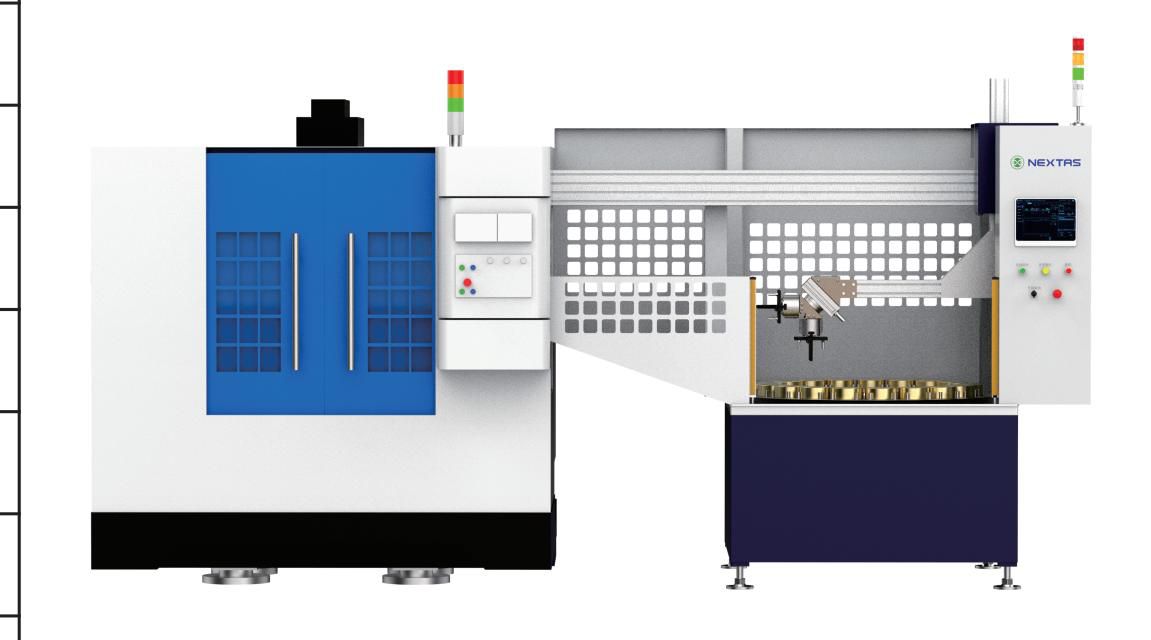
Two published shop cases: a 94% cut in changeover time and a fixture change in under 90 seconds. See the NEXTAS setups behind each result.

One Datum Strategy: How a High-Mix Fluid Power Shop Cut 4-Axis Changeover Time by 94% with NEXTAS Zero-Point Workholding

Before
A 42-minute on-machine changeover left the spindle waiting between short batches.
NEXTAS configuration
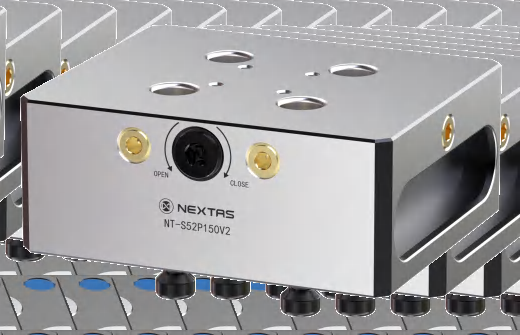
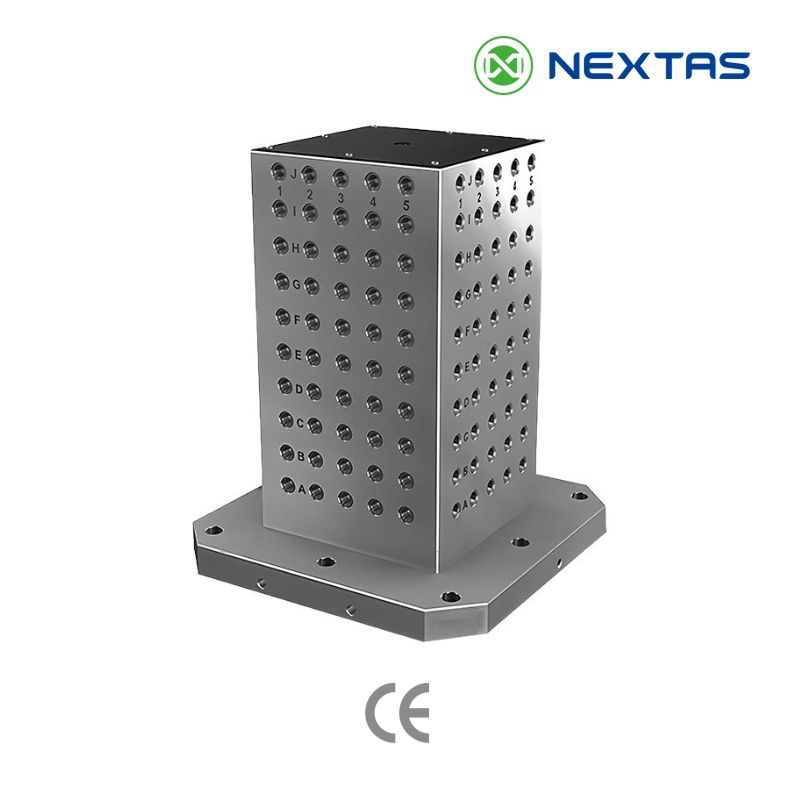
NT-S96P160V2 vises on a shared 96 mm zero-point 4-axis bridge, with the next job prepared off the machine while the spindle cuts.

Reported changeover resulta 94% cut in spindle downtime

See the setup behind the result

Why split one plate into two? A VMC 4+2 pneumatic baseplate

Before
Removing T-slot clamps, indicating the fixture and picking up the origin took 35–50 minutes per batch.
NEXTAS configuration
A four-station pneumatic zero-point zone for the first operation and an independent two-station zone for the second, with the next fixture staged off the machine.

Reported changeover resultFixture changeover under 90 seconds

See the setup behind the result

Engineering before quotation

Tell us about the machine and the bottleneck.

Share your machine and part to get a workholding direction that connects the datum interface, upper fixture and changeover method. NEXTAS can review the selected scope for quotation.

  1. 01
    Machine and tableModel, mounting pattern, available air, and access limits.
  2. 02
    Part and processDrawing, material, operations, tolerance, and current setup.
  3. 03
    Production targetBatch size, changeover time, cycle goal, or automation plan.
  4. 04
    Engineering replyInitial response within 1 business day; the recommended configuration follows after review.
≤0.003 mmcatalog-listed datum repeatability CMMinspection capability Since 2009precision manufacturing
Initial response within 1 business day

Get an engineering recommendation

Start with your machine, workpiece and the setup you want to improve. We can shortlist a product family from there, then work through the configuration for your quotation. Include drawings or model numbers if you have them.

Company and setup details (optional)

Your information is used only to respond to this inquiry.

Prefer WhatsApp? Start a project chat

Engineering buyer FAQ

Answers before you compare a fixture

Exact repeatability, force, interface, and maintenance requirements still depend on the chosen product and installation.

Ask a technical question
How does the Self-Centering Vise maintain accuracy?

The catalogue lists repeat-clamping accuracy below 0.02 mm for the S52/S96 series. Confirm the selected model, jaw setup, measurement method and acceptance criteria before ordering.

What is the main advantage of a Zero-Point System?

Prepare the next fixture off the machine, then exchange it on a matched zero-point interface. Check receiver and pull-stud compatibility and verify the datum at each station before reusing the work offset.

When should I choose a Pneumatic Vise?

Choose pneumatic clamping for repetitive or automated loading where cycle speed and consistent clamping force matter. Confirm air quality, pressure, clamp confirmation, and the safe state before unattended use.

When does a Dovetail Fixture make sense?

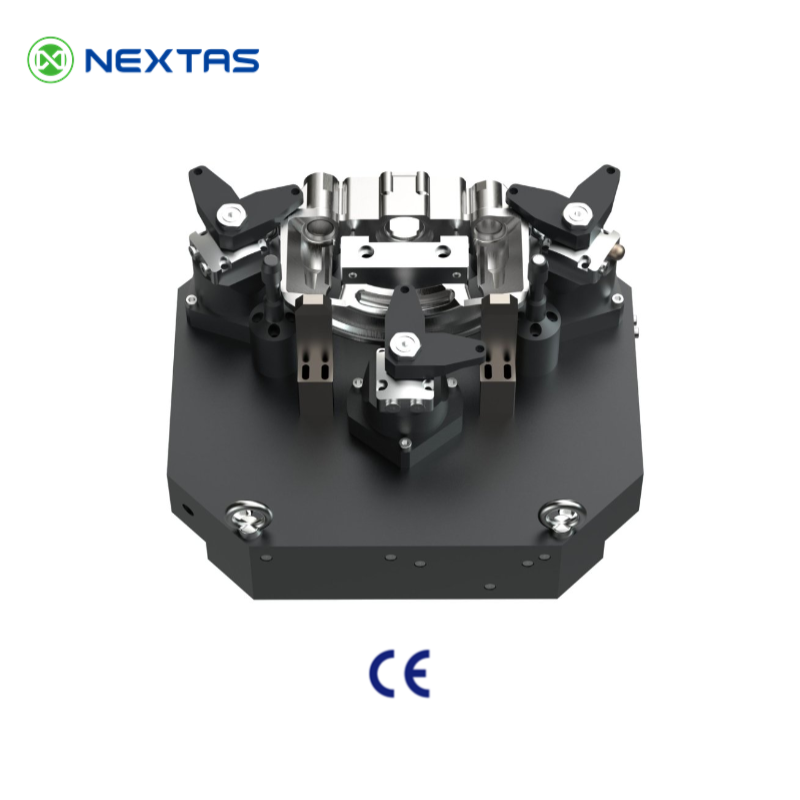
It is a strong starting point for 5-axis parts that need low-profile holding and access around five sides. The raw material needs a small dovetail preparation before clamping.

How are E-Series and R-Series chucks different?

E-Series is centered on ITS-style EDM, WEDM, grinding, and inspection transfer. R-Series is a broader pneumatic and manual datum family for CNC, EDM, presetting, and metrology workflows.

Is this website related to NEXTAS CO., LTD?

This is the dedicated international website for NEXTAS workholding solutions. Product information, engineering support, and manufacturing capabilities are supported by NEXTAS CO., LTD.