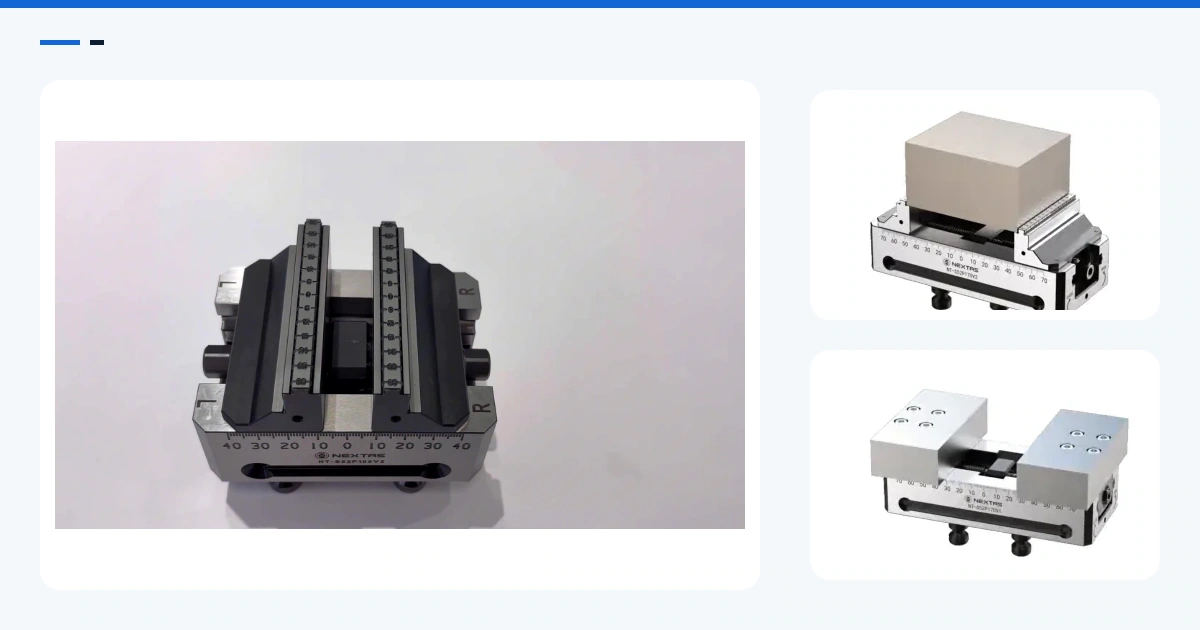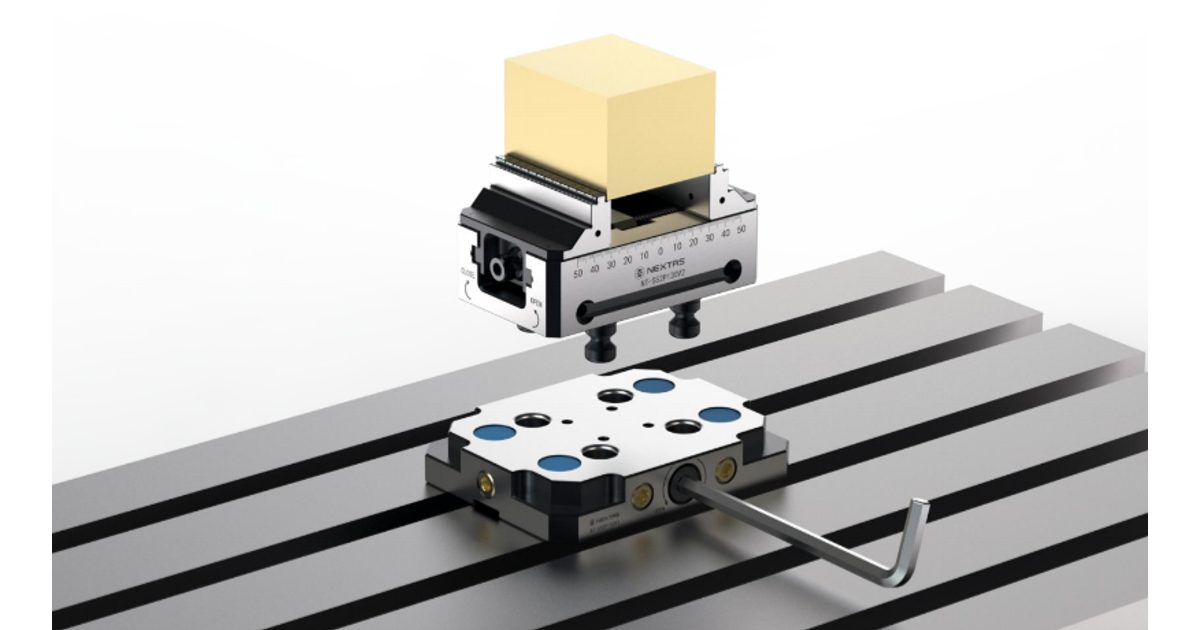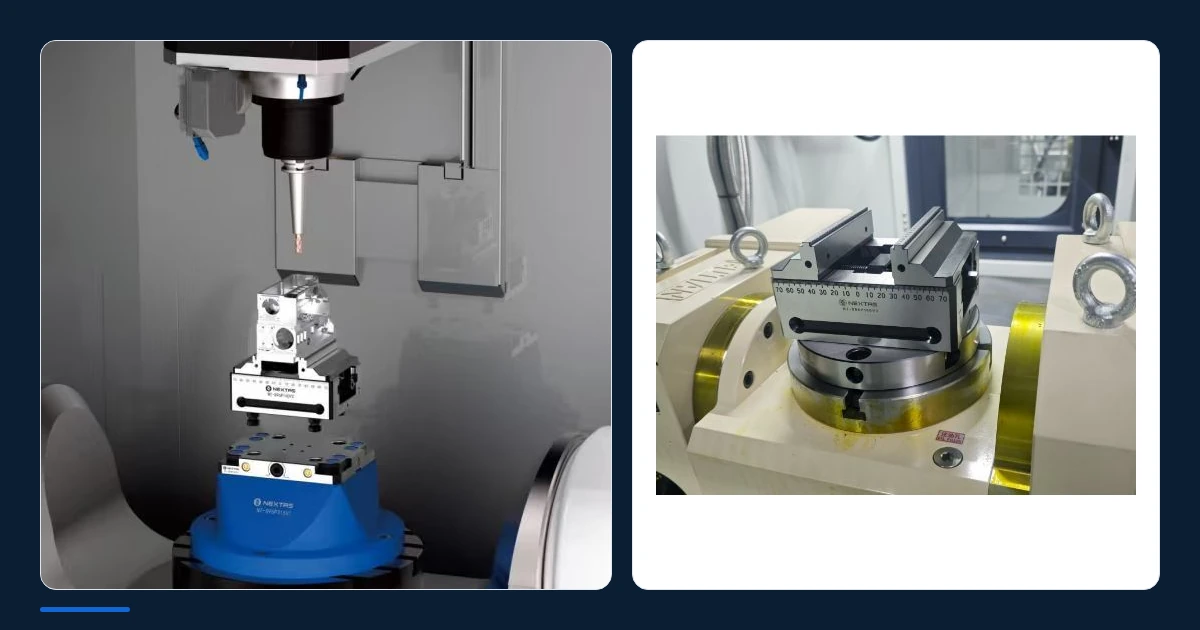
Check jaw contact, fixture height and the complete moving load before the first cut. The self-centering vise product page provides the S52/S96 model specifications.
The short answer: approve the moving setup, not the vise alone
A compact self-centering vise can expose more faces of a complex part. That does not make it an automatic fit for a 5-axis machine. The real object you must approve is the moving assembly: table or trunnion, plate or adapter, vise, jaws, stock, finished part, toolholder and spindle nose.
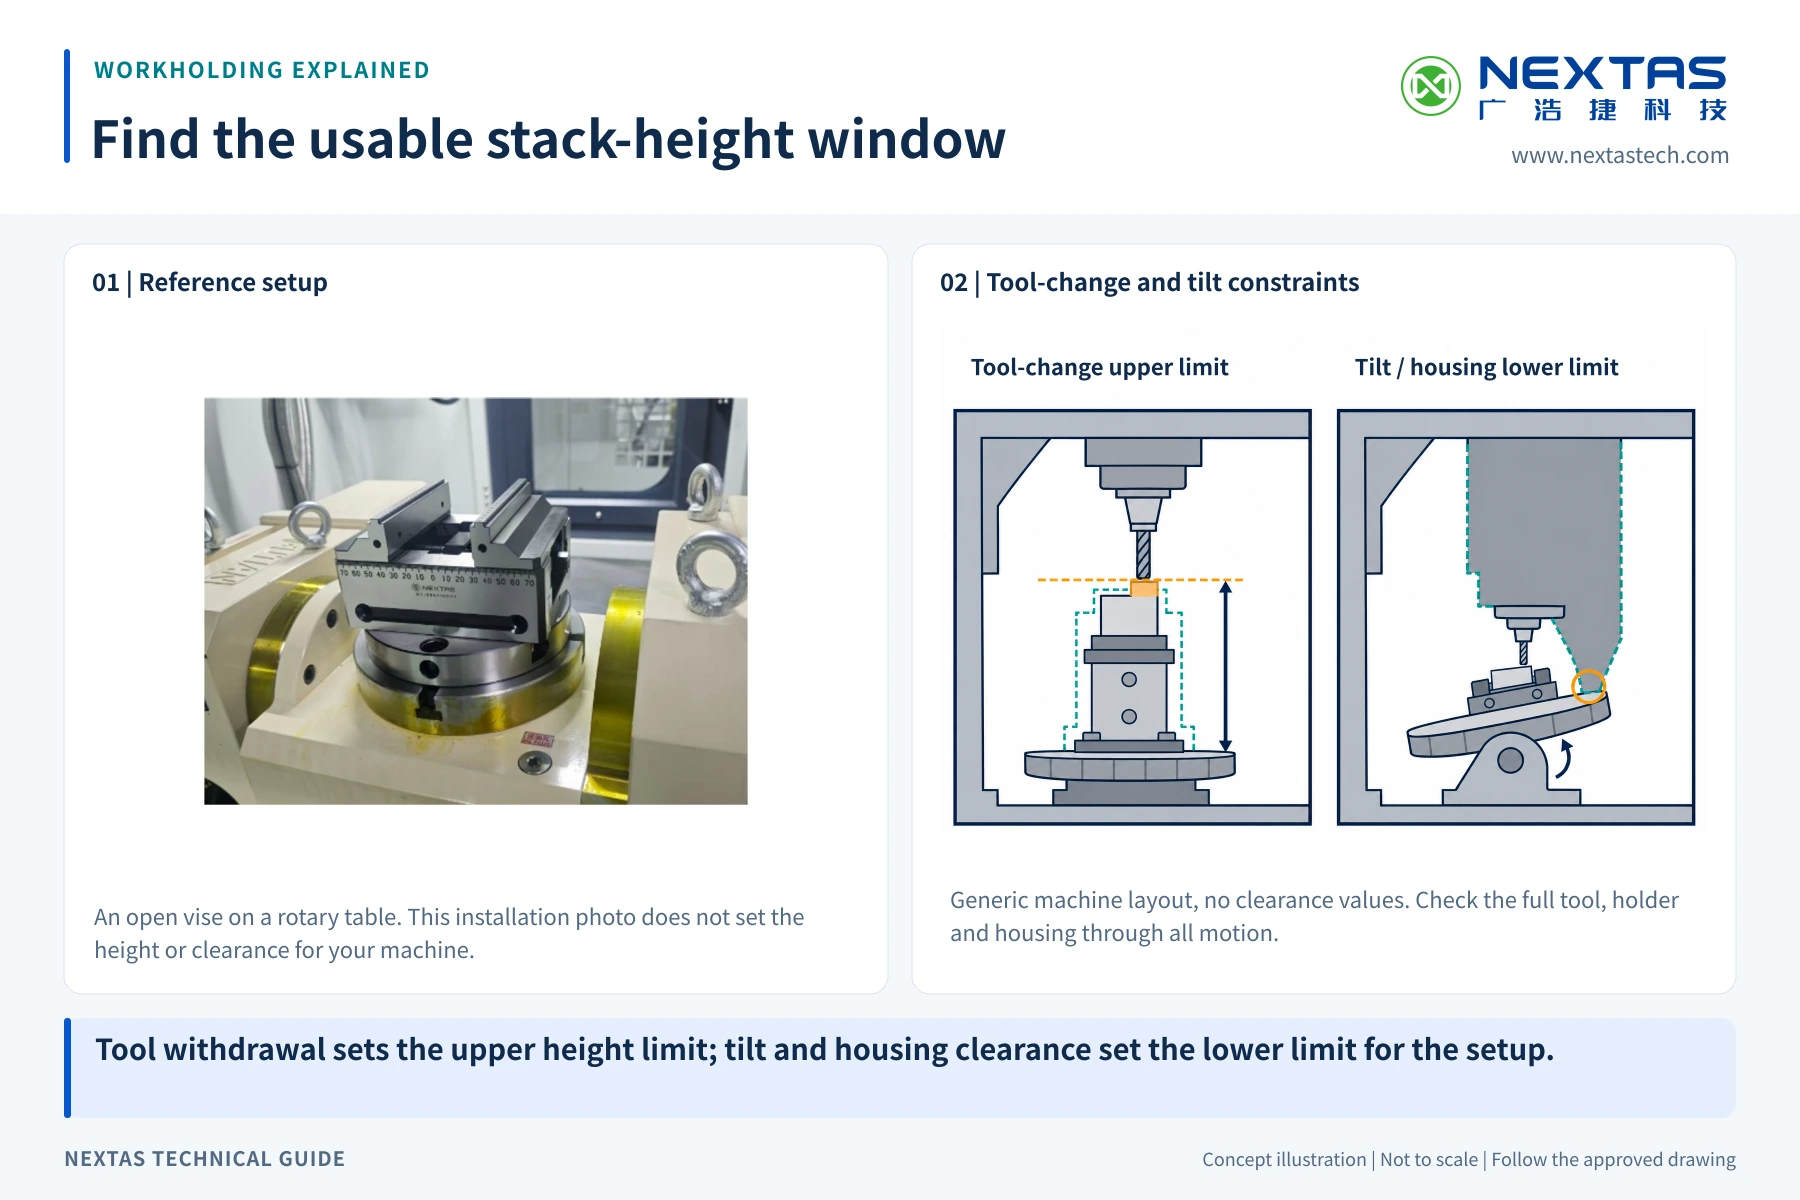
Begin with the largest shape that each item can occupy. Include the jaws when they are fully open. Include stock before it becomes a smaller finished part. Add the longest tool assembly and any probe used in the same program. Then move those shapes through every planned rotary position. A clear front view is not enough.
The vise must also hold the part in a place the tool can reach. That depends on jaw contact, grip depth and support under the cut. Finally, add the full mass and locate the combined center of gravity. Compare both with the machine builder's limits. Only then should you plan a dry run and first article.
A release-ready choice answers five questions:
- Does the stock and finished part stay inside the usable machine space?
- Can every required tool reach the cut without striking the setup?
- Do the jaws contact enough sound material for the planned cut?
- Are mass, turning moment and balance within the machine limits?
- What dry-run, first-article and inspection results will release production?
Build the part envelope from stock to finished shape
The part envelope is the space occupied by the workpiece during the job. Use the raw blank as one boundary and the finished model as another. A casting boss, saw-cut corner or extra stock tab may be the first item to hit the spindle, table or enclosure. Do not check only the final CAD shape.
Mark which faces must be cut and which material must remain for clamping. Add any probe move, tool-change position and hand-loading move. If the workpiece is turned or reloaded, treat each setup as a separate envelope. Also show the part at the rotary limits used by the program, not just at zero degrees.
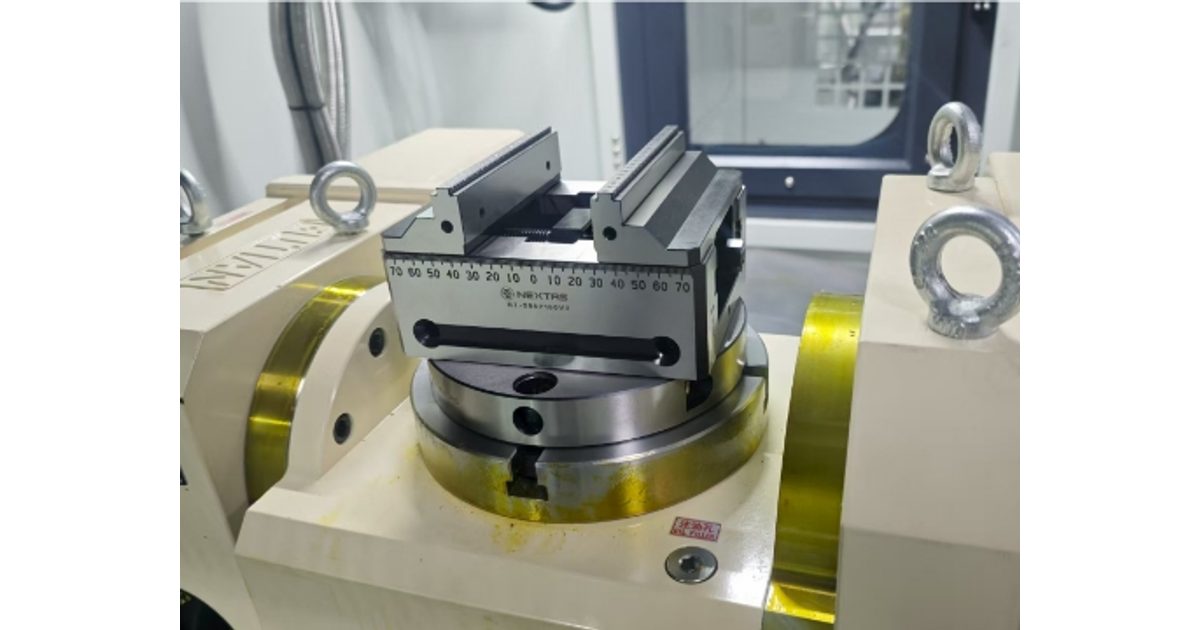
A useful clearance review records the smallest gap at each critical position. The machine owner should set the required margin. The margin must cover real variation in stock, tool length, setup and machine behavior. NEXTAS can review supplied geometry, but the machine builder and process owner remain responsible for the permitted motion.
Trace the toolholder and spindle nose, not only the tool tip
Many 5-axis collisions happen above the cutting edge. A short end mill may clear while its holder or the spindle nose hits the jaw, part or adapter. Put the full tool assembly into the check. Use the actual gauge length, holder diameter and spindle outline. If more than one tool can make the feature, compare both access paths before raising the part on a taller stack.
Check approach, cutting and retract moves. A holder can pass the cut and still collide on entry. A probe can also need more room than the cutting tool. At steep tilt angles, check the rear jaw, screw housing and open jaw travel. At rotary reversals, make sure no cable, air line or manual handle enters the moving zone.
Tool access is a tradeoff. A taller jaw or riser may expose a lower feature, yet it raises the part and moves the cut farther from the table. A shorter jaw may improve clearance but leave less contact. Do not solve one blocked feature by creating an unknown support or load case.
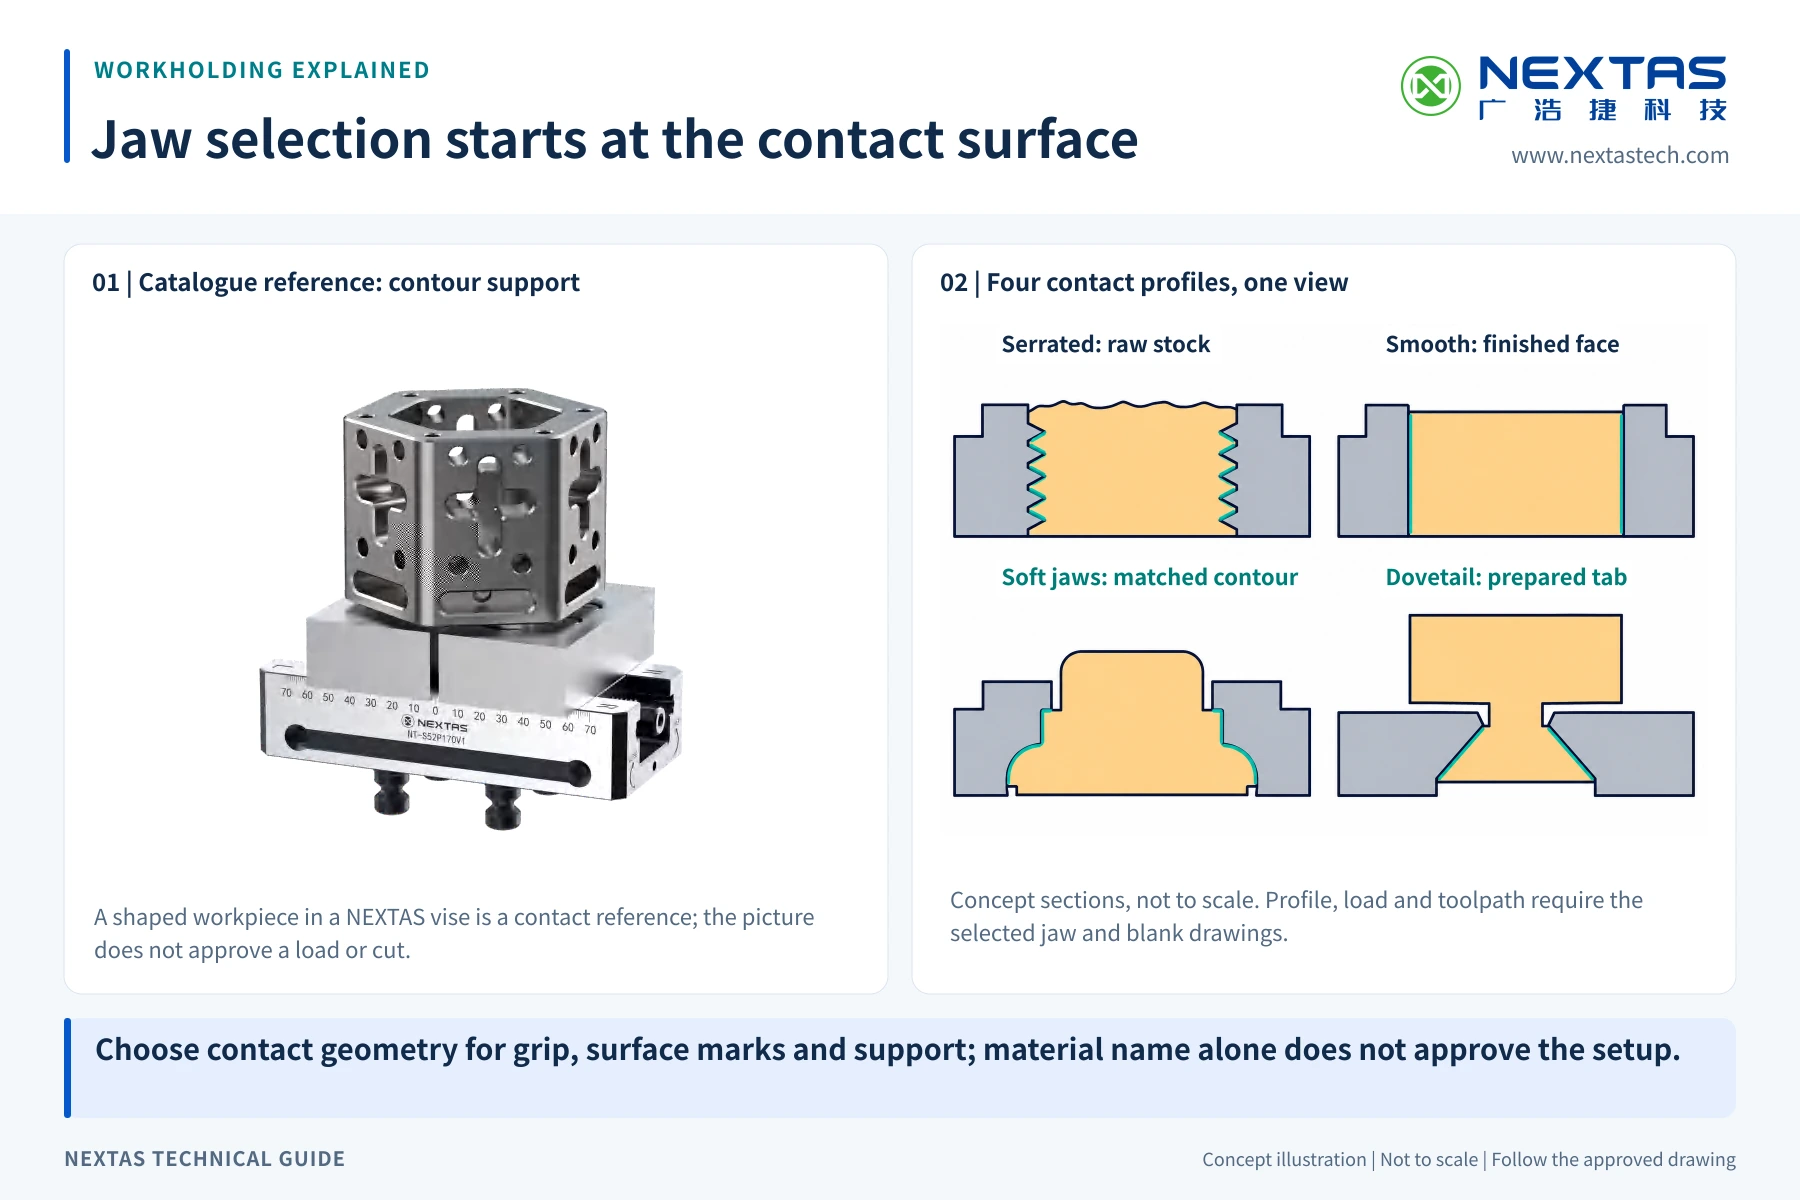
Choose jaw contact and grip depth from the cut
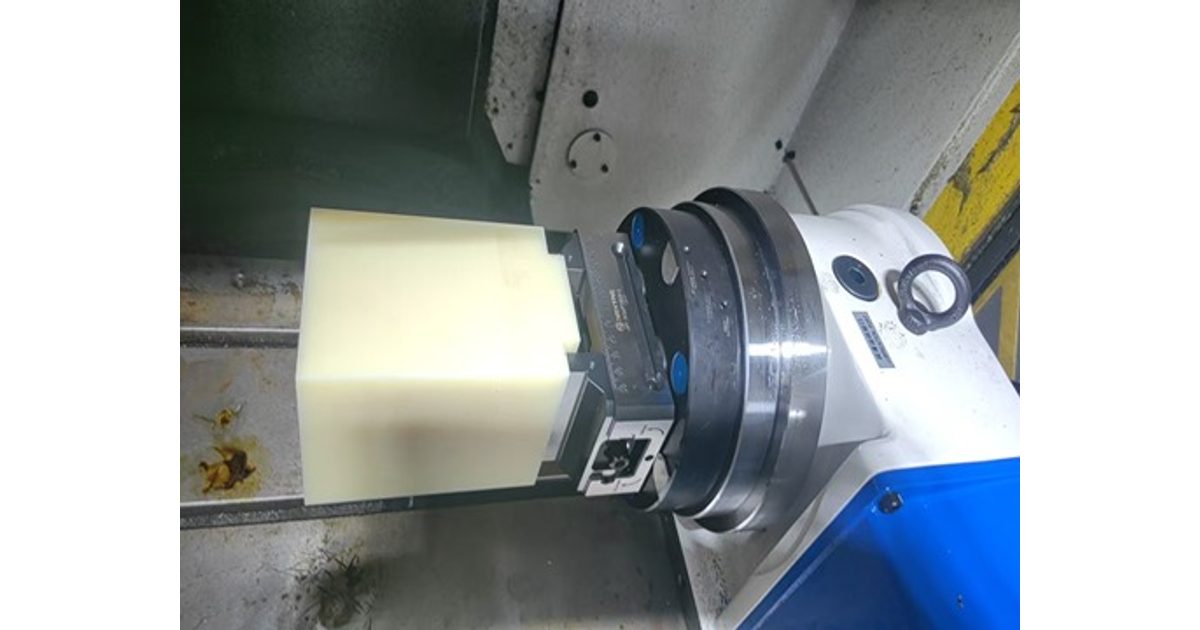
Grip depth is the vertical amount of material held by the jaws. There is no universal depth for a complex part. A safe plan depends on the material, contact shape, cutting direction, tool load, overhang, jaw style, support and allowed clamp load. “Hold as little as possible” is not a release rule.
Start by drawing the jaw contact on the stock. Show the contact height, length and surface condition. Hard jaws may suit repeat raw-stock shapes when their contact is understood. Soft jaws can be machined to support a special profile or protect a finished surface. Serrated contact may help rough stock, but it changes the surface and must be approved for that part. Do not assume that two jaws touching the part means the load path is sound.
Keep the clamp load tied to the chosen model and jaw setup. The self-centering product family contains different sizes and force ratings. It also lists repeat positioning for named hardware. Neither value is a finished-part tolerance or a promise that a shallow grip will survive a planned cut. Part results still depend on the full machine, mounting, jaw, tool, program and inspection chain.
Thin walls need special care. Clamp load can move the part before cutting starts. Cutting can then remove material and release that stress. Use support where the process allows it, choose a contact shape that spreads load, and inspect the part both clamped and released when distortion matters. If contact, material or load is unknown, stop the release and resolve it.
Check total rotary load and the combined center of gravity
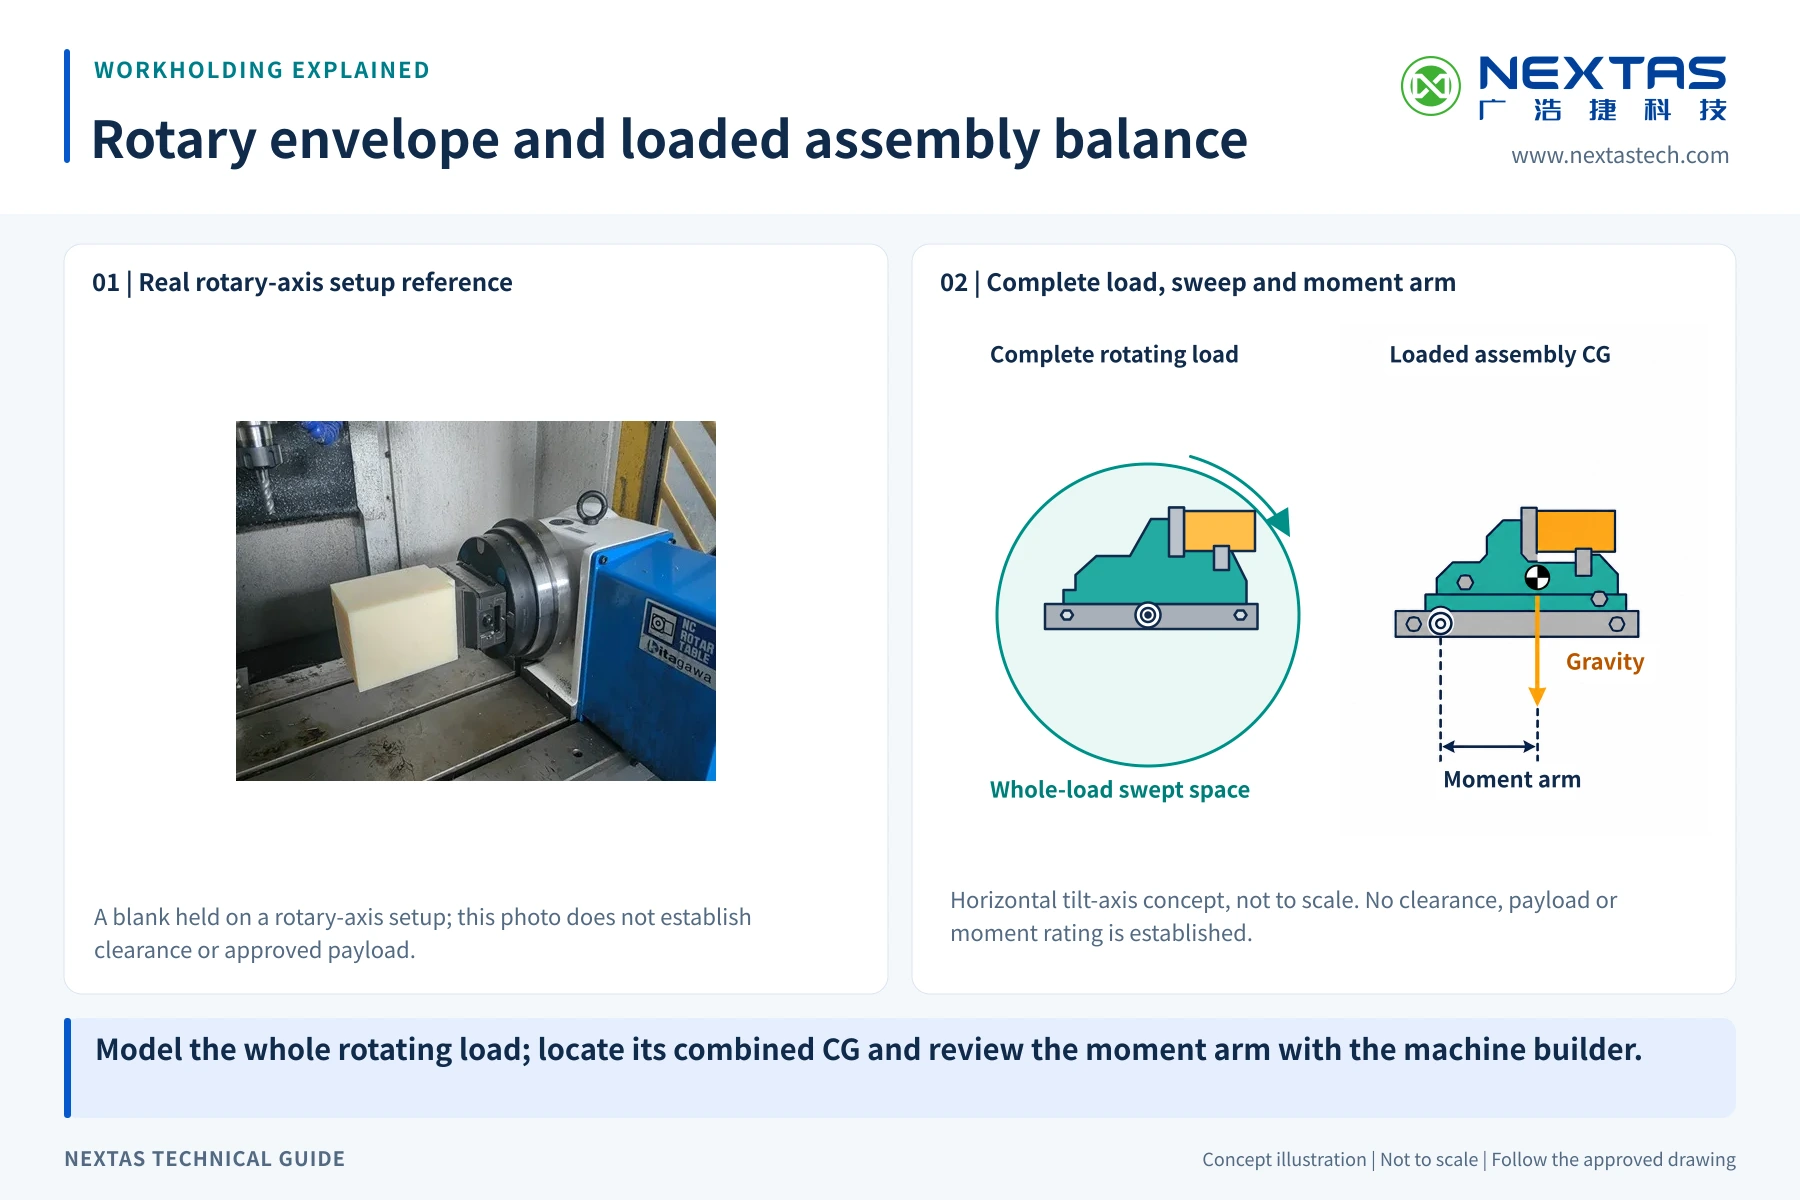
A rotary-table payload is not a vise-weight limit. Add the vise, jaws, part, adapter, plate, pull studs, fasteners and any other item that turns with the axis. Then locate their combined center of gravity. A load placed far from the rotary center creates a larger turning demand than the same mass held close to it.
Use the selected model drawing, not a family photo. For example, the current NEXTAS product data lists NT-S52P210V2 at 77 mm wide, 210 mm long, 87 mm high and 4.4 kg. It lists NT-S96P210V2 at 125 mm wide, 210 mm long, 111 mm high and 10.8 kg. Both list a 0–200 mm clamping range, but they belong to different force and mounting families. These values help size the stack. They do not select the vise for you.
| Named model | Published body size and mass | Buyer use |
|---|---|---|
| NT-S52P210V2 | 77 × 210 × 87 mm; 4.4 kg | Add its drawing, jaws, part and interfaces to the rotary model. |
| NT-S96P210V2 | 125 × 210 × 111 mm; 10.8 kg | Do not transfer its mass or family rating to an S52 model. |
Ask the machine builder for permitted mass, center-of-gravity position, turning moment and balance rules. Check any speed reduction or position limit required for an offset load. The machine owner must approve the result for the exact trunnion, table and program.
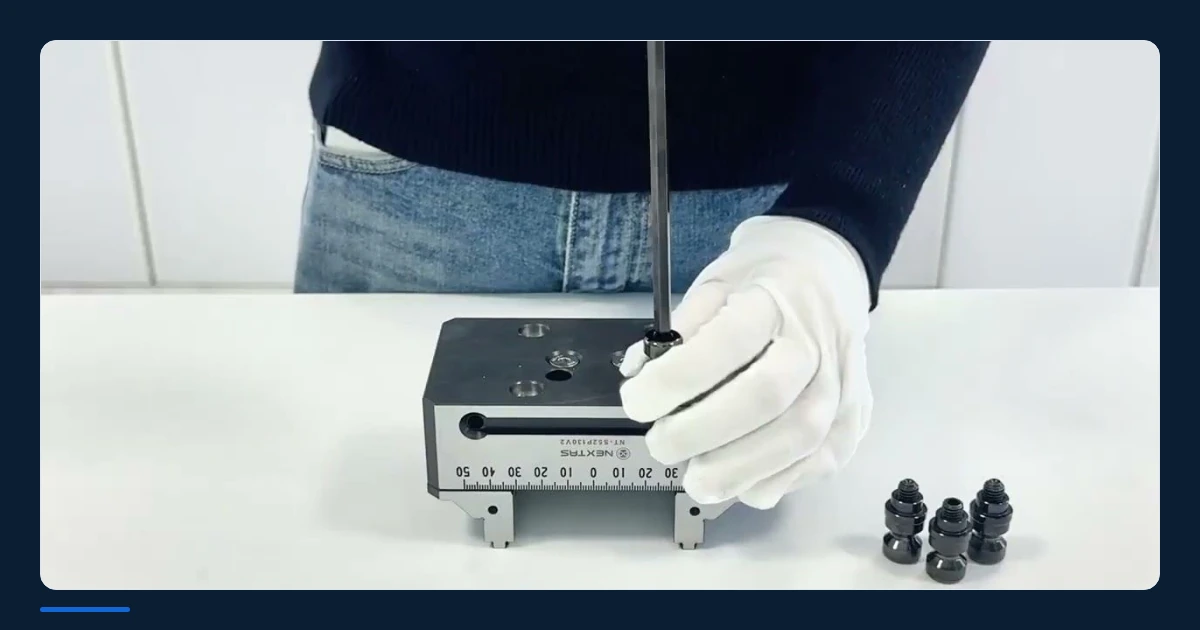
Use the setup video for orientation only
A 1-minute 52-second hands-on view of setup and adjustment steps for a NEXTAS 5-axis self-centering vise.
Release the first cut in controlled steps
First, close the paper gaps. Freeze the part revision, stock size, machine, rotary table, mounting stack, vise model, jaws and tool list. Mark the proposed jaw contact and grip depth. Record the total rotating mass and center of gravity. Set clearance, inspection and part limits before anyone runs the program.
Second, review motion off the machine. Use the best available machine and setup geometry. Check stock and finished shapes. Include open jaws, tools, holders, spindle, probe and loading access. Have a named person approve the result. Simulation can find many conflicts, but it does not prove the real setup matches the model.
Third, inspect the actual assembly. Clean and seat each interface by the approved method. Confirm fasteners, jaw installation, stock location and tool data. Keep people outside the hazard area. Follow the machine builder's procedure and the shop's safety rules. Do not defeat guards or normal protective functions to gain a better view.
Now run the planned positions without cutting and at the safe speed set by the machine owner. Use single block or another approved prove-out mode where required. Keep the tool clear until the motion, offsets and rotary direction are confirmed. Then cut one representative first article under written conditions. Inspect the agreed features and look for part movement, jaw marks, poor access and chip packing.
Release production only when the process owner accepts the first article and records the setup. If a tool needs an unplanned approach, the part moves, the machine load is unclear, or a limit is missed, stop. Revise the drawing, jaws, program or setup, then repeat the affected checks.
Send geometry and release limits for a useful review
Send NEXTAS the part model and drawing, raw-stock size, material and required machined faces. Add the machine and rotary-table drawings, axis limits, table payload rules and planned mounting stack. Include the chosen tools and holders, jaw contact sketch, grip depth, part and fixture masses, and center-of-gravity estimate. State the clearance margin and first-article limits your team will use.
NEXTAS can compare those inputs with the selected vise drawing and identify open questions. Final machine motion, cutting conditions, safety and production release remain with the machine builder, integrator and process owner.
Need a model-specific check?
Share the part, rotary table, tool and jaw plan
We can review the supplied geometry against a named NEXTAS vise and list the drawings and unknowns needed before a quote.
Questions buyers ask before the first cut
What should I send to check 5-axis vise clearance?
Send the part model, stock size, finished shape, machine and rotary-table drawings, vise and adapter drawings, jaw plan, and the longest tool and holder assemblies. Include the rotary limits and any probe or loader that enters the same space.
How much grip depth is enough for a complex 5-axis part?
There is no safe universal depth. Grip must suit the material, contact shape, cutting direction, jaw style, support and allowed clamp load. Mark the proposed contact on the part drawing, then approve it through process review and a controlled first article.
Does vise repeat positioning equal finished-part accuracy?
No. A vise value belongs to the named model and stated test. Finished-part accuracy also depends on the machine, rotary axes, mounting stack, jaws, part, tools, program, temperature and inspection method. Set part limits separately.
How should rotary-axis load be checked?
Add the mass of the vise, jaws, part, adapters, fasteners and any plate. Locate the combined center of gravity and check it against the machine builder's permitted mass, moment and balance rules at the planned positions. Do not compare the vise weight alone with the table payload.
Does a compact vise clear every 5-axis tilt angle?
No. The part, open jaws, toolholder, spindle nose, adapters, table and enclosure move through different paths. Check the full geometry at every indexed or simultaneous position used by the program, then confirm the result on the actual machine at safe speed.
What should the first-cut release trial include?
Start with drawing and simulation review, then dry-run the planned positions with the tool clear. Load one approved blank, use the written clamp method, cut a representative first article, and inspect the agreed features. Release production only after the owner accepts the results and records the setup.