Pay more only when the plate removes a limit you can measure
A higher-priced plate is worth considering only when it solves a requirement you can name and test. You may need wider support for a large fixture. You may need a lower stack for tool clearance or a chosen release method. You may also need a model whose stated load data fits the planned duty. “High-performance” alone is not an engineering specification.
Start with the exact part number. Trace the forces from the part, through the fixture or pallet and pull studs, and down to the machine table. Mark the plate or receiver modules and mounting bolts in that chain. Check the support count. Check the full stack height. Confirm how the plate will release. If the premium option does not improve a known limit in that chain, there is no technical basis for paying more.
A defensible approval has three parts:
- A selected model and drawing that match the interfaces.
- A reviewed load, support, stack-height, mounting, and release plan.
- An acceptance test with pass limits agreed before installation.
Draw the load path before comparing force
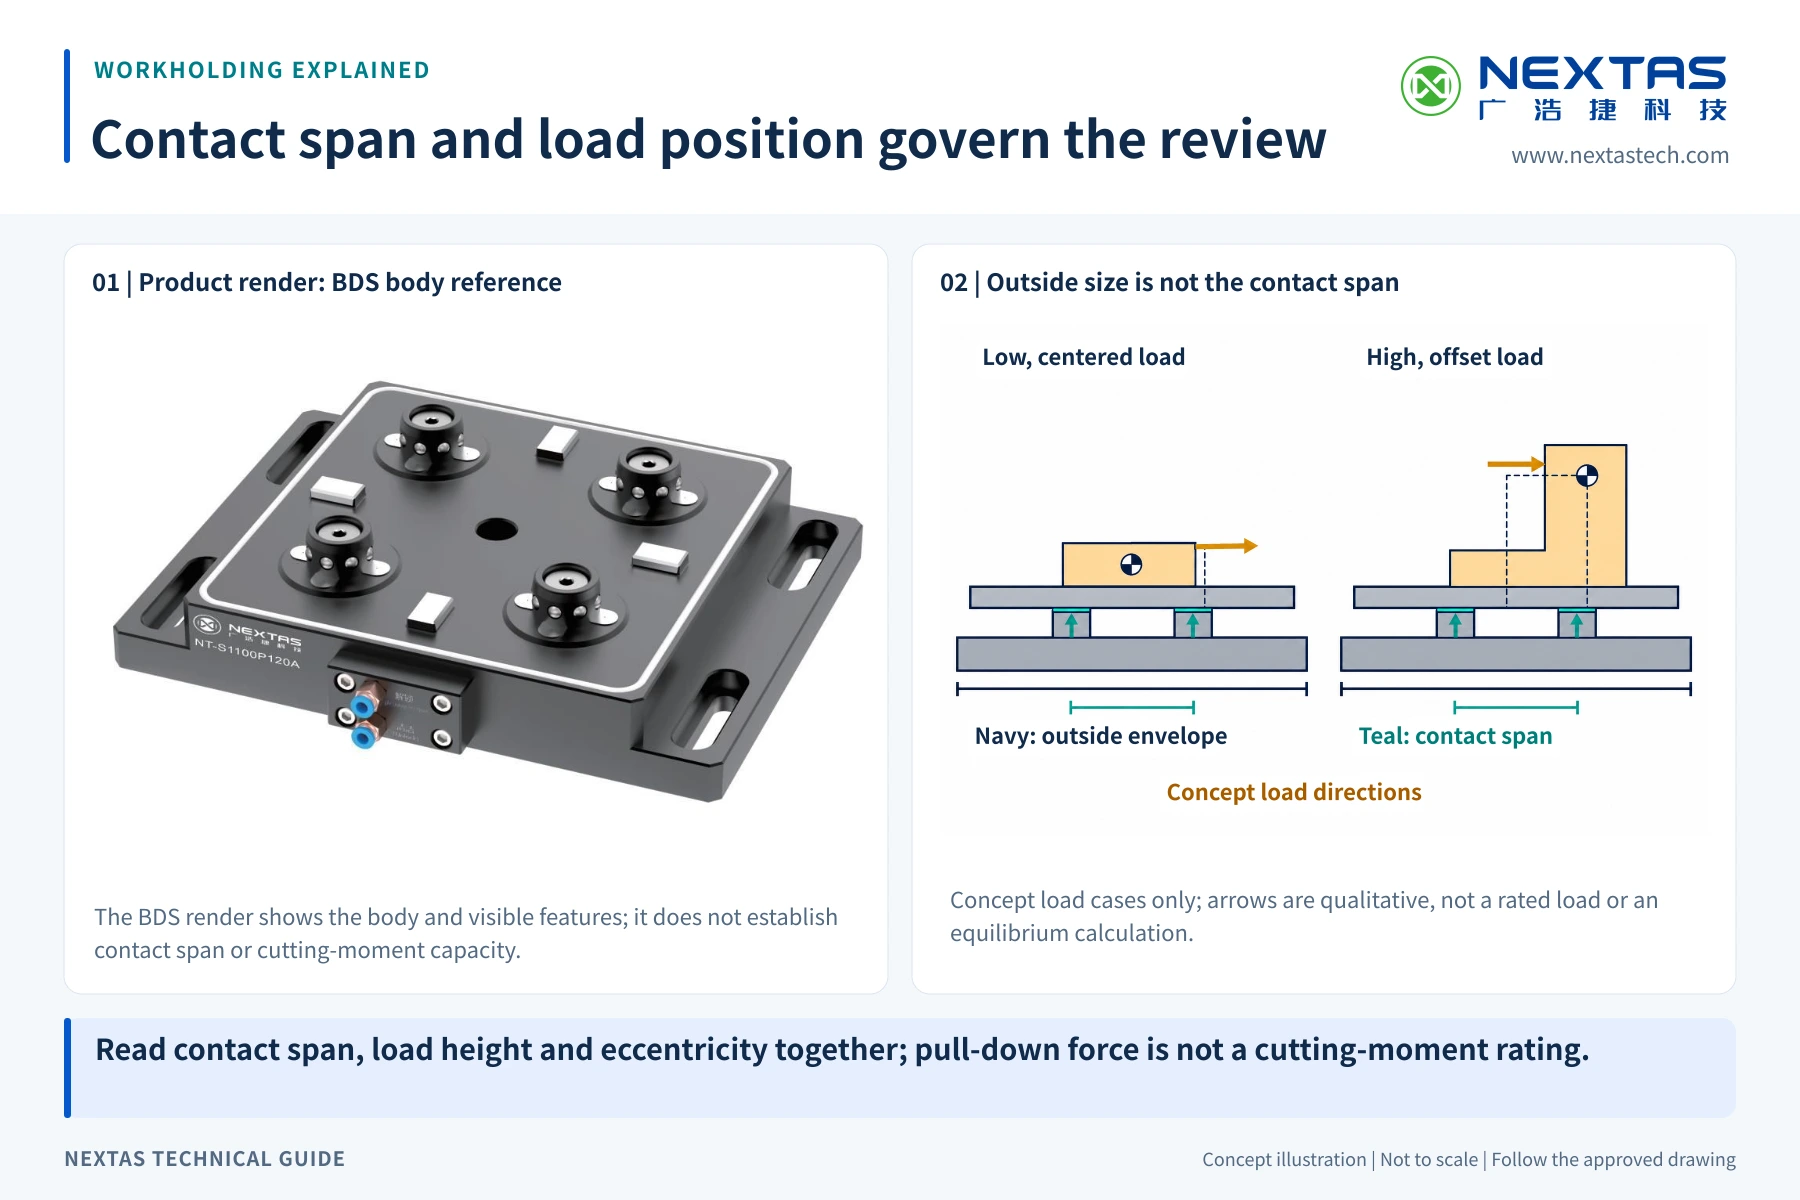
A catalog clamping-force value tells you something about the named plate or family. It does not describe the whole fixture. Cutting force can act sideways, upward, or as a turning moment. A tall part can raise the demand on the interface. So can an offset vise or a pallet that overhangs its supports. The same weight set low and central creates a different case.
Sketch the chain from the cutting area down to the machine table. Mark the workpiece and fixture mass. Add the center of gravity and likely cutting directions. Show unsupported spans and the distance from the load to each support. Also mark where the base is bolted to the table. The key question is simple. Can the layout carry the real duty without relying on one headline number?
Do not add force ratings from unrelated products or assume that a lifting-load figure is a machining-load limit. The manual plate page, pneumatic plate page, and receiver-system page describe different hardware families. Keep each value with its stated model or family and ask NEXTAS to review the complete layout.
Keep every number attached to the exact model
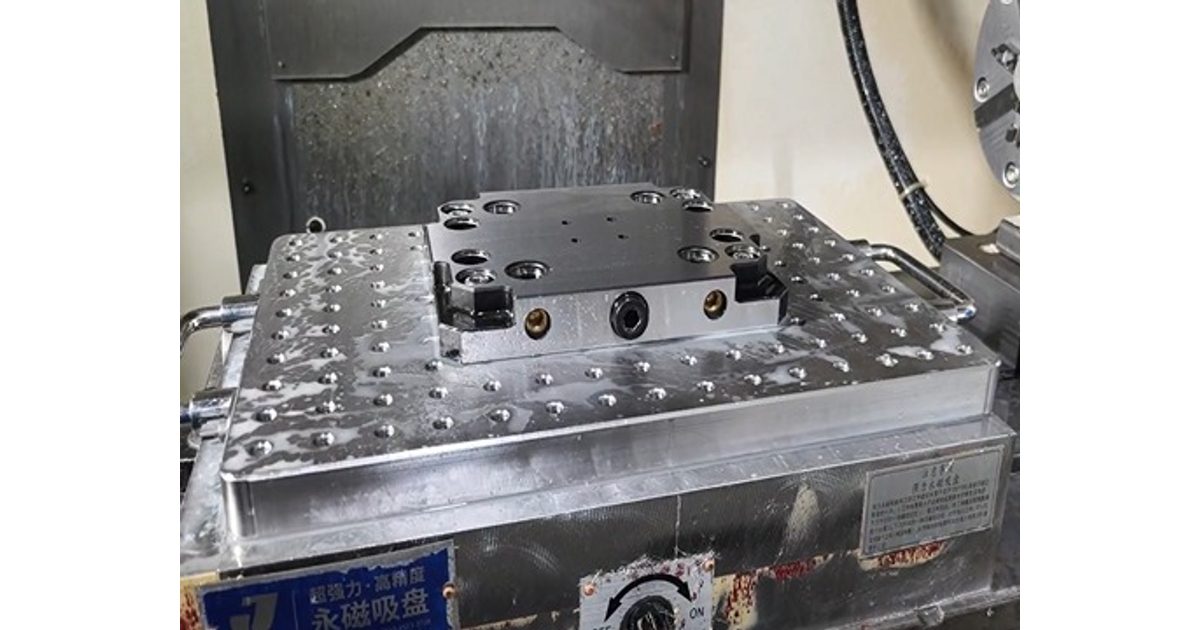
The examples below are intentionally not a size ladder or a recommendation. They show why “52 mm,” “96 mm,” and “pneumatic” are not enough for purchasing. Model, station layout, release method, matching stud, and stated rating must stay together.
| Selected model | What the source page states | Buyer boundary |
|---|---|---|
| NT-S52P208V1 | Manual P208 four-station plate. 52 mm family. 20,000 N. Matching stud NT-S52P16V1. | Use the family value only with this manual plate context. |
| NT-S96P330V2 | Manual P330 four-station plate. 96 mm family. 30,000 N. Matching stud NT-S96P20V1. | A larger family value does not prove the mounted stack is suitable. |
| NT-S52P229QD1 | Pneumatic 52 mm plate. 18,000 N. Stated lifting load: 200 kg. Release pressure: 0.5–0.8 MPa. Stud: NT-S52P16V1. | The lifting value is not a general machining-load rating. |
| NT-S96P392QD1 | Pneumatic 96 mm plate. 40,000 N. Stated lifting load: 660 kg. Release pressure: 0.5–0.8 MPa. Stud: NT-S96P20V1. | Do not transfer these maximum model values to other pneumatic plates. |
For a quote, use the current product drawing and specification for the chosen part number. The table is a reading aid based on the linked manual plate and pneumatic plate pages, not a substitute for model confirmation.
Support count follows the footprint and turning moment
One central interface may suit one compact fixture. A long base may need supports set farther apart. The same may be true for a wide pallet or an off-center load. The purpose is not simply to collect more clamping force. It is to support the real load path and limit the open span.
Ask for a top view with the fixture outline and center of gravity. Mark the pull-stud locations and proposed supports. Then check edge distance, bolt access, and chip escape. Make sure every support can seat on the same prepared plane. More supports also create more interfaces to clean and verify. Their benefit depends on the layout and its installation.
The separate zero-point receiver-system range includes multi-station layouts. Those receiver-system specifications must remain separate from manual and pneumatic plate figures. The layout idea may help a discussion, but only the selected compatible components can define the proposal.
Stack height and mounting can erase the advantage
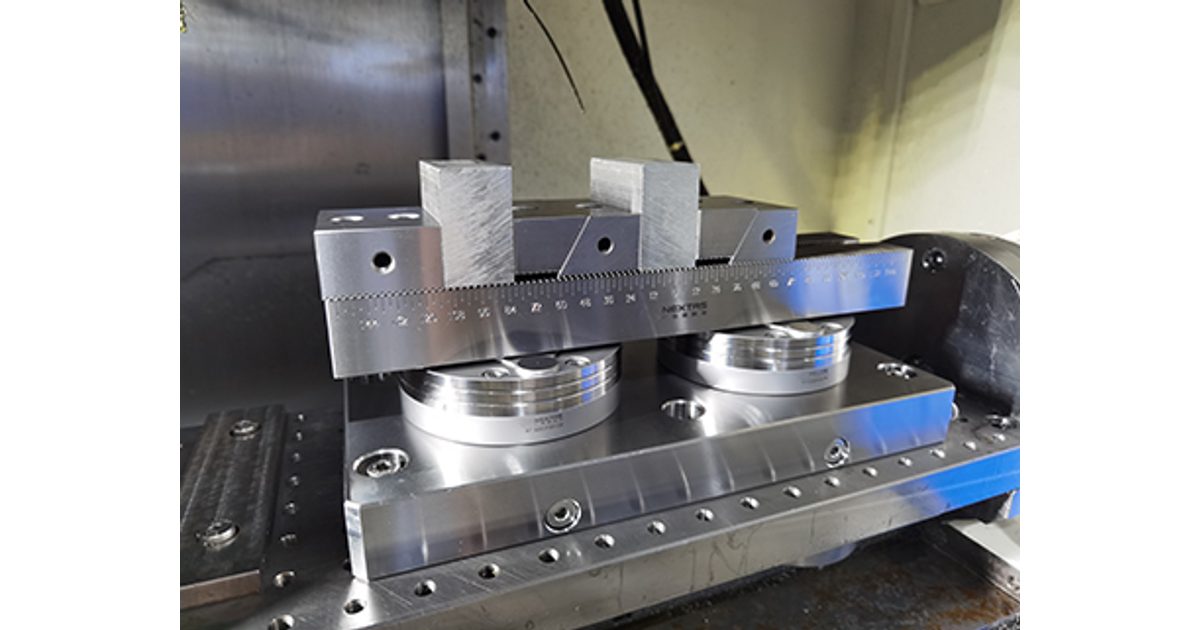
Stack height is the added distance between the machine table and the workpiece. It includes the plate, pallet, adapter, fixture, and jaws. A taller stack may improve access in one job. Yet it may cut tool reach or machine clearance in another. It can also move the cutting point farther from the table. Review that shape in the real work envelope. The plate name cannot settle it.
Put the complete stack into the machine layout before ordering. Check spindle, toolholder, rotary table, enclosure, probe, and loading clearance. Include the tallest part and the longest tool assembly planned for the job. If a raised plate or adapter is proposed, compare that exact drawing rather than estimating from a family photo.
Mounting deserves the same attention. Confirm the table type, bolt pattern, datum strategy, fastener access, seating-plane condition, and installation procedure. Record any adapter plate and its thickness. A premium plate mounted on an unknown or poorly prepared base has not solved the original problem. Ask who owns the mounting drawing and who will verify it after installation.
Choose manual or pneumatic release from the process
The NEXTAS manual 52 mm and 96 mm plate families use manual unlocking and list different family clamping-force values. Pneumatic plates use a spring-locked mechanism with pneumatic release, while force and lifting data vary by exact model. These are different choices, not one scale on which pneumatic always means better.
Manual release may fit a process with an operator present and controlled changes. It also keeps the service plan simple. Pneumatic release may be worth the added hardware when changes are frequent. It may also fit an automated sequence. The buyer must still define the air supply, valve state, sensing, and interlocks. Cleaning and recovery after lost air or an incomplete release also need a plan. The product page lists a 0.5–0.8 MPa release range for its named pneumatic models. That value does not replace a cell-level controls and safety review.
Use the video for orientation, not acceptance
A 14-second product view of the NEXTAS manual zero-point plate system.
Watch on YouTube
Set release checks before approving the premium
First, close the paper gaps. Name the plate, matching stud, and fixture or pallet. Add the support layout, total stack height, mounting interface, and release method. State the expected service conditions. Record the workpiece and fixture mass, center of gravity, cutting directions, and pass limits. Keep an unknown marked as unknown until the responsible engineer confirms it.
Second, verify the installation without cutting. Inspect the mounting plane and interfaces. Follow the stated fastening procedure, seat the fixture, and check access to the release control. Cycle the planned exchange sequence. Make sure the fixture reaches its datum and releases as intended. It must also recover from the agreed fault cases. For pneumatic use, test the approved response to lost air and an incomplete sequence. Follow the cell integrator's safety plan.
Third, run representative work under set conditions. Record the setup, tool, program, material, and inspection method. Repeat exchanges and inspect the parts. Compare the results with the limits set before the test. Include the shop's approved cleaning routine. Run a controlled contamination check only if the responsible team has defined a safe method. A product photo, short video, or unloaded cycle cannot replace this evidence.
- Pass: the selected model and complete stack meet the written limits in the agreed test.
- Revise: mounting, support placement, stack, release controls, or cleaning steps need a documented change and retest.
- Stop: the exact interface, load case, safety response, or acceptance limit remains unknown.
Build the commercial case from accepted evidence
A premium option becomes reasonable only after the technical need is clear. Compare the full installed scope. Include the plate, studs, adapters, and extra pallets. Add air preparation, valves, sensors, integration, installation, training, and planned maintenance. Then compare that scope with the standard option that fits the same job.
Use your own production records for change frequency, setup labor, machine waiting, inspection, scrap, and recovery events. Do not turn a catalog force value into a payback promise. A larger or more automated plate may create value in one process and add cost or complexity in another. The decision is credible when the expected benefit is tied to an observed constraint and the installed system passes the agreed checks.
Before requesting a price, be able to answer:
- Which exact standard option fails which written requirement?
- Which selected premium model addresses that requirement?
- What new hardware, services, and controls are included?
- What evidence will decide acceptance?
Compare plates for your setup
Include the machine model, fixture size and the constraint behind the enquiry—load support, available height or release method. From there, we can compare suitable standard plates and work out whether a custom design is justified.
Also state what must be verified before purchase and during commissioning. That lets the discussion start with a compatible model and an evidence plan instead of a generic premium claim.
Need a model-specific review?
Share the load path, mounting drawing, and release sequence
NEXTAS can review the supplied inputs against the relevant product family and identify the drawings, open questions, and checks needed for a quote.
Questions buyers ask before paying more
What makes a zero-point plate high-performance?
High-performance should describe a verified fit for a demanding job. It is not just a label. The selected model must suit the load path, support layout, stack height, mounting interface, and release method. It must also meet the pass limits on the actual machine.
Does higher clamping force guarantee a more rigid setup?
No. A force value belongs to a stated model or family. Setup behavior also depends on support spacing, overhang, fixture stiffness, mounting, and the full stack. Compare the exact model. Then test the mounted assembly under representative work.
How many support points does my fixture need?
There is no safe universal count. Place enough compatible supports under the real fixture footprint. They must control the load and turning moment. Have the layout reviewed against the selected hardware, then prove it on the machine.
Should I choose manual or pneumatic release?
Manual release can suit attended changes and simple services. Pneumatic release can suit frequent or automated changes. The exact plate, air supply, valves, sensing, interlocks, and fault recovery still need review and validation.
Do 52 mm or 96 mm labels prove that parts are compatible?
No. A family label is only a starting point. Confirm the exact pull stud, locating geometry, and bolt pattern. Also check the seating surfaces, fixture clearance, stack height, and model drawing before ordering or mixing parts.
What should a zero-point plate acceptance test include?
Record the selected model and mounted stack. Use a representative fixture and load. Repeat seating and release cycles, then inspect the parts. Test the agreed cleaning and fault-recovery steps. Set pass limits before the trial.