Decide the upper clamp, then decide if the fixture must leave the machine
Start with the part. Decide how the stock will be held while the tool reaches each cut. That is the job of a dovetail fixture, a self-centering vise or a custom upper fixture. Then ask whether that upper fixture must leave the machine and return to a known location. That second job may call for a zero-point base.
These are not three equal substitutes. A dovetail fixture and a vise touch the workpiece. A zero-point base normally sits below them and connects removable tooling to the machine. A shop may use a dovetail fixture alone, a vise alone, or either one on a zero-point interface. The right answer comes from the full stack, not a product name.
When the stack is clear, send the part, the machine, and the layer that must leave the machine on the workholding quote.
Leave the first review with one simple sketch:
- Show the raw stock, finished part and surfaces that may be clamped.
- Show the tools, jaws or dovetail contact, and support under the cut.
- Show every layer from the machine table to the part.
- Mark which layer must be removed, stored or moved to another machine.
- List the drawings and trials needed before purchase release.
If you have already chosen a zero-point architecture and need to select a named receiver, mating interface and acceptance plan, use the separate zero-point system RFQ checklist. This article stops one step earlier.
Choose the upper clamp from the part and the cut
A workholding choice begins with the raw blank, not with a catalog photo. Mark the faces that must be cut. Mark the material that may be gripped. Add the main cutting directions, the longest toolholder and any probe used in the same setup. The clamp must hold sound material while leaving a safe path for those items.
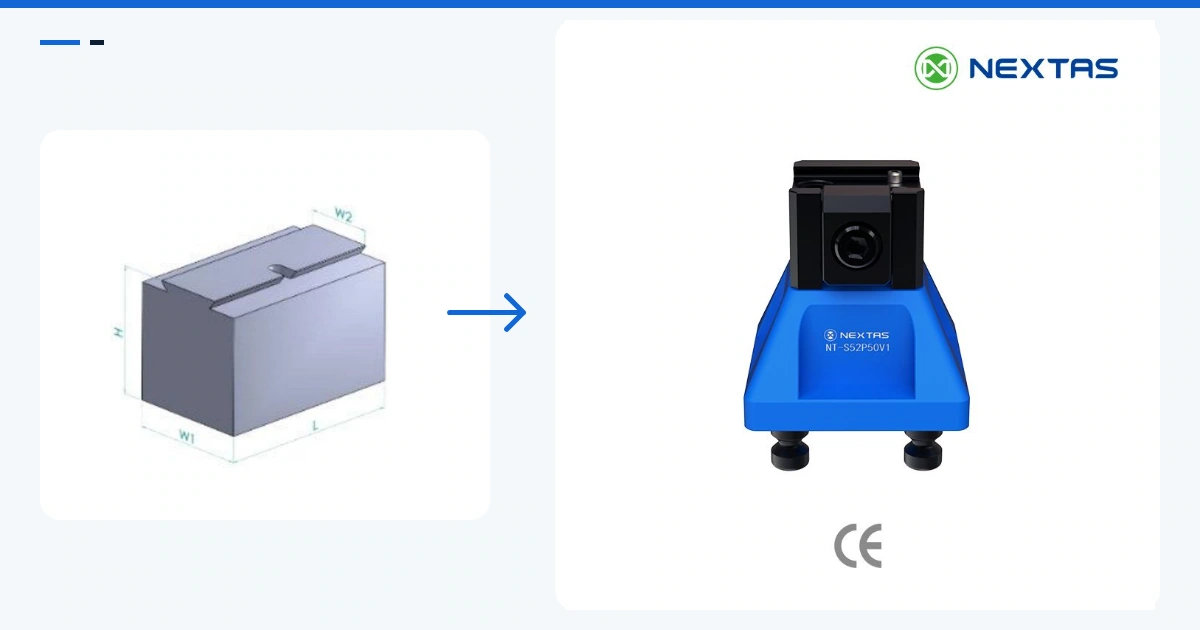
A dovetail fixture can suit stock that may receive a matching sacrificial profile. The profile becomes the contact between the part and fixture. This can leave several part faces open to the tool. It also adds a stock-preparation step. The buyer must control the profile drawing, remaining material, pull direction, support and the process that makes that profile.
A self-centering vise brings two jaws toward the part center. It can suit prismatic stock, repeat families and parts that benefit from centered loading. Yet the word “self-centering” does not prove that the part will stay on the program datum. Jaw contact, stock variation, soft-jaw form, grip depth and support still matter. A trial must use the real part and planned cut.
A custom fixture may be safer when neither option gives clear contact or support. Thin walls, cast shapes, finished surfaces and off-center loads can need shaped nests, added stops or more than two contact zones. Do not force a standard clamp into a part that lacks a clear load path.
Compare contact, access and preparation
Use the same part drawing for every option. A fair review does not compare a finished dovetail concept with an undefined vise setup. Give each route a contact plan, tool-access check and release test.
| Upper-tool route | Best first question | Evidence before release |
|---|---|---|
| Dovetail fixture | Can the stock carry a controlled sacrificial profile? | Profile drawing, remaining material, contact direction, support and a cutting trial. |
| Self-centering vise | Can two jaws grip sound material without blocking the tools? | Jaw drawing, contact depth, clamp setting, stock range, support and a cutting trial. |
| Custom upper fixture | Does the part need shaped support, extra stops or special location? | Fixture drawing, contact map, fastener plan, load review and first-piece inspection. |
Tool access is not just the tool tip. Check the cutter, holder, spindle nose and probe through each planned motion. Also check the stock before it becomes the smaller finished shape. A taller clamp may open one face but raise the part and increase the turning effect on a rotary axis. A shallow grip may improve access but remove needed support.
Do not use a fixed rule for grip depth or clamp load. Those values depend on the selected model, jaw or profile, material, cut and overhang. Treat published product data as an input tied to a named item. It is not a promise of finished-part accuracy or safe cutting on an unknown setup.
Add a zero-point base only when the fixture must move
A zero-point base creates a known machine-side interface for removable tooling. It may help when a shop prepares fixtures away from the spindle, changes repeat jobs, shares a defined pallet between approved machines or hands a known carrier to automation. It does not replace the jaws, dovetail contact or custom nest that holds the workpiece.
If the upper fixture stays on one machine for long runs, an added interface may bring little value. It adds height, mass, joints, fasteners and cleaning duties. The benefit must come from the real production route. Do not assume that one more quick-change layer will improve every job.
Before adding the base, draw the table pattern and every interface above it. Include the base, mating plate or pull studs, upper fixture, jaws, stock and tools. Record total height, mass and the combined center of gravity. Check support under the cutting load. A locator can return to a position while an unsupported plate still bends.
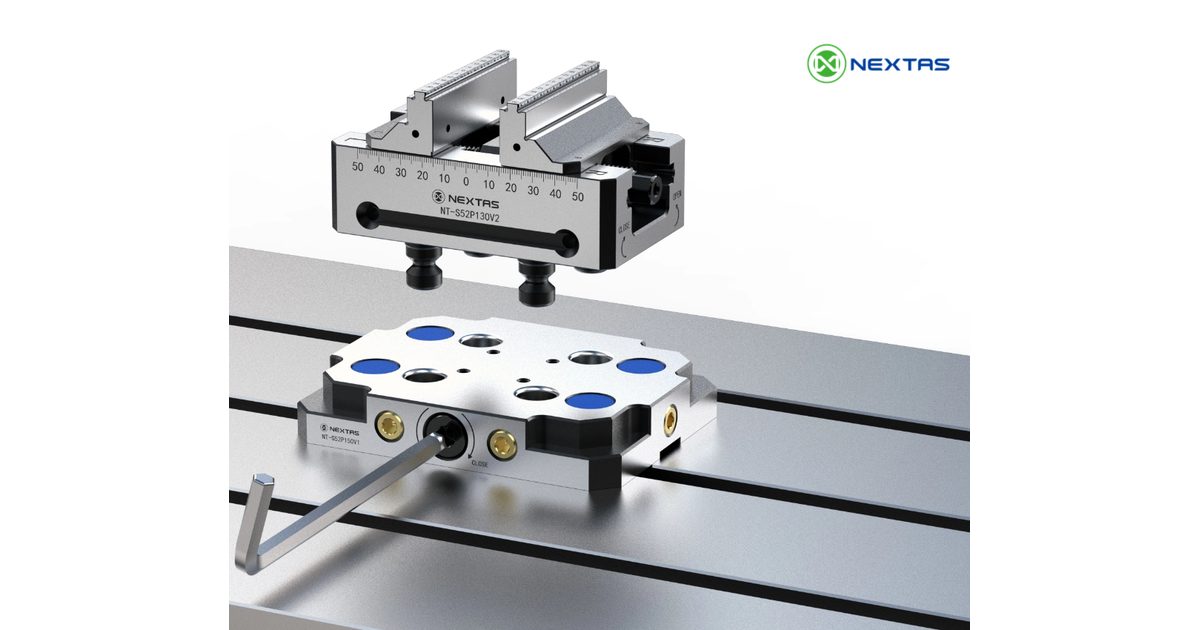
Pitch, diameter and a similar appearance do not prove fit. The buyer needs the exact base model, mating part number, drawing revision, stud geometry, mounting pattern and allowed options. If air or signals are involved, the approved circuit and machine response also belong to the stack review.
Use four routes to keep the choice clear
Route 1: dovetail fixture on the machine interface
Use this route when the stock can carry the planned profile, the tool can reach the cuts, and there is no need to move the fixture through a zero-point base. The drawing must still show how the fixture mounts and how the part is supported.
Route 2: self-centering vise on the machine interface
Use this route when jaw contact is clear, stock range is controlled and centered loading helps the process. Define the jaws, clamp setting, support and mounting. Do not release a family name without the exact vise model and drawing.
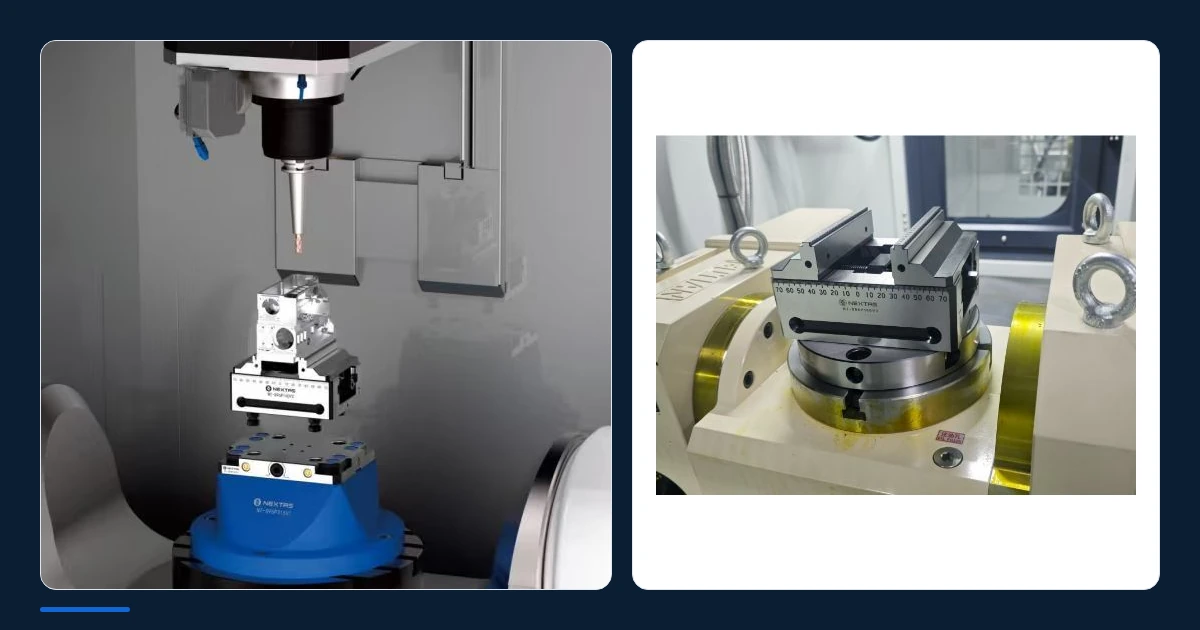
A 1-minute 52-second hands-on setup and adjustment demonstration.
NEXTAS self-centering vise setup demonstration.
Route 3: an upper clamp on a zero-point base
Use this route when the dovetail fixture or vise has passed its own part review and the whole upper tool must be removed and returned. Approve both interfaces. The upper clamp still needs a cutting trial; the base still needs a model and mating-interface review.
A 25-second view of a NEXTAS side-inlet zero-point arrangement.
Watch on YouTube
Side-inlet layout reference.
Route 4: custom upper fixture, with or without a base
Use this route when the part needs special contact, support or location. Add a zero-point layer only if the custom fixture must move. Keep custom design and machine-side relocation as separate approval gates.
Do not rank these routes with a generic changeover-time or return-on-investment claim. Record your current method, actual handling steps, inspection needs and safe staffing. Then run a timed trial in your own cell. This gives the buyer evidence that belongs to the plant instead of a borrowed promise.
Map the full workholding stack before you choose dovetail, vise or zero-point
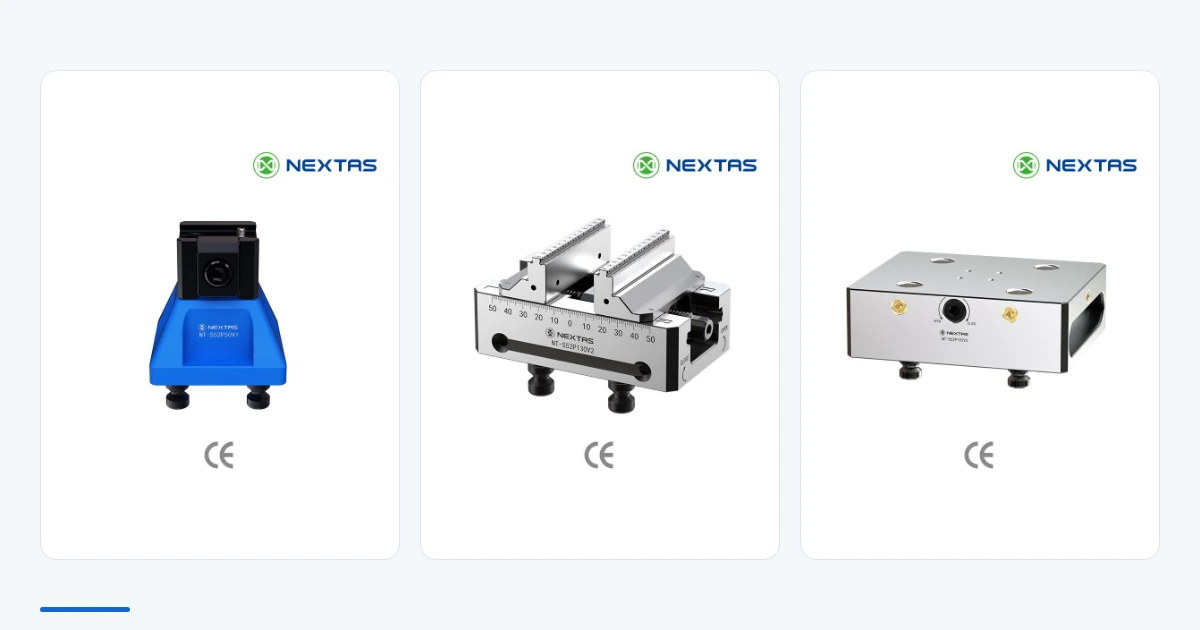
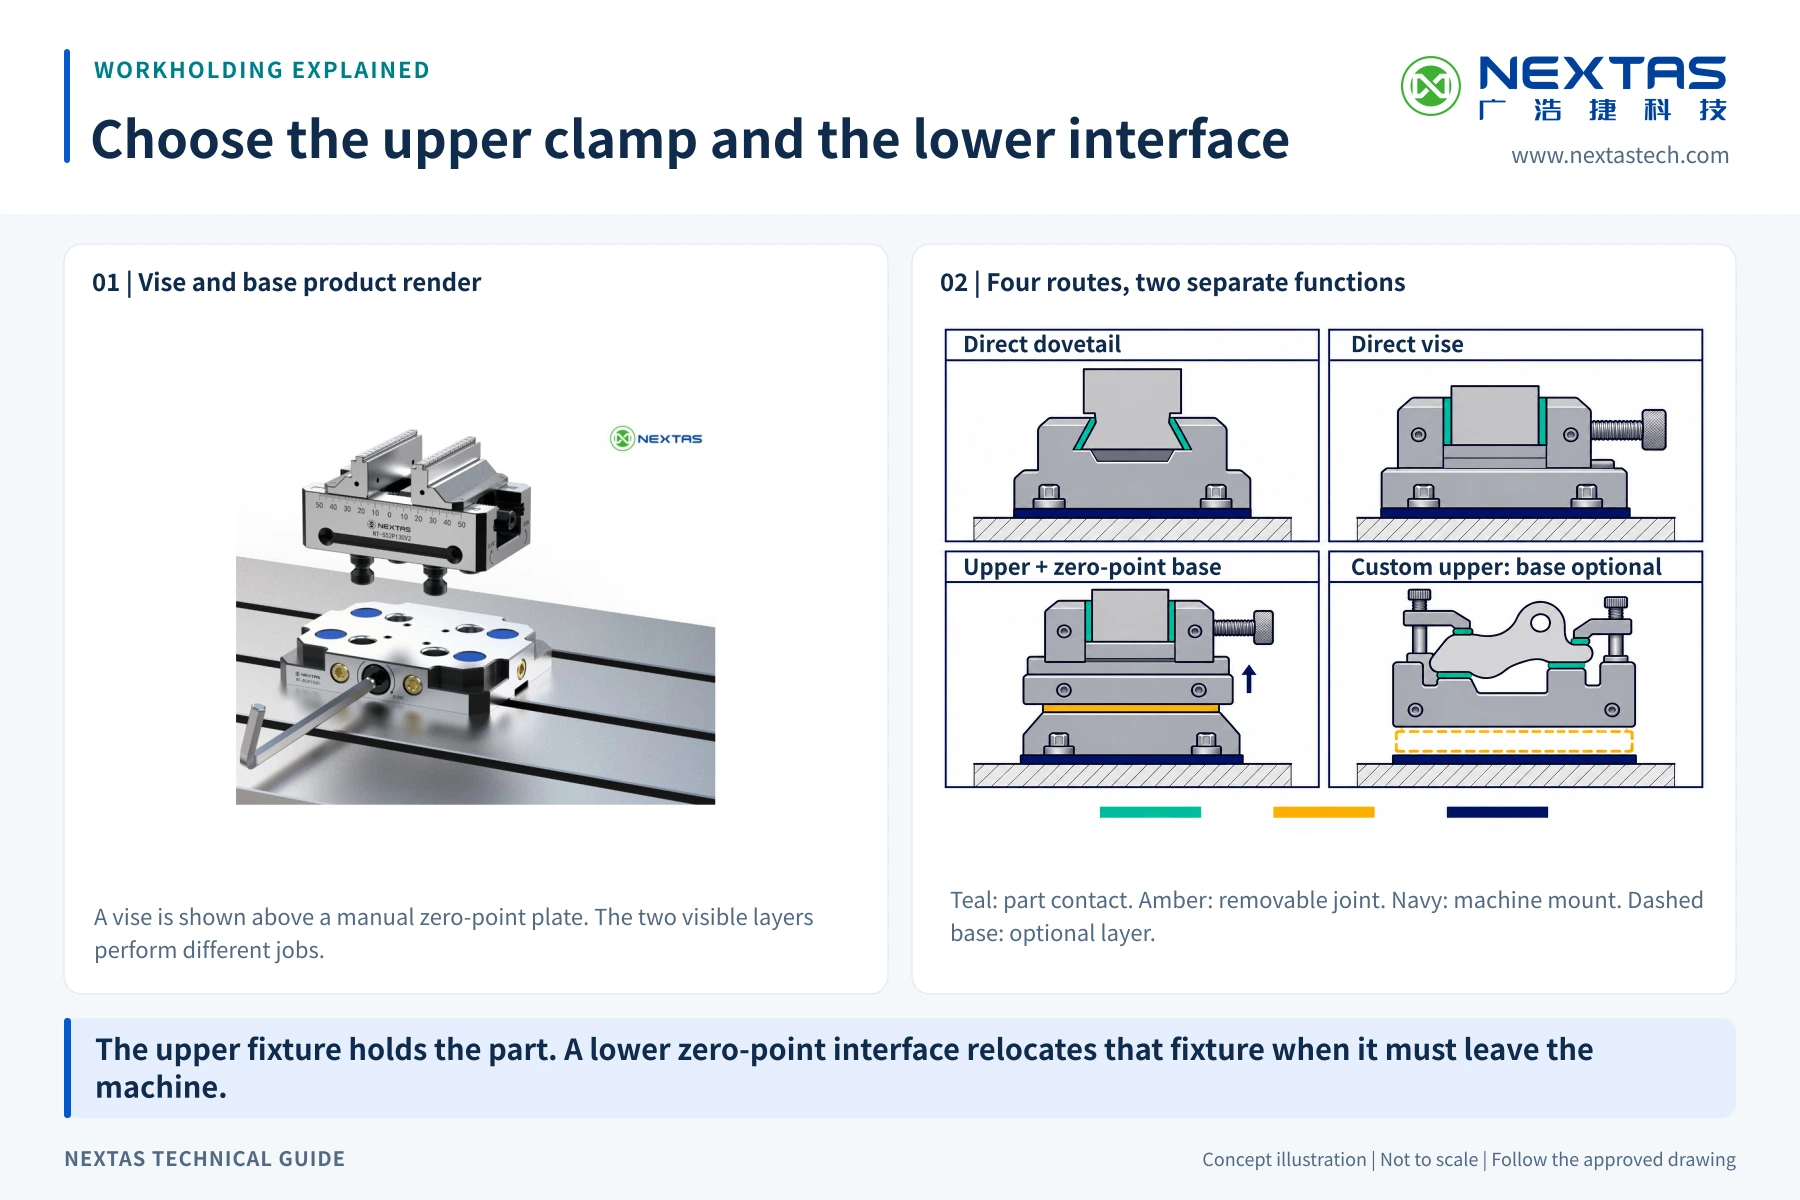
A dovetail fixture, a self-centering vise and a zero-point base do different jobs. A dovetail grips a prepared feature on the workpiece. A vise is the usual start when the part has clear jaw contact, the stock range is known and you do not want a sacrificial dovetail. A zero-point base locates removable tooling on the machine, so a dovetail fixture or a vise can be changed as a stack — each layer still has to fit on its own.
Write the stack from the table to the part before you choose: machine table or rotary face, adapter, zero-point base if used, mating plate or studs, upper fixture, jaws or profile, and part. Add fasteners, keys, stops, hoses and cables. A missing adapter or line route can change height, mass and clearance after the order is placed.
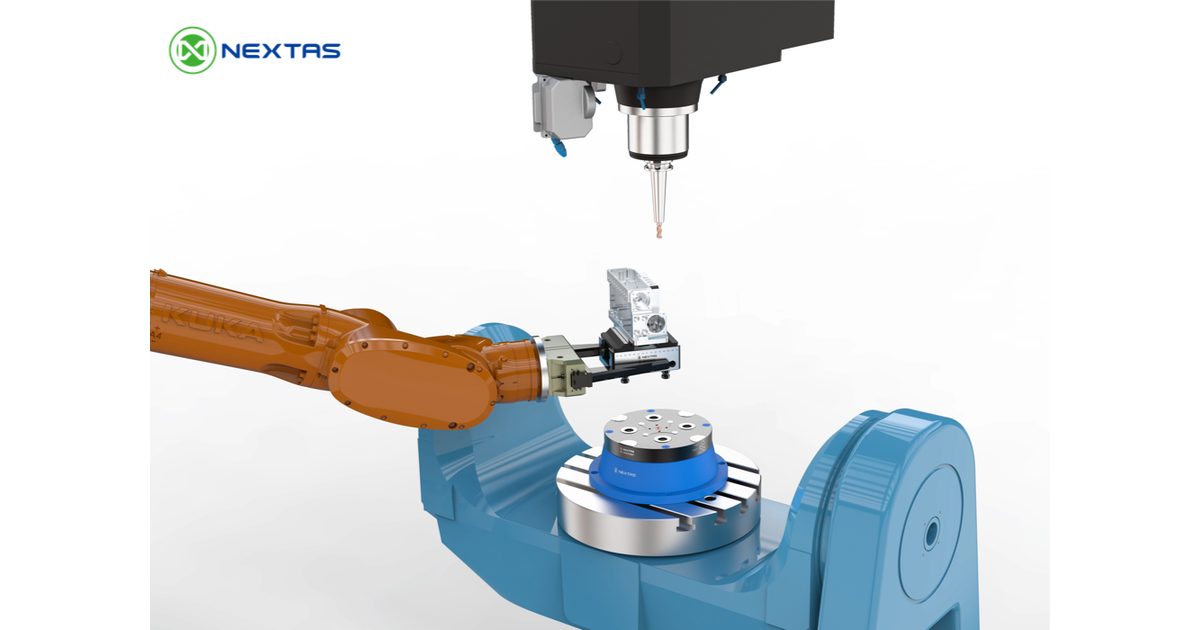
For robot loading, review the robot, gripper, workpiece, fixture, machine, signals, guards and recovery together. No single clamp or base establishes cell safety; the integrated arrangement needs its own validation.
Confirm the setup with a planned shop trial
A catalog claim will not tell you if the part will locate on your machine. Confirm the setup with a planned shop trial: document review, as-received inspection, a dry cycle, then a first piece.
Begin with document review. Confirm the part and stock revision, upper-tool model or design, machine-side interface and full stack drawing. Check tool access and machine motion in the approved engineering method. Confirm fasteners, clamp settings, support and any service connections.
Next, inspect the parts as received. Clean and mount them by the supplier's method. Check the location and seating features without adding an unapproved test contaminant. Run a dry cycle with cutting disabled. Use the machine owner's safe setup mode and keep people outside the hazard zone.
Then make a planned first piece. Start with a cut that the process owner has approved. Inspect the features that show location, support and distortion. If the fixture will be removed and returned, repeat that real sequence and measure the result with a stated method. The pass limit must come from the part and process, not a general catalog phrase.
Questions to ask before you choose the workholding setup
Are a dovetail fixture and a zero-point base alternatives?
No. A dovetail fixture grips a prepared feature on the workpiece. A zero-point base locates removable tooling on the machine. A shop can mount a dovetail fixture on a zero-point interface when both layers pass their own review.
When should I start with a self-centering vise instead of a dovetail?
Start with a vise when the part has clear jaw contact, the stock range is known and no sacrificial dovetail profile is wanted. Confirm the jaw drawing, grip, support, tool access and planned cut in a real trial.
When does a zero-point base add value?
It may add value when an approved upper fixture must be prepared off the machine, changed for repeat jobs or moved through a defined process. If the fixture rarely moves, the extra height, mass and interface may not help.
Does a zero-point base set finished-part accuracy?
No. It locates one interface in the stack. Finished-part results also depend on mounting, support, the upper clamp, stock, tools, machine, program, temperature and inspection method.
What drawings are needed before choosing the architecture?
Provide the part and stock, machine table or rotary interface, planned tools, upper fixture or jaw concept, and the full stack. Show motion limits, loading access and which layer must be removed or shared.
When should I request a custom fixture?
Request a custom review when a dovetail or two-jaw contact cannot give clear location, support and tool access. Thin walls, cast shapes, finished contact faces and off-center loads often need a part-specific plan.
Discuss the workholding for your part
The part and machining sequence will narrow the choice between a vise, a dovetail fixture and a custom arrangement. A zero-point base addresses another part of the setup: how the fixture connects to the machine and returns after a changeover. The machine model, a part or stock photo and the step you want to improve give us enough context to begin that comparison.