P75, P110, and P150 are on the pneumatic vise page. This note is only the air that has to reach them.
The wall gauge says 6 bar. Will four vises still clamp in 0.3 seconds? The gauge cannot answer that. It is one pressure, in one place, at one moment.
Three numbers, three jobs
Keep them apart. The average over a cycle can look comfortable while the clamp itself is short of air.
| Number | What it decides |
|---|---|
| Air used in one cycle | Average demand on the branch, and on the compressor. |
| Stroke-average flow | Air for one motion, divided by the time you allow, then the loads that overlap in that same window. That flow picks the filter, regulator, valve, and tube. |
| Lowest pressure at the fixture port during the worst overlap | Pass or fail. |
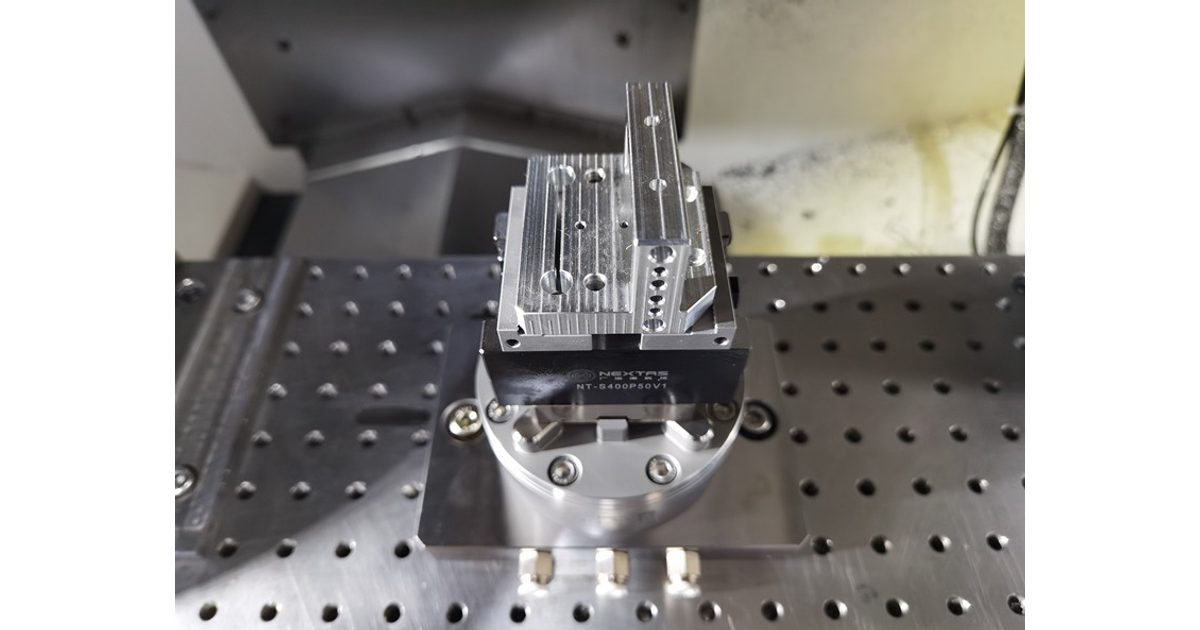
What a pass looks like
Both have to hold. The lowest pressure at the fixture port stays at or above the device minimum plus the margin for this project, and both the clamp and the release finish inside their time limits.
fixture-port minimum ≥ device minimum + project margin
FRL is three jobs, and flow comes from the curve
FRL means filter, regulator, and lubricator. Three functions. The device manual says which ones this circuit gets. Oil goes in only when that manual allows it. If the manual forbids oil, leave the lubricator off the line that feeds the device.
Port size names the thread. Read flow from the curve of the exact part, at the inlet pressure you have and at the flow the overlap asks for. Two regulators with the same port can lose different amounts of pressure.
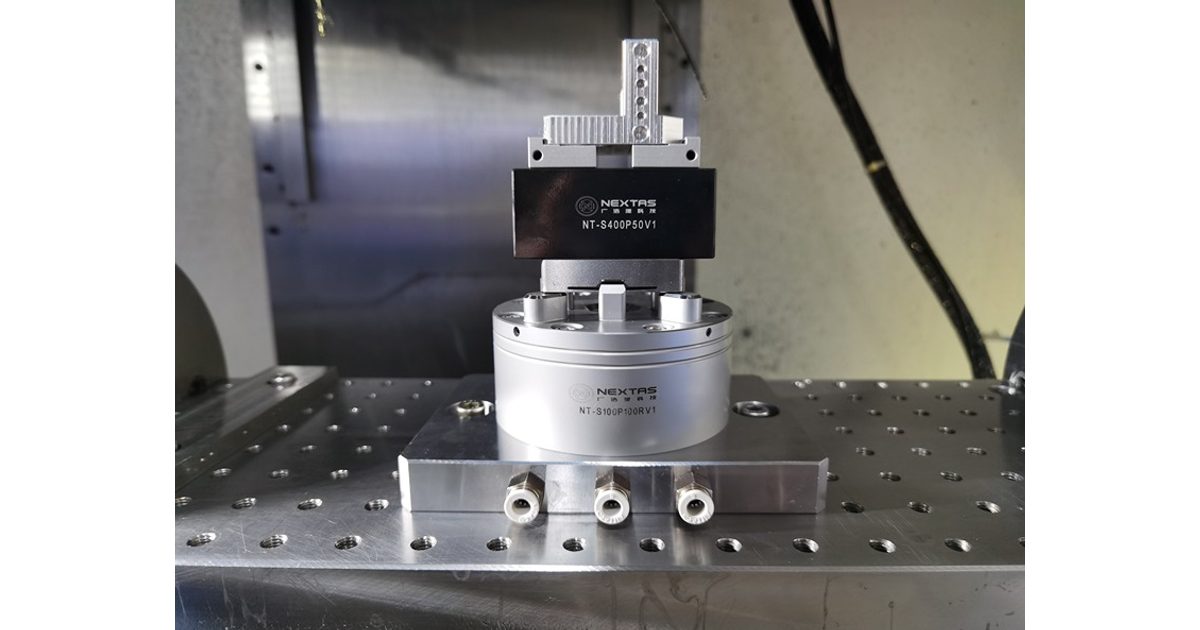
Measure the worst overlap
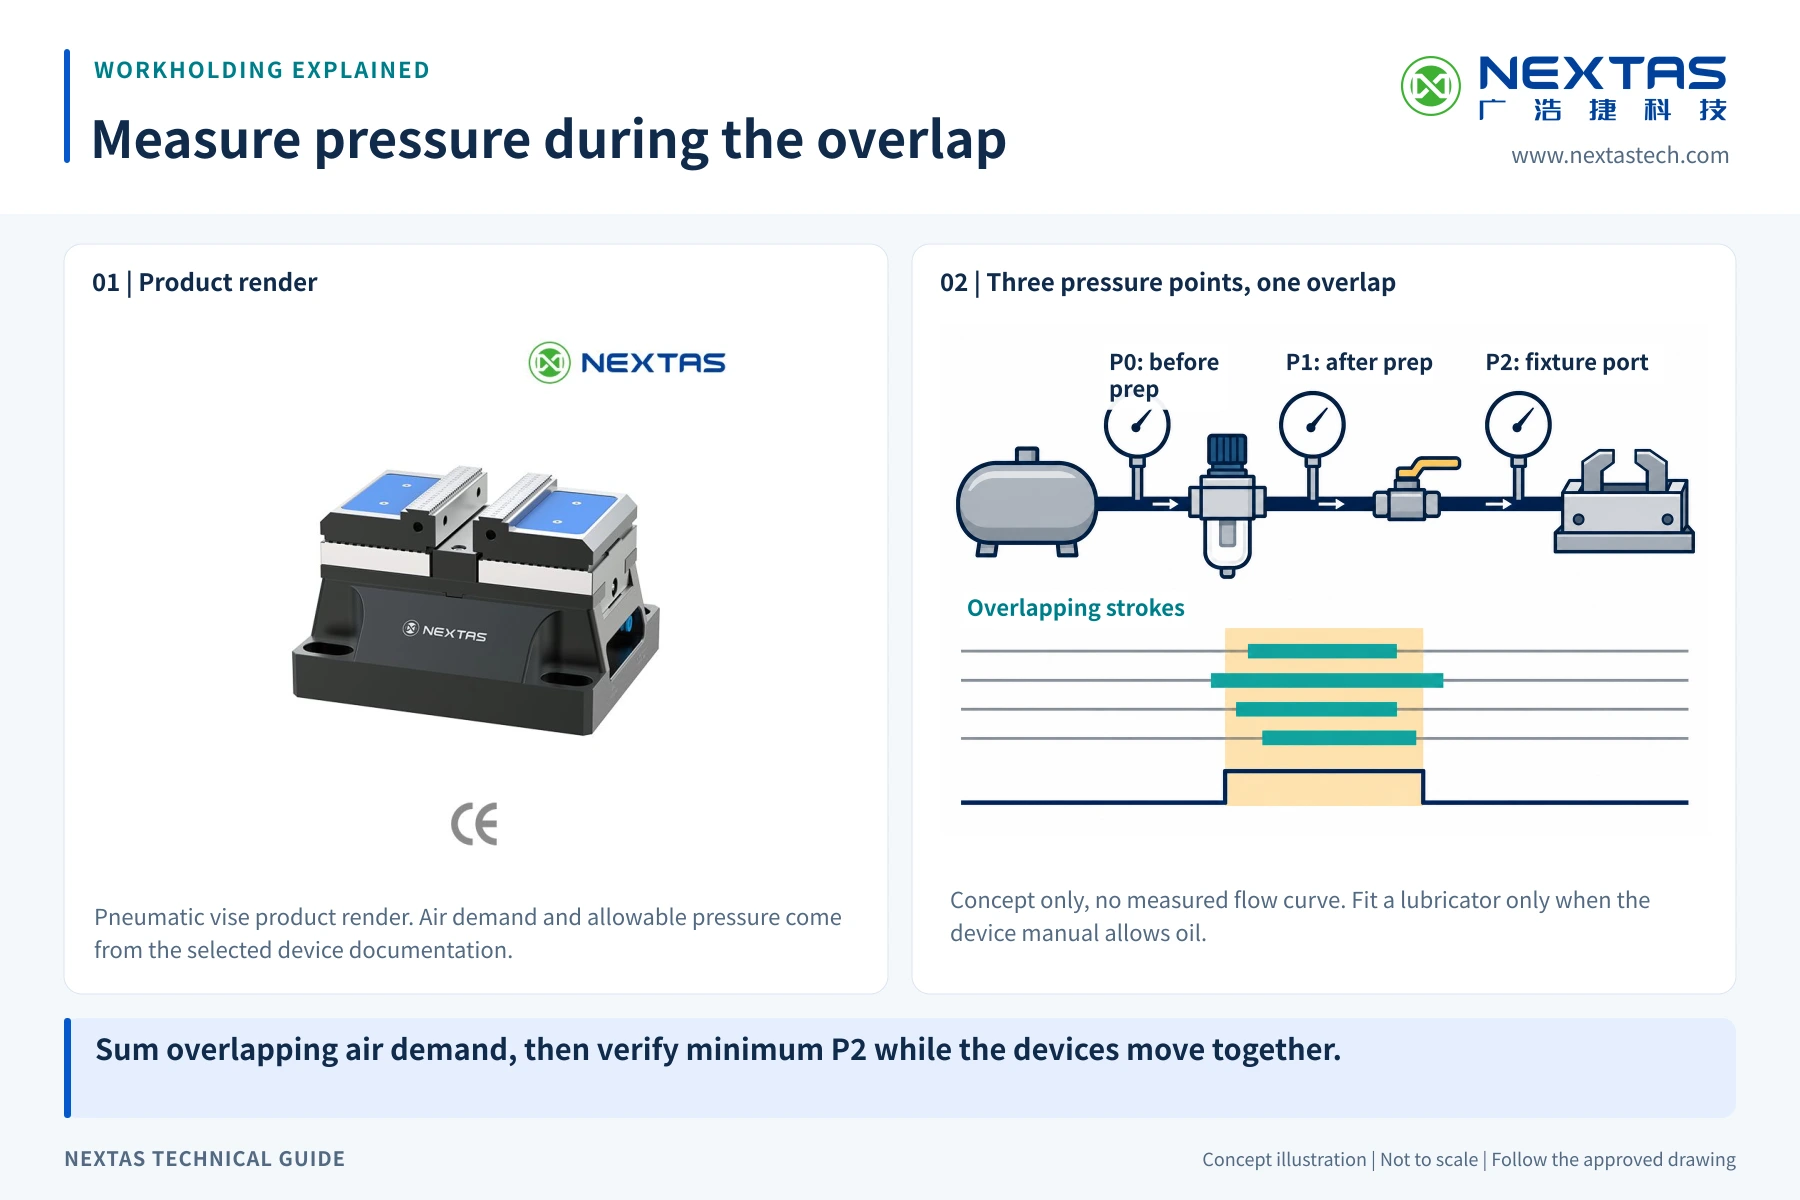
Log three points while that overlap is actually happening. P0 is before the air-preparation unit. P1 is after it. P2 is at the fixture port. The pass line above is P2.
A higher regulator setting leaves a blockage where it is. If P0 falls, the branch or the compressor is short. If P0 holds and P1 falls, look at the filter, the regulator, or the lubricator if one is fitted. If P1 holds and P2 falls, look at the valve, the fitting, or the tube.
An air tank covers only a short gap you can calculate, and only when it refills before the next event. A plugged fitting still has to be opened.
What to send with the quote
Send the device model and its circuit, the clamp and release times you need, the overlap timeline, the flow curves, and the P0, P1, and P2 record from the worst window.
The vise quote is on the pneumatic vise page. If the cell is more than the vise, start from the contact page. Around the air, see a pneumatic vise on a machining center, a pneumatic vise in an automatic cell, custom pneumatic fixtures, and a pneumatic vise as a machine upgrade.
One hypothetical event, labeled as a hypothesis
The catalog prints stroke 2.5 mm per jaw and air pressure 0.5–0.8 MPa for V1. It does not print NL/min or a bore. The example below uses a hypothetical bore of 40 mm. That bore is not a NEXTAS dimension. Free air is about piston area times stroke times (gauge pressure plus 0.101) divided by 0.101. At 0.6 MPa, inside the V1 band, one such event is about 22 cm³ of free air. That is not a published NEXTAS consumption.
Plate unlock pressure is not printed. The plate catalog cell says air pressure and does not give this 0.5–0.8 MPa band. The vise band does not apply to a plate. Oil in the FRL is allowed only when the device manual allows it. The pass line stays the pressure at the fixture port.
Four vises in the same window
Four vises that stroke in the same 0.3 s add their events in that window. They do not average across the shift. About 18 L/min appears only during that window, and only if the 40 mm bore assumption were true. Size the FRL and the valve for the overlap you measured, then confirm pressure at the fixture port while that overlap happens. A quiet average over an hour can hide the dip that opens a jaw.
Worked example: peak airflow and pressure at the fixture
For the quotation, record how many devices move together, how long the window lasts, which port you measure and whether the FRL manual permits oil. Keep the selected model data with the pneumatic vise article.