Core answer
A tooling column brings several fixture faces onto one base. Start with the machine and your part family, then choose the faces that give tools, loading and inspection the access they need.
Use this guide to compare column shapes, mounting options and standard models. The loaded envelope and machine load limits define which layout can work in your cell.
Start with the machine, not the column
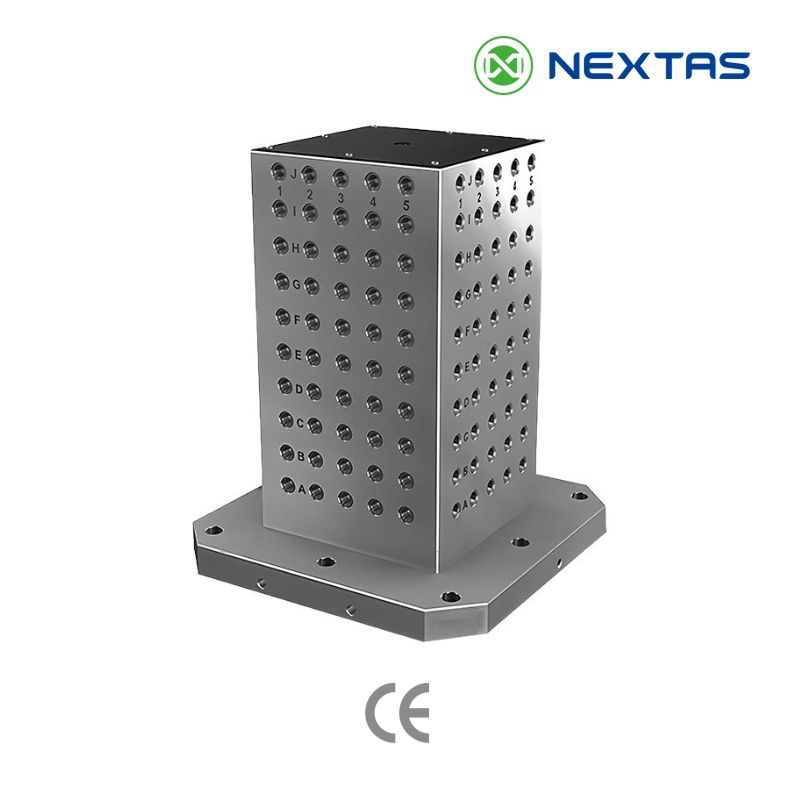
A CNC tooling column, also called a tombstone, is a multi-face base for fixtures and parts. The column may sit on an HMC pallet, a rotary table, a machine table or another approved adapter. It does not create more usable capacity by itself. The machine must be able to carry, turn and reach the complete assembly.
Ask for the machine builder's table or pallet drawing before choosing a model. Record the locating features, bolt pattern, available mounting depth and any fastener limits. Add the permitted table or pallet load. If the builder states a centre-of-gravity limit, keep that rule with the project file.
Then capture every moving limit. Use X, Y and Z travels, the rotary diameter or swing, spindle nose position, tool-holder length, door opening, pallet changer path and any probe or coolant hardware near the work zone. A catalog outline with no tools or parts is not a clearance study.
| Input | What to record | What it prevents |
|---|---|---|
| Table or pallet | Drawing, locating features, bolts and usable surface | An adapter that cannot locate or fasten |
| Axes and rotation | Travels, swing, index positions and changer path | A loaded face entering a restricted area |
| Spindle and tools | Nose, holder, cutter, probe and approach angles | A part that fits but cannot be reached |
| Load rule | Mass, balance and centre-of-gravity limits | Approval based on the bare column alone |
Choose usable faces, not the highest face count
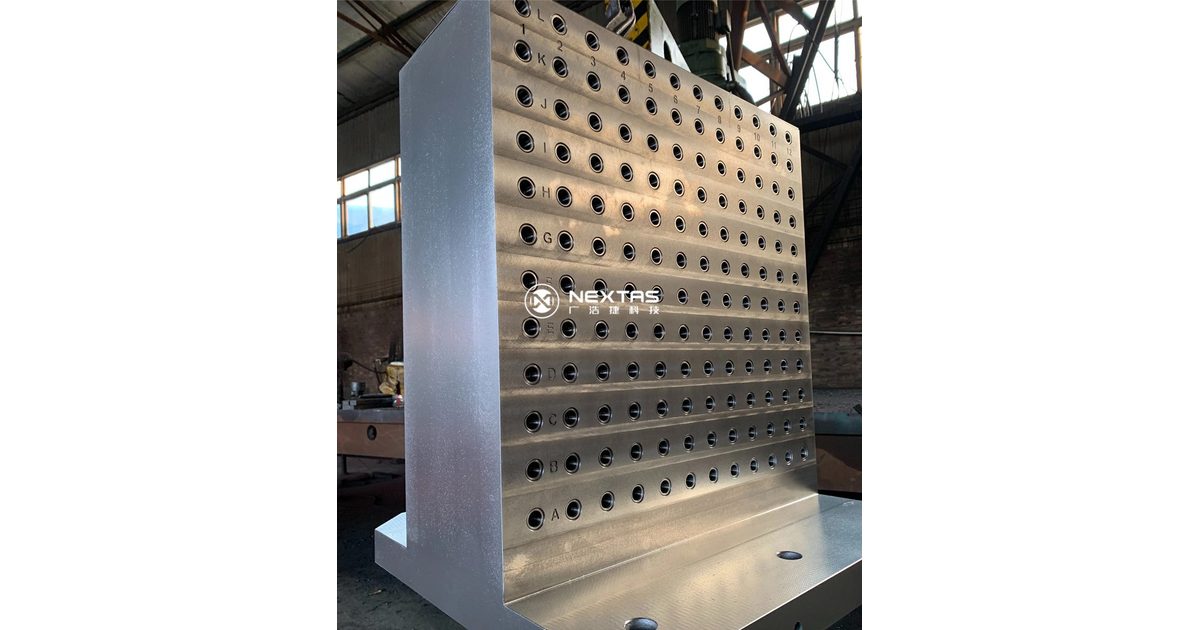
A square column gives four broad sides. A hexagonal or octagonal column gives more sides, but each face has less width for the same overall envelope. More faces can help when the parts are narrow and the tool can reach each station. They can hurt when fixtures, clamps or parts extend into the next face.
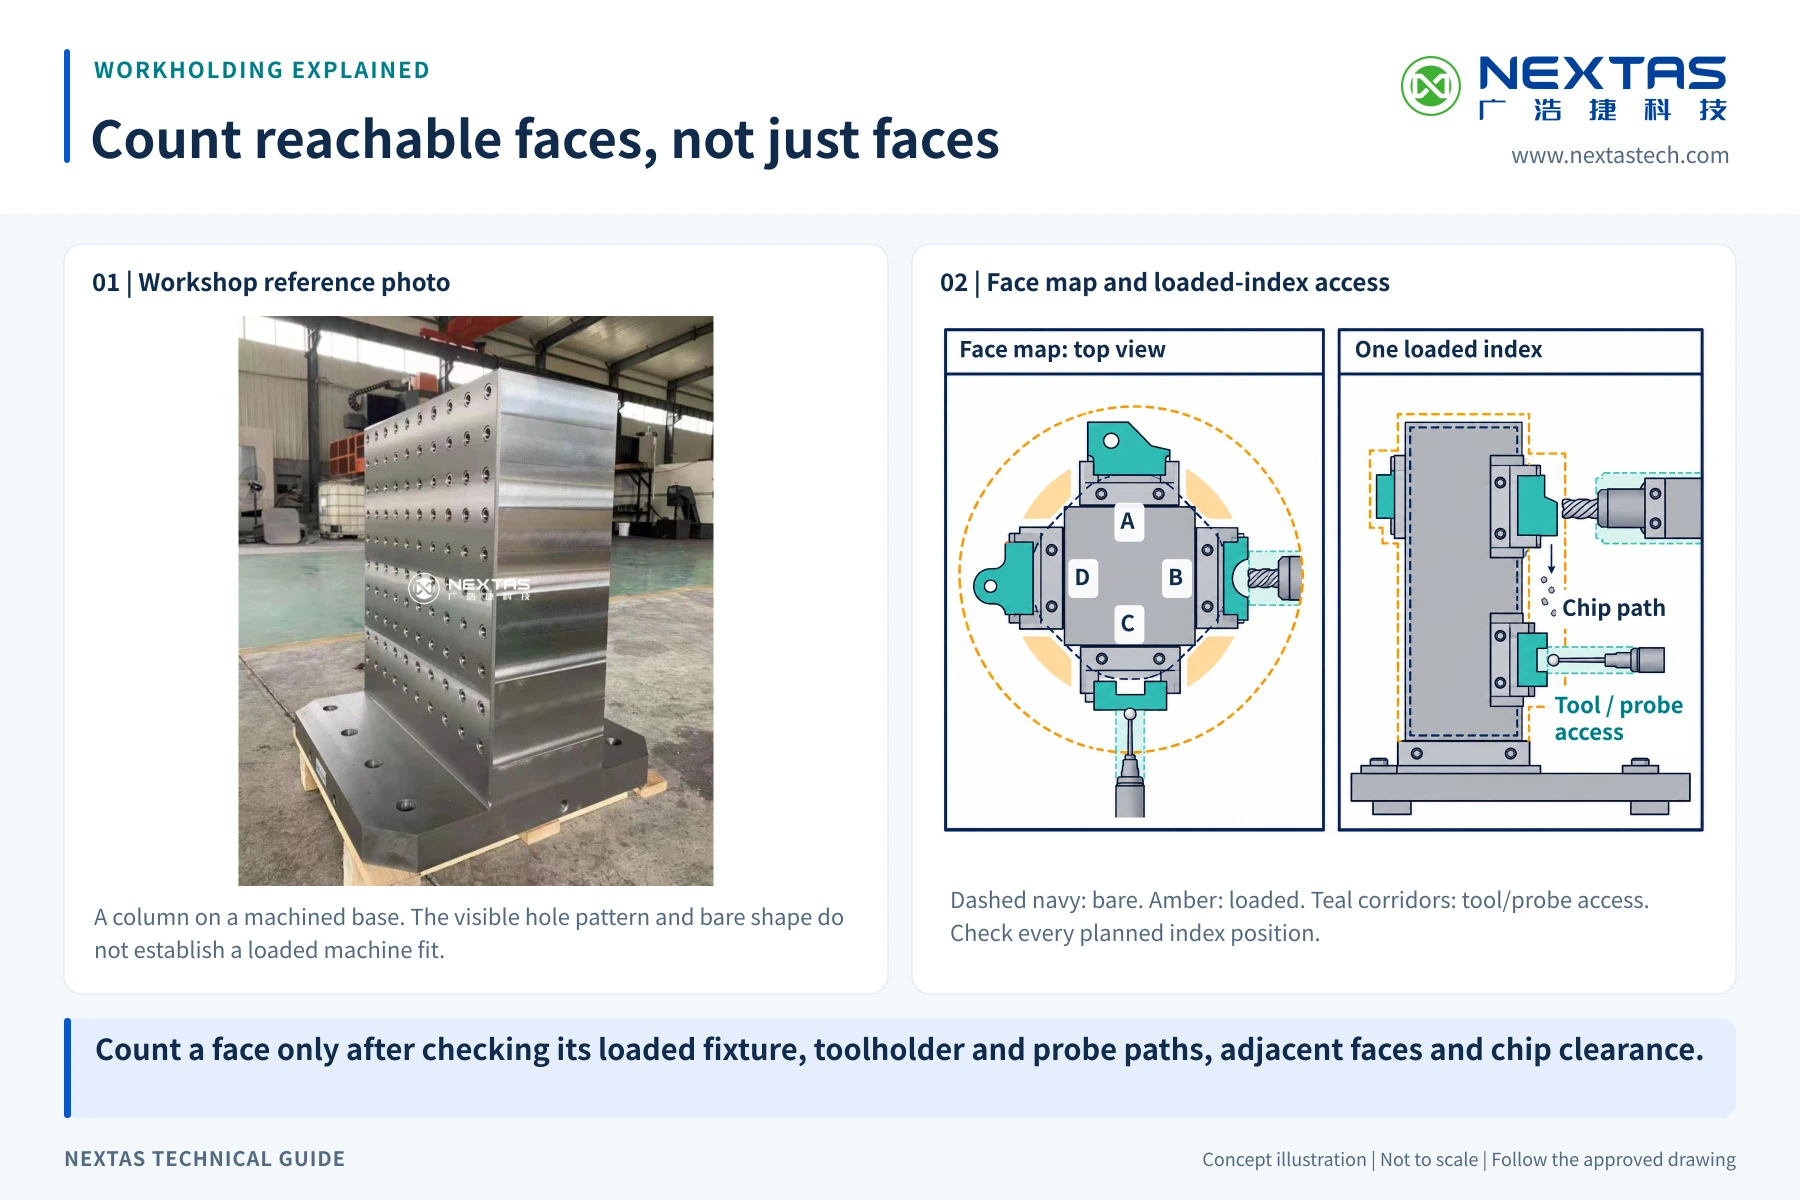
Make a face map before choosing the shape. Put the actual part, fixture, clamp and tool approach on every proposed face. Mark the cutting operation and the datum used on that face. Show where the operator reaches bolts, where chips fall and where a probe must enter. If one face is blocked by the spindle, door or neighbouring fixture, do not count it as usable capacity.
Balance also matters. A heavy fixture on one side can change the loaded centre of gravity. Parts may leave the column at different stages, so the load can change during the cycle. Use the machine builder's rules and review the worst planned condition, not only the fully loaded starting picture.
Use the standard models for a first screen, then confirm on your machine
You do not need a custom column drawing just to start a layout. The seven standard models in the table below already list face width, base, height, nominal workpiece height and weight, so you can shortlist by size first. Check the chosen model against your machine, parts and fixture plan.
The NEXTAS product page lists the seven models below. Width across flats is the distance between opposite faces. “Max workpiece height” is the value listed for that exact model; it is not proof that the part, fixture and tool clear your machine. Weight is the listed bare-column value. Add every ordered adapter and every loaded item before checking the machine limit.
| Exact model | Shape | Across flats | Base | Height | Listed workpiece height | Weight |
|---|---|---|---|---|---|---|
| NT-TCS250P400V2 | Square | 250 mm | 250 mm | 400 mm | 320 mm | 100 kg |
| NT-TCS300P400V2 | Square | 300 mm | 300 mm | 400 mm | 300 mm | 130 kg |
| NT-TCS350P400V2 | Square | 350 mm | 350 mm | 400 mm | 280 mm | 170 kg |
| NT-TCH320P600V2 | Hexagonal | 320 mm | 300 mm | 600 mm | 480 mm | 220 kg |
| NT-TCH400P600V2 | Hexagonal | 400 mm | 350 mm | 600 mm | 450 mm | 290 kg |
| NT-TCO360P600V2 | Octagonal | 360 mm | 350 mm | 600 mm | 450 mm | 285 kg |
| NT-TCO450P600V2 | Octagonal | 450 mm | 400 mm | 600 mm | 420 mm | 360 kg |
Use this table to remove models that are clearly too large, too tall or too heavy. Final selection still needs the chosen drawing, the real machine interface and the loaded envelope. A standard size does not fit every machine.
Specify mounting and locating clearly on each interface
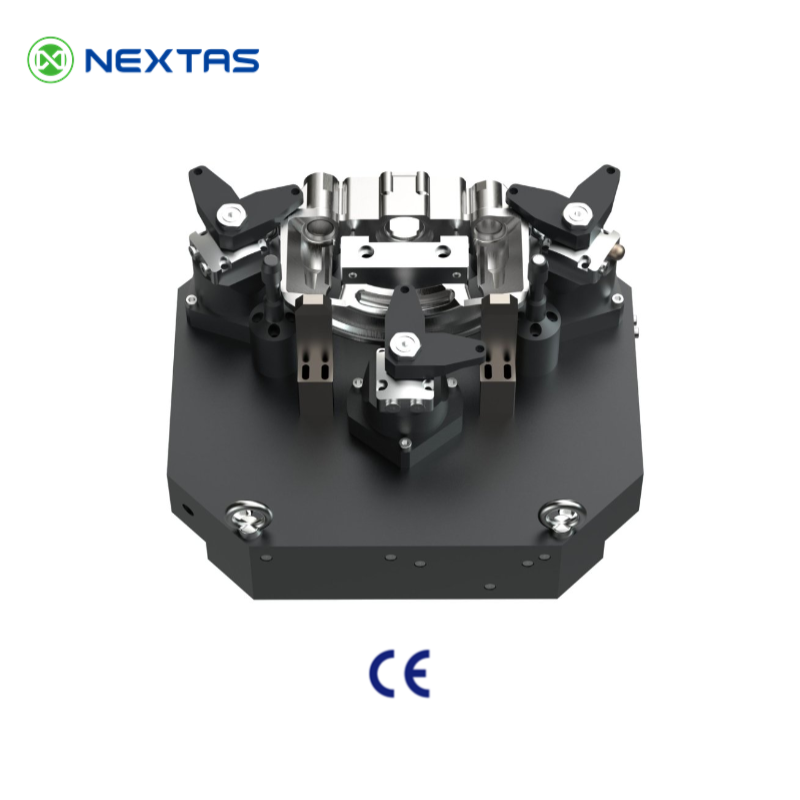
If the base bolts and the face holes are not specified separately, the column may mount to the table while the fixture still will not locate on the face. The column has two interfaces: it mounts to the machine-side base, and the fixtures mount to the column faces. Keep them separate in the drawing set. On each interface, specify both the mounting method and the locating method. For the base, name the bolt size, locating feature, contact surface, orientation and any adapter or zero-point receiver. For each face, name which holes locate, which holes clamp and which holes only provide clearance. When both are clear, it is easier to check fit and to reuse existing clamps or receivers.
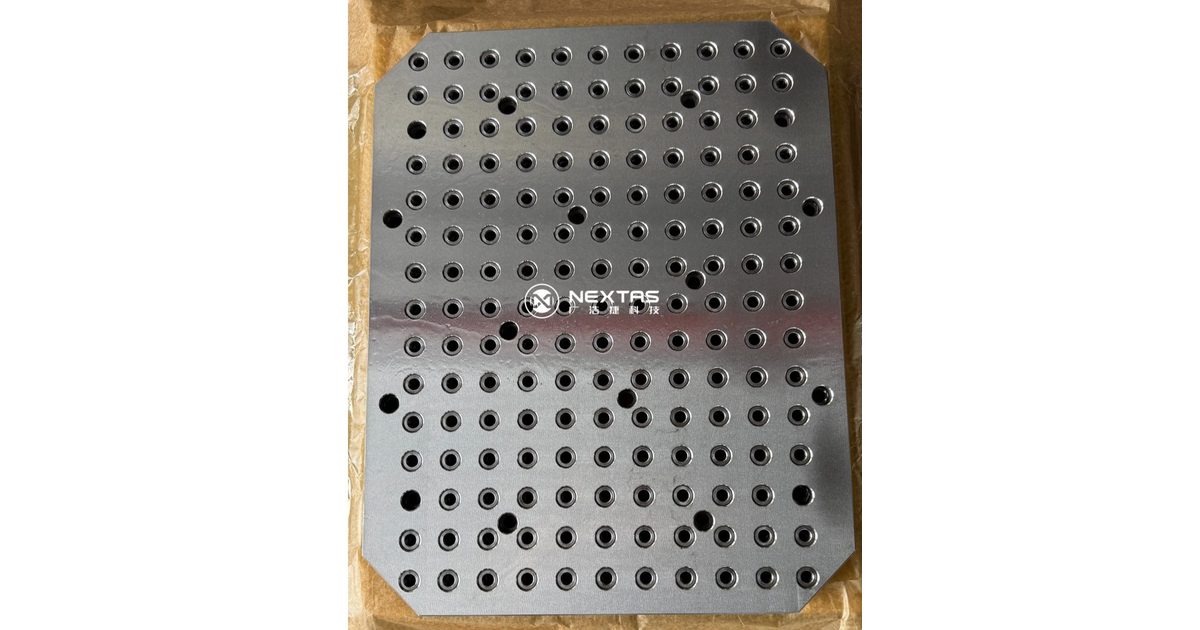
The product range supports plain drilling, precision hole locating and T-slot locating. These are layout choices, not quality grades. Plain drilling can suit a fixed fixture plan. Precision locating holes can provide named reference points. T-slots can allow more movement when fixture positions change. The right choice depends on how the fixture will be installed, removed and checked.
Do not approve an interface from pitch alone. Hole diameter, tolerance, depth, thread, edge distance, dowel relationship and datum reference can all matter. If an existing fixture or zero-point system must be reused, send its drawing or measured interface and ask the supplier to mark the match on an approval drawing.
Build the loaded envelope and load sheet
Column weight is only the first line of the load sheet. Add the base adapter or pallet, receivers, fixture plates, vises, clamps, supports, parts, fasteners, hoses and fittings. State the mass and location of each large item. Show the centre of gravity for the full assembly if the machine builder asks for it.
Now create an envelope for each index position. Include the longest part, the widest clamp and the tallest fixture. Add tool holders, probe stems and the spindle nose. Check the approach and exit path, not just the final cutting position. Also check access for loading, torque tools, chip removal and maintenance.
If the column moves through a pallet changer, include that route. Door, lift and transfer limits may be tighter than the cutting zone. If the column stays on a rotary table, check cables, hoses and nearby guards through the full planned rotation. The site integrator or machine builder must approve the complete motion and load case.
Give every face a job and a datum
A clear face plan makes the quote and acceptance test much easier. Label the faces A, B, C and so on. For each face, list the part number, operation, fixture, datum, clamp direction, tool approach and inspection feature. If two faces carry different jobs, show the worst tool and part envelope for both.
Plan chip and coolant paths as well. A pocket that collects chips near a locating surface needs a cleaning step. A hose or nozzle must not block indexing. A fixture may need a drain path or a cover. These details cannot be proven by the bare column, so include them in the fixture and process review.
See tooling column forms and prepared faces
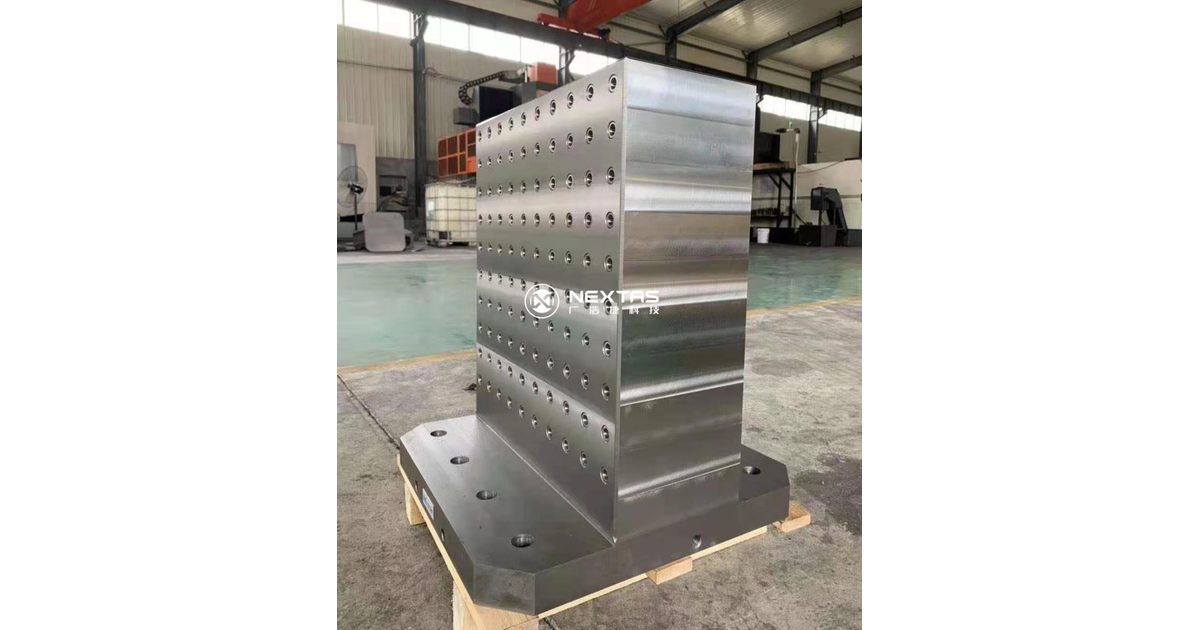
A 30-second vertical workshop view of tooling column bodies and prepared fixture faces.
Watch on YouTube
Separate supplier inspection from machine acceptance
Before production, agree which features the supplier must inspect. Start with the approved general arrangement drawing. Mark the base contact, mounting features, face datums, key hole positions and any fixture-locating features that matter to your process. Put the method, sample scope and acceptance limit next to each item.
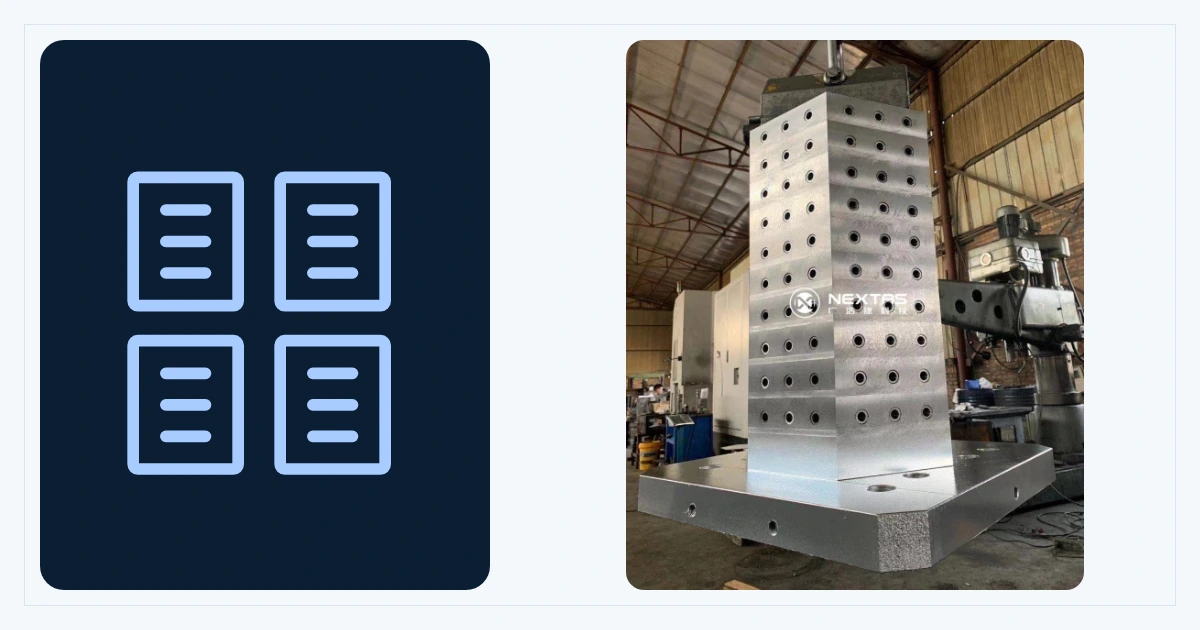
Ask for material or heat-treatment records only when they are part of the order. The NEXTAS product page lists HT250 and QT500 material routes and stress-relief annealing, but a workshop photo cannot show which route was used. The purchase order and traceable record must identify what applies to the delivered item.
Incoming inspection confirms that the received column matches the order. Site acceptance checks the complete loaded system. Mount it on the real pallet or table. Confirm fastener access and the agreed locating method. Move every planned axis and index position at a safe test speed under the machine builder's procedure. Check tool, spindle, probe, fixture, part, door and changer clearance.
Then measure the project datums using the agreed tools and method. If the column is designed to be removed and reseated, include repeated seating in the plan. If parts are loaded on several faces, inspect the features that reveal face-to-face or operation-to-operation error. This page does not supply one tolerance or test count for every machine.
Tell us the machine and the parts you want to hold
The column also has to clear your travels and hold the largest part in the plan. Tell us the machine and the parts you want to run. A table drawing, a part list, or a fixture concept for the largest part will speed up the layout talk if you already have them. Mention any clamps or zero-point receivers you want to keep, and how many faces you have in mind.
Pricing and lead time are set after the scope and quantity are clear.
Questions to ask before you choose the column layout
How many faces should a CNC tooling column have?
Choose by usable faces, not the largest face count. A face is useful only when the part, fixture, tool, spindle and rotary motion all have room. Map the real part family on each face before choosing a four-, six- or eight-sided layout.
What machine data is needed before selecting a tombstone?
Send the machine model, table or pallet drawing, bolt and locating pattern, axis travels, rotary limits, spindle and tool envelope, door and changer limits, permitted load, and any centre-of-gravity rule from the machine builder.
Does a standard NEXTAS tooling column fit every HMC table?
No. A standard model name does not prove table fit. Compare the selected column drawing with the exact table or pallet interface, fasteners, locating features, load limit, axis envelope and changer path before approval.
How should I choose plain drilling, precision holes or T-slots?
Use the fixture plan to choose. Plain drilling supports a fixed hole plan. Precision holes add defined locating points. T-slots allow more fixture movement. The approved drawing must state which features locate, clamp or provide clearance.
What inspection evidence should come with a tooling column?
Put the required evidence in the order. It may include an approved drawing, material or heat-treatment records when ordered, and an inspection report for named base, face, hole and locating features with agreed methods and limits.
What should a tooling column acceptance test cover?
Check the received hardware against the approved drawing, then test the loaded assembly on the real machine. Confirm mounting, axis motion, tool access, fixture clearance, service access and the agreed datum checks. Use project limits; this page does not set a universal pass value.