
Do you measure and align the same insert at every station? Wire electrical discharge machining (EDM) cuts the profile; sinker EDM makes the cavity; a coordinate measuring machine (CMM) checks the part. Measure the alignment and handling required by your current route before planning a transfer system.
For a fictional comparison, assume 45 minutes to two hours (45–120 min) per in-machine alignment. This is an illustrative assumption, not an observed workshop range or NEXTAS time study. Replace it with measured machine downtime, alignment results and uncertainty from your actual process.
A documented part datum is the workflow goal. The part or electrode can remain on its travelling E-Series holder while each station has a fixed mounted chuck. Release each pairing, align the station to its reference artifact, and measure transfer offsets before approving any reduced alignment routine. Matching hardware alone does not remove re-referencing, cleaning, seating checks or first-part acceptance.
The short answer:
Plan a controlled datum-transfer chain from wire EDM to sinker EDM and inspection. Matching ITS-style interfaces are only the hardware starting point. The four listed E-Series bodies reseat closer than 0.003 mm on the selected chuck. That figure is catalogue reseat, not a finished-part tolerance. Prove the chain on your machines before you freeze the route.
What “one datum” means here
A datum is the defined reference used to locate and measure the part. Each machine and CMM has its own coordinate frame. A chuck and holder can provide physical reference features, but they do not align those station frames automatically.
Wire EDM (WEDM) is the wire-cut station. Sinker EDM is the cavity-burn station. The CMM is the inspection station. A common part datum requires a released chuck–holder pairing at each station, documented alignment to a reference artifact, and measured transfer offsets with agreed uncertainty and acceptance limits. The same family and holder alone do not preserve one physical coordinate origin.
E-Series and R-Series use different interface families. They are not direct substitutes. A released cross-interface transfer chain can still define a common part datum if the additional interface, alignment and transfer measurements are qualified. Family names alone do not decide that result. The ITS-50 tooling guide covers EROWA-style holders; the System 3R-style chuck guide covers the other family.
The E-Series product page is the catalogue source for the numbers in this article. ITS 50 / ER-036345-style fit is a drawing check, not a family-name promise.
Which body sits on which machine?
The family name is not the layout. Four listed bodies share the same ITS-style idea. They do not share the same outline.
Values below come from the current E-Series catalogue page. Confirm the selected model drawing before you freeze tank clearance or air.
| Code | Listed body | Mass | Candidate mounting context |
|---|---|---|---|
| NT-S100P100V1 | Model 100 pneumatic | 5.3 kg | Flat mill, sinker table, CMM plate |
| NT-S100P100V2 | Side vertical | 7.1 kg | Side plate, rotary, or wire rail |
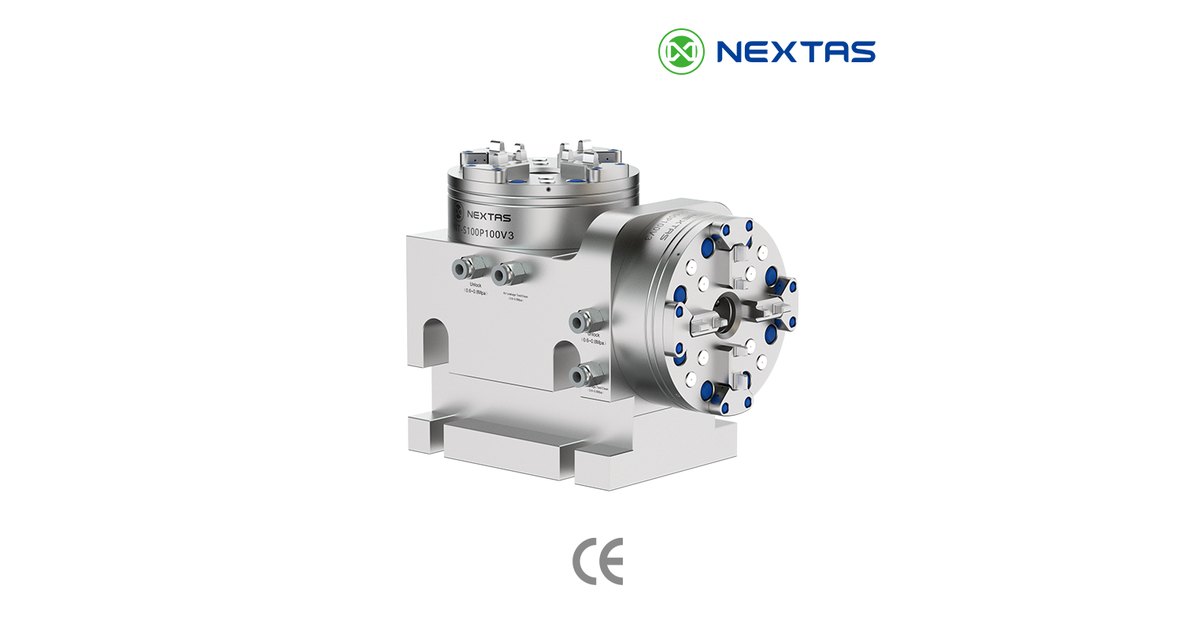
| NT-S100P100V3 | Right angle | 17.7 kg | Right-angle mounting; verify overhang, support and approved moment/load limits |
| NT-S100P80V1 | EDM pneumatic | 2.0 kg | Tight EDM space |
All four list reseat closer than 0.003 mm. V1, V2, and V3 list more than 6,000 N clamp. P80 lists 4,000 N and a 15 kg clamping load. That 15 kg figure is not a robot payload or a cutting-load rating.
The catalogue lists 0.5 to 0.8 MPa to open the pneumatic chuck; confirm the selected released drawing and circuit. The chuck tables cite spigot NT-S200P55V2, while the accessory table uses NT-S100P55V2. Confirm the ordered code, geometry, holder pairing and chuck revision against the approved drawing before order release.

V3 is the listed right-angle body with a mass of 17.7 kg. Its outline alone does not approve an overhung job. Check the selected chuck and holder drawings, support contacts, friction/retention limits, combined loads and moments, machine mounting and wire-guide clearance before choosing this layout.
Wire water, sinker oil, and a clean CMM
The part and holder travel between wire EDM, sinker EDM and inspection. Each station’s fixed chuck remains on its released mount. Check the actual exposure and cleaning procedure for each chuck and the travelling holder separately.
Wire EDM. The chuck can sit in deionized water. Unprotected steel pits. The listed E-Series bodies use hardened stainless steel. Still wipe the seat. Water plus sludge will hide a chip.

Sinker EDM. The threat is graphite dust and oil. A flake on a Z pad cocks the holder. Where the selected model has an air blast, use it as one clean step. Then look. Then wipe. Air alone does not prove a clean seat.

CMM room. Clean and dry the holder using the approved procedure for the selected assembly. Preserve the qualified part-to-holder setup where that procedure permits. Any unclamping, cleaning or remounting that can change the datum chain requires the specified remeasurement before transfer.
How do the numbers get to the machine?
The holder can repeat relative to its fixed, mounted chuck within the selected component’s specified test conditions. The chuck must be aligned to each station’s coordinate frame. Measure the part reference through the released CMM routine and document the transfer offsets and their uncertainty before applying them at a cutting station.
An illustrative sequence, subject to the released station references, looks like this:
- Mount the blank or electrode on the holder at a bench, not in the tank.
- Clamp the holder in a matching chuck on the CMM.
- Probe the features against the chuck centre. Record shift in X, Y, and Z, plus rotation if you need it.
- Send those numbers to the wire or sinker control. Where the selected control supports it, an RFID (radio-frequency identification) tag may identify a holder or carry supported data. Other approved methods transfer a program file or use manual G54 entry. Verify the correct holder, units, coordinate transform and offset values for every method; manual entry needs an independent check.
- Clamp on the machine. Load the offsets. Close the tank. Start the burn.
Optional holder-identification tags and program-file transfer are cell-specific integration methods, not catalogue functions promised for these chucks. Confirm the actual tag, reader, data format and control support with the integrator before using them.
A small catalogue reseat value does not remove station alignment or prove that the remaining transfer offset is small. Establish reference artifacts, station transforms and transfer measurements under the agreed method. The reseat guide explains the scope of <0.003 mm.
Seat check and air-loss hold
Unattended burns fail when the holder is not down, or when air is lost and nobody knows.
On the listed pneumatic models, shop air at 0.5 to 0.8 MPa opens the chuck. When air vents, springs pull the drawbar. That hold is a process hold. It is not a safety-rated stop unless the full cell safety design says so.
Some circuits also watch the seat with a small air port on the Z pad. If the holder is flat, pressure builds. If a chip lifts the face, air leaks and the switch stays open. That signal can block Cycle Start. It is a process check, not a safety function.
Do not treat a green light as proof the job is safe to run with nobody in the bay. Guarding, stop logic, and recovery still belong to the cell builder.
Where the hours go
Measure the buyer’s current baseline: machining, alignment, handling, cleaning, inspection and waiting. Use the actual downtime split to decide which steps a qualified transfer workflow could reduce.
This is a fictional planning scenario, not a customer case or observed workshop range. If a wire machine waits 90 minutes a day for indicate, and you run 220 days, that is 330 hours a year of tank time with no burn. Cost that at your shop rate. Compare it with chucks, holders, and a CMM program. Do not use a catalogue reseat number as a payback claim.
The times below are fictional planning assumptions, not observed shop ranges or NEXTAS test data. Compare them with measured baseline and pilot results.
| Item | Measured in-tank alignment | One E-Series holder |
|---|---|---|
| Time in the machine | Fictional assumption: 45–120 min | Measured exchange plus cleaning, seating/lock checks, released offsets and first-part acceptance |
| Who holds the origin | Measured part reference after station alignment | Qualified part–holder references, station alignment and measured transfer offsets |
| How offsets enter | Typed | File, chip, or typed — pick one and lock it |
| Night running | Operator required for any manual alignment and exchange | Only after full-cell guarding, seating/lock, air, faults and restart acceptance |
Measure the complete released workflow after factory and site acceptance, including cleaning, seating and lock confirmation, datum checks and first-part inspection.
How to roll it out
Do not bolt a chuck into a tank and hope.
Fit and clearance. Weigh the job. Check wire guides, tank rims, and travel. Decide V1, V2, V3, or P80 from that envelope, not from a family name.
Mount and air. Use a ground plate. Clock the chuck to the machine axes. Keep total indicator runout under 0.002 mm if that is your install spec. Plumb dry air at 0.5 to 0.8 MPa with a filter at the chuck.
Prove reseat and transfer. Treat NT-S200P55V2 as the chuck-table candidate; resolve the NT-S100P55V2 accessory-code discrepancy through the approved geometry and revision. Clamp, measure, release, clean and reload a qualified reference artifact on each station. A count of 10 to 20 repetitions is an illustrative planning example, not a sufficient universal protocol. Agree the count, load, temperature, measurement uncertainty and acceptance criteria. Record station alignment and transfers across wire EDM, sinker EDM and CMM. Use <0.003 mm as the component catalogue comparison unless a separate installed limit is agreed.
CMM program. Release the reference artifact, station alignment and part-datum routine. Document how offsets and coordinate transforms move between systems and verify the transferred values before the machining cycle.
Inspection and service. Follow the selected model’s cleaning, seal inspection and service instructions. Define the drawbar-force measurement method, load condition and acceptance limit; set inspection and replacement intervals from those instructions and actual use. Neither a calendar nor an air blast alone proves acceptable seating or retention.
What to send for an E-Series review
NEXTAS can review the chuck body, holder family, and open stack questions. We cannot sign off a CMM program, a robot safety plan, or a tank rebuild from this page.
- Machines: models for wire, sinker, mill, and CMM. Write “unknown” if a field is open.
- Holders: photos of current chucks and holders, plus any drawing.
- Job: part or electrode size, mass, and how far it hangs past the seat.
- Fluid: water, oil, or both.
- Target: the reseat limit you will measure, and the method.
- Air: pressure you can hold at the chuck, not only at the compressor.
- Family: whether you already run ITS-style or System 3R-style holders.
Ask for the body, matching holders, and the open questions. The process owner still has to prove dirt, probes, and first-part checks on the mix.
NEXTAS is an independent supplier and is not affiliated with, endorsed by, or sponsored by EROWA or System 3R. Those names, ITS 50 and ER-036345 appear here only to identify the holder family a buyer may already run.
Questions before you freeze the WEDM-to-CMM route
Does <0.003 mm mean the finished part will match the CMM?
No. That figure is catalogue reseat on the listed chuck. Finished-part transfer also depends on the holder, the mount, dirt, temperature, and the probe plan. Prove the full chain on the agreed test.
Can I mix E-Series with a System 3R-style chuck on one job?
The families are not directly interchangeable. A common part datum may still be defined through a released cross-interface transfer chain with an additional checked interface. Qualify the actual pairing, station alignment, reference artifact and measured offsets with agreed uncertainty and acceptance limits. A shared family name alone does not provide this proof.
Is the air-seat check a safety stop?
No. It is a process check that can block Cycle Start when the holder is not down. It is not a safety-rated function unless the full cell safety design says so.
Which body should I shortlist first?
Start with tank clearance, total assembly mass, support contacts and the selected model’s approved load and moment limits. V1 is the flat-table body; V2 is the side body; V3 is the right-angle body; P80 is the compact EDM body with a lower listed clamp force. Send the assembly and machine-envelope drawings. Photos aid identification but do not approve fit or load.
What can NEXTAS review from this page?
The chuck body, holder family, and open stack questions. Send the brief above. Your integrator and control vendor still qualify offset transfer and any holder-identification tag or reader. The cell builder still owns guarding and recovery.
WEDM to CMM review
Send machine models, holder photos, and tank clearance
Send the brief above and name V1, V2, V3, or P80 if you already lean one way. NEXTAS can review the chuck, holders, and open questions for your quotation.
Discuss your E-Series route