00:00 Out · 00:12 Right bay · 00:30 Left fetch · 00:58 Seat/lock
Walk onto any shop floor running a bridge or gantry milling center, and you will quickly spot the paradox of large-part machining: the most expensive spindle in the building often spends the most time standing still.
When machining large structural plates, precision machine frames, or multi-cavity mold bases, the cutting cycle itself is rarely the bottleneck. The real profit leak happens between cycles. Once the gantry spindle stops, operators have to wait for an overhead bridge crane, unbolt heavy toe clamps, rigging-lift the finished plate out of the deep enclosure, sweep chips off the massive T-slot table, load the next raw blank, and spend 30 to 45 minutes indicating the X-axis and probing work offsets. During a standard eight-hour shift, traditional on-machine setup leaves a high-horsepower gantry mill cutting metal for barely 4 to 4.5 hours.
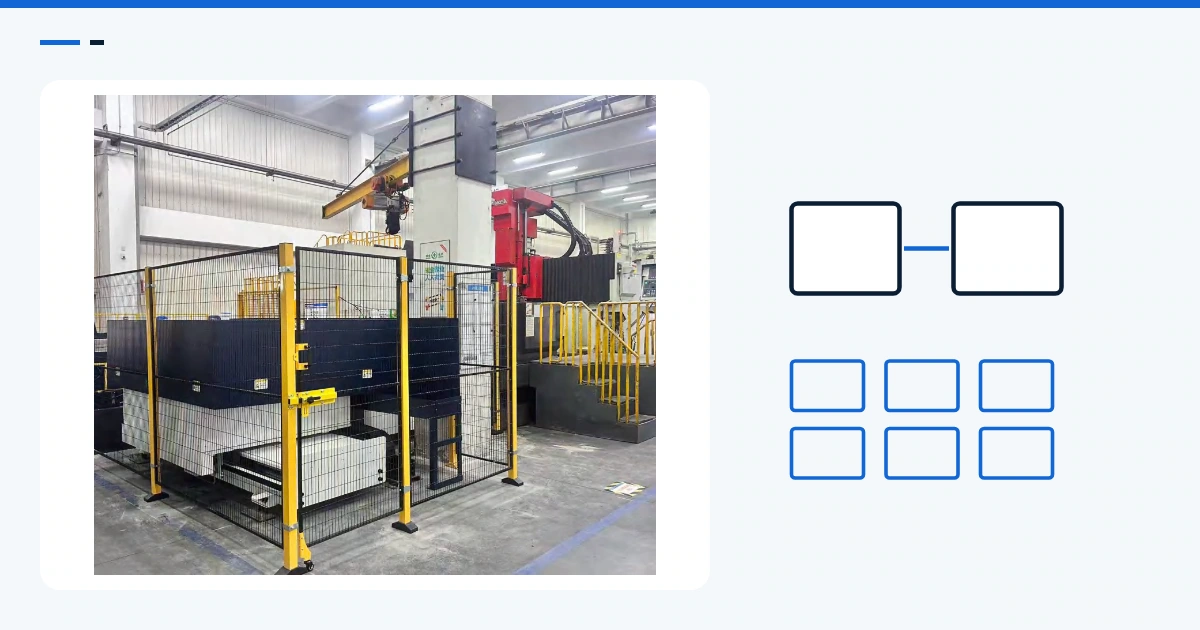
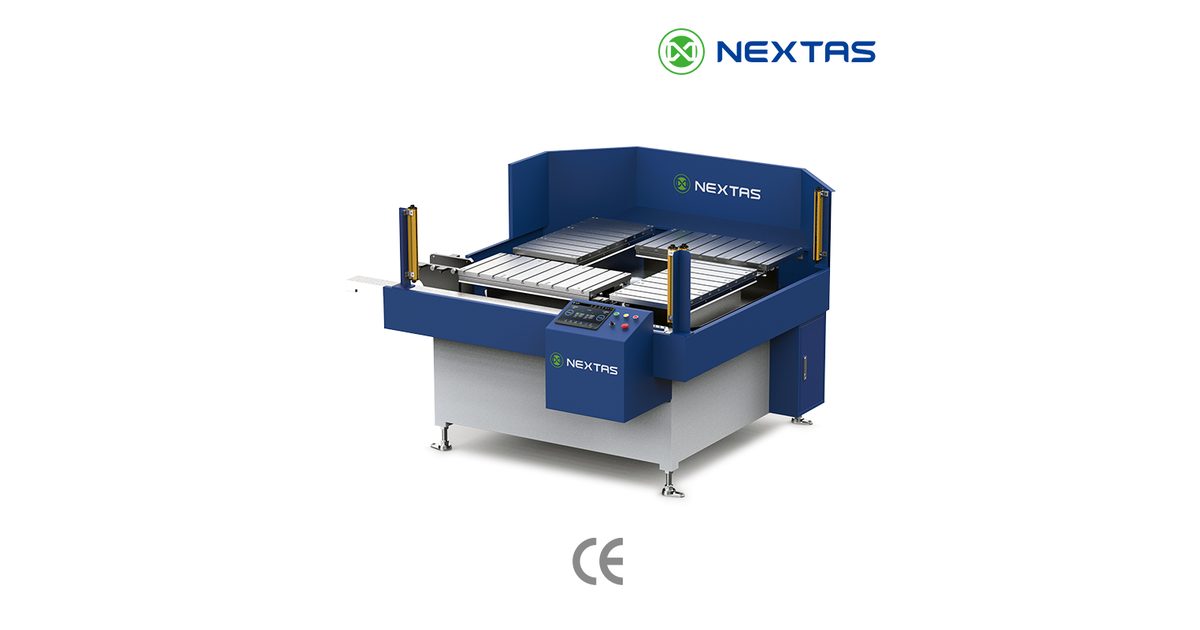
To reclaim those lost spindle hours without investing in a second bridge mill, the customer partnered with NEXTAS to integrate a heavy-duty Dual-Station Front-Loading Automatic Pallet Changer (APC) directly in front of its CNC gantry machining center.
Anatomy of a Gantry Pallet Swap
As captured on the customer’s shop floor, the NEXTAS APC transforms what used to be a two-person crane rigging ordeal into a hands-free mechanical swap. The clip is played fast; the swap itself takes about three minutes.
- 00:00 – 00:12 | Automated Door Opening & Unloading (Station 1 Out): The moment the gantry mill finishes decking a large metallic plate on Pallet #1, the NEXTAS automated vertical safety door opens upward. The central longitudinal transfer shuttle reaches inside the machine envelope, unlocks the table’s V4 Positioning Datum receivers, and glides the finished pallet smoothly out onto the central bridge track.
- 00:12 – 00:30 | Lateral Transfer to the Right Staging Bay: Once clear of the gantry columns, the shuttle indexes Pallet #1 laterally into the right-hand staging bay. The finished plate is now parked safely outside the machining zone, ready for offline unloading.
- 00:30 – 00:58 | Fetching the Pre-Staged Workpiece (Station 2 In): While the gantry mill was cutting Pallet #1, the operator had already used the offline left-hand staging bay to clamp and pre-stage Pallet #2—loaded with a heavy ribbed structural component. The transfer mechanism shifts left, engages Pallet #2, and indexes it laterally onto the central longitudinal rail.
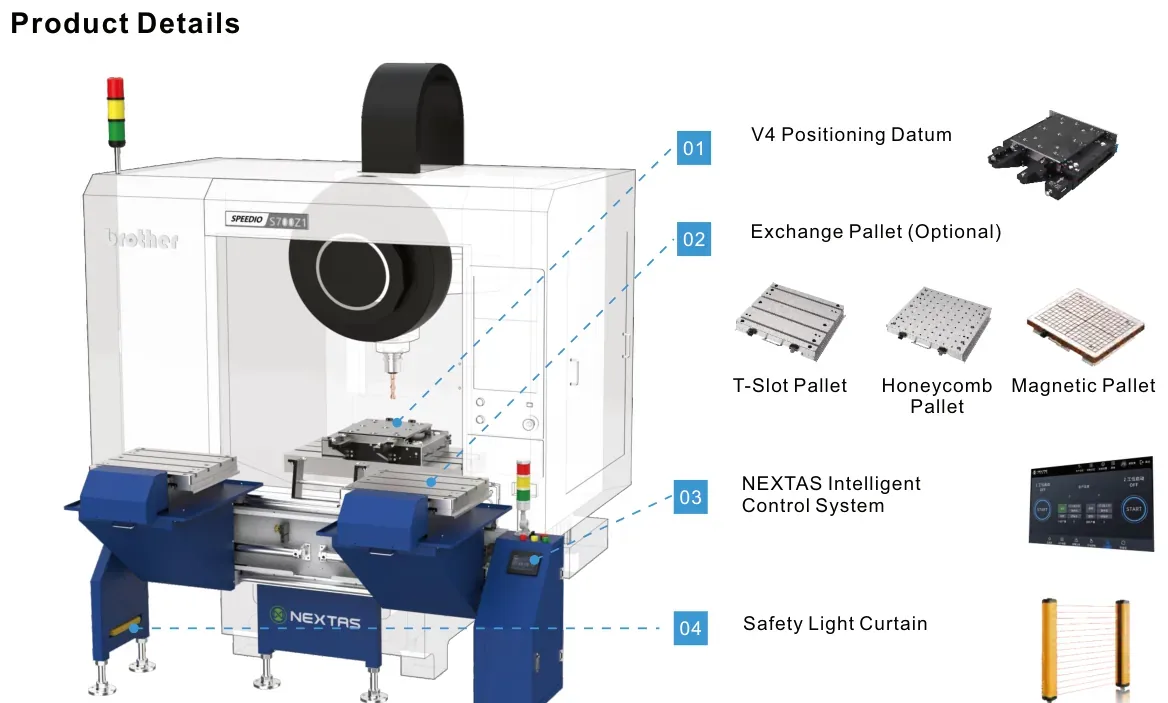
- 00:58 – 01:28 | Machine Seating, Datum Blow-Off & Cycle Start: The central shuttle drives Pallet #2 straight through the open enclosure door onto the gantry table. As the pallet lowers onto the hardened martensitic stainless steel V4 zero-point receivers (engineered with up to 1,350 kg of automatic lifting capacity), integrated X/Y/Z air-jet ports blast away residual coolant and swarf. An internal Z-axis air-seal detection circuit verifies flush seating and sends a confirmation signal directly to the machine’s CNC servo system. About three minutes after the previous cut ending, the vertical door closes and the spindle is back in the cut.
Engineering Highlights: Built for Heavy-Duty Gantry Envelopes
Retrofitting automation onto a gantry mill requires far more structural rigidity and chip-management intelligence than a compact vertical machining center:
- T-Shaped Shuttle Architecture for Narrow Floor Aisles: Rather than using a massive rotary swing arm that consumes wide floor space and struggles with heavy cantilevered loads, NEXTAS engineered a rigid T-layout combining a central linear transfer beam with flanking left/right staging bays. Enclosed within high-visibility yellow safety fencing and guarded by safety light curtains, the operator can safely load or crane-lift parts at one station while the shuttle operates.
- V4 Positioning Datum with Real-Time Air-Seal Verification: Inside the gantry enclosure, heavy cast-iron or aluminum chips can easily ruin Z-axis flatness if trapped under a pallet. The NEXTAS V4 positioning system—manufactured from imported martensitic stainless steel—combines automatic X/Y/Z air-jet cleaning with Z-axis air-tightness seat verification. If a stray chip prevents the pallet from seating within < 0.003 mm to < 0.005 mm repeat positioning accuracy, the NEXTAS Intelligent Control System halts the cycle before the tool ever touches the part.
- Closed-Loop CNC & OEE Integration: Mounted outside the safety perimeter, the NEXTAS touchscreen HMI console gives operators one-touch control over station queuing, manual overrides, and automated mode selection. Behind the scenes, the platform monitors real-time operational parameters, provides fault pre-alarms, and calculates live Overall Equipment Effectiveness (OEE).
By the Numbers: Traditional Gantry Setup vs. NEXTAS Dual-Station APC
| Operational Metric | Traditional On-Table Gantry Setup | NEXTAS Dual-Station APC System | Shop-Floor Impact |
|---|---|---|---|
| Workpiece Changeover Time | 15 - 45 min (crane + manual clamping) | about 3 min (clip is played fast) | 15–45 min changeovers cut to about 3 min |
| Changeover Setup & Indicating | 2 - 4 hours (dialing in & probing) | 10 - 20 min (offline pallet prep) | 85% - 90% faster job changeovers |
| Effective Cutting Time / Shift | 4 - 4.5 hours | 7 - 7.5 hours | +50% to +80% spindle utilization |
| Overall Machine Utilization | < 50% | 50% - 90%+ | 60% to 200% capacity multiplication |
| Datum Repeatability & Safety | Manual indicator sweep (± 0.02 mm) | < 0.005 mm + Z-axis air-seal check | Payback achieved in 6–18 months |