Should a 1–3 machine shop buy a two-pallet changer, or a rack of extra pallets? The machine price is not the whole buy. The extra pallets, tools, and fixtures often decide whether the spindle keeps cutting after people leave.
A two-pallet automatic pallet changer (APC) swaps one pallet in the machine with one pallet outside. A multi-pallet pool stores more pallets in a rack. A lift or robot feeds the machine from that rack.
This guide helps a shop owner or production engineer pick a first layout. Measure your cycle time and mix. Then send that pack for a workholding review.
The short answer:
Compare a two-pallet changer if one staged job covers the measured loading gap. Compare a pool if the actual mix needs more queued jobs. Count tools and fixtures as well as pallets. Night operation also requires acceptance of the complete cell, fault response and restart plan.
What does a two-pallet changer actually do?
On a two-pallet APC, Pallet A is in the machine and cutting. Pallet B sits at a load station outside. You unload, clean, and clamp the next job on Pallet B while Pallet A runs. When the program ends, the pallets swap. The spindle does not wait for you to open the door and pick parts off the table.
Measure the actual pallet-exchange and loading times separately. If loading the spare pallet takes longer than the current cut, that delay adds spindle waiting. If Pallet A cuts for 18 minutes, you have 18 minutes to finish Pallet B. If you are late, the spindle waits. If you leave for the night, the machine can cut the one pallet you staged. Then it stops.
That is still a big gain over a manual vertical mill, where the spindle sits while you load in the enclosure. A two-pallet machine can keep cutting through the day shift. It does not, by itself, give you a full night of lights-out work.

The NEXTAS pallet changer page covers manual and automatic layouts. Use it to talk about pallet size, payload, and the load station. It does not pick a two-pallet shuttle versus a rack for you. Your cycle time does that.
If the open question is still “manual table versus APC,” stop here and read the manual pallet changer guide first. This article starts after that fork. It compares two automatic buffers on one to three machines.
The night buffer is one pallet, not a shift
A rotary 6-pallet pool and a stacked rack with 10, 12, 16 or more pallets are different project layouts. Both can store jobs for later loading. Their staged cycle time is only a queue estimate. Before unattended use, accept the complete machine/cell: guarding, load retention, tool life, chips, inspection, fault response, safe states and authorized restart.
The hardware difference is simple. Two-pallet: one spare cycle. Pool: many spare cycles. If each pallet cuts 15 minutes, one spare pallet dies 15 minutes after the last person leaves. Eight staged pallets are two hours. Sixteen staged pallets are four hours, not a full night. Compare cut time times staged count to the hours you actually want after close. Tools, chips, and probes can stop the queue sooner.
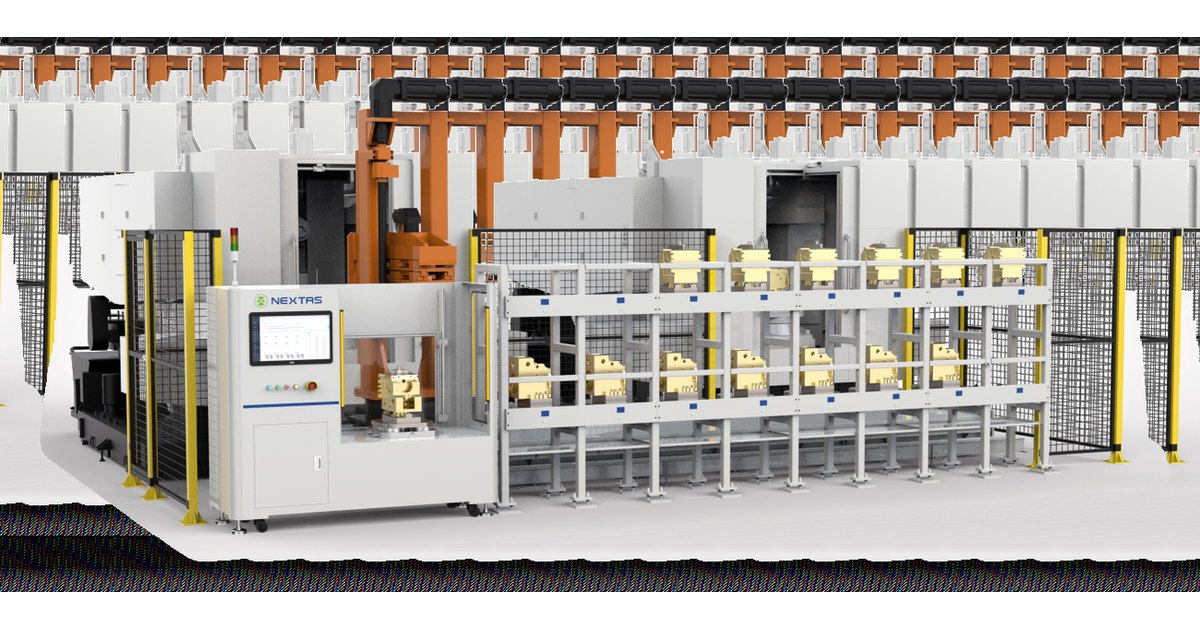
A rail-guided cell is a larger cousin of a single-machine pool: pallets travel on a floor rail between machines. A linear flexible manufacturing system (FMS) is that kind of cell. For a 1–3 machine shop, start with one machine and a rotary or stacked pool if the delay is pallet wait. Do not treat a rotary 6-pallet and a stacked rack as the same kit.
Planning ranges only. Your mix, cut time, and alarms set the real buffer. These rows are not NEXTAS test results.
| Layout | Stored pallets | Night buffer | Who must stay nearby |
|---|---|---|---|
| Two-pallet APC | 2 | One extra job | Operator to reload the free pallet for the next cycle |
| Small rotary or rack pool | 6 to 12 | Several extra jobs | Day staging, then alarms |
| Larger pool or rail cell | 12 to 24+ | A long queued run | Staffing depends on the accepted complete cell, guarding, fault response and restart plan. Remote alarms alone do not authorize unattended operation. |
For a hypothetical time study, 25% to 50% cutting time can be used to test the cost calculation. These are invented scenario inputs, not measured shop ranges or NEXTAS results. Measure this machine’s cutting and waiting by cause. A changer or pool improves output only if it removes the recorded bottleneck and the tools, fixtures and accepted cell can support the added run.
Study a shared FMS only when jobs, pallets, or tools wait across more than one machine. The FMS readiness test covers that larger fork.
Why tools and fixtures can stop the cell first
A frequent miss is to budget the rack and forget the tool magazine and the fixtures. The pool can deliver a pallet. The spindle still stops if the next cutter is missing, or if the pallet has no fixture on it.
Build the magazine count from the actual tool list. A hypothetical 40 to 80 pockets for one part family is not an equipment requirement. Include shared tools, job-specific tools, sister tools and restrictions for tool size or adjacent empty pockets. For each queued job, check remaining tool life and the accepted response when a tool wears or breaks.
First-pass pocket counts, not a catalog law:
- Two-pallet APC: hypothetical 40 to 80 pockets. Replace this with the actual main tools, backups and blocked-pocket count.
- Six-pallet pool: 120 pockets is an illustrative planning count, not a minimum. Determine the required capacity from the actual tool list, job mix, sister tools and magazine restrictions.
- 12-pallet pool: 240 pockets is a hypothetical example, not a minimum. Count the real inventory, sister tools and blocked pockets, then obtain the builder’s magazine options.
Every stored pallet also needs workholding. A blank station in the rack is idle capital. A 400 mm or 500 mm tombstone with vises is a large line item if you buy a dedicated fixture for every pallet. Many mixed shops instead put a zero-point plate on each pallet face. Then vises, dovetail blocks, and nests can move onto any pallet without a new tombstone for every part number.

Listed NEXTAS pneumatic plates use 52 mm or 96 mm pull-stud spacing. The release-supply reference around 6 bar is retained from earlier guidance and has not been independently verified as a catalog pressure rating. Confirm the required pressure, pressure at the plate and release circuit on the selected-model drawing. The catalogue describes mechanical self-locking with pneumatic release. Confirm the selected drawing, mechanical retention and air-loss behavior on the actual circuit; this mechanism alone does not prove a safe cell state. The listed models publish a clamping-force range of 9,000 N to 40,000 N. That catalog figure is not the same as pull-in or locking force. Use the selected model's datasheet. Do not copy the top number onto a small plate. See the pneumatic zero-point plate page and the automation quick-change guide for the interface, not for a pallet-rack quote.
NEXTAS does not set the machine tool’s magazine price or the original equipment manufacturer (OEM) rack price. Get those quotes from the machine builder. Then add fixture stations and zero-point plates so the comparison is honest.
Can the control skip a bad pallet?
The builder’s approved control sequence decides how pallets exchange and which guard and machine states must be checked. Review the response to an empty pallet, tool fault, failed docking and loss of clamp confirmation. A machine that waits safely at a fault may need an authorized person before it can restart.
A pool needs more than a swap code. Cell software has to know which pallet is loaded, which program is approved, and which cutters still have life. If Pallet 4 needs a spent tool and no sister tool is in the magazine, the cell should store that pallet and call Pallet 5. It should also tell the day shift what failed.
That logic belongs to the machine or automation vendor. NEXTAS does not supply OEM cell controllers and is not affiliated with those brands. Ask the machine builder who owns tool-life data, pallet IDs, and fault routing. A zero-point clamp signal is a process check. It is not a safety-rated function unless the full safety design says so.
Before a weekend run, walk a short list:
- Does each queued pallet have stock, a proven program, and a known fixture ID?
- Do remaining tool minutes cover the queue, including sister tools?
- What happens on a broken tool: abort the feature, return the pallet, start the next good job?
- Who may reset an alarm, and from where?
If those answers are missing, a 16-pallet rack still stops at the first fault. Hardware cannot skip a job the software cannot identify.
Quote the extra kit, not a brochure hour claim
Do not start with a brochure utilization number. Compare the extra kit you must quote: fixtures, magazine size, rotary or stacked pool hardware, and cell software. The table below names those lines. It is not a customer case and not a NEXTAS price list.
Planning comparison only. The cells name kit lines and what extra cash buys.
| Quote line | Two-pallet example | 12-pallet example |
|---|---|---|
| Night buffer | One staged pallet | Queued rotary or rack, if tools last |
| Extra kit to quote | Two fixtures, standard magazine | Rack, large magazine, 12 stations, cell software |
| What the extra cash buys | No in-machine loading on the day shift | A longer unattended queue |
Use the night-buffer math in the rack section: cut time times staged pallets. Write chip, probe, and tool limits next to that count. Do not convert the count into annual revenue until you have a quoted kit and a time study.
If a pool still looks cheaper than a second machine plus a second shift, keep going. If the extra fixtures and 240-pocket magazine already exceed a second two-pallet machine, stop and compare that path with the same time study. The standalone automation guide helps when the first cell is one machine, not a plant-wide FMS.
Floor space: one stacked rack vs three machines

Compare the project footprints first. Three two-pallet machines need three machine, chip and load zones; a rotary 6-pallet pool and a stacked 12- to 16-pallet rack have different footprints. Include guarding, service access, forklifts and the load station on each drawing. Then compare capacity separately: one pooled spindle does not become three spindles because its rack is tall.
Equal hours are not automatic. Three machines can cut three different materials at once. One pooled machine cuts one program at a time. If your bottleneck is spindle waiting on one stable family, a rack on that machine can beat a second unused mill. If your bottleneck is three unrelated processes, a rack will not merge them.
Measure waiting by machine and by cause. Then compare square metres. Do not use a brochure footprint as a plant layout.
Which layout fits your shop?
Start with average cut time on a pallet face. Then look at batch size and whether a skilled setter is hard to hire.
Lean toward a two-pallet APC when:
- A pallet face cuts 45 to 120 minutes or more. One person can load the spare pallet during that cut.
- You run repeating batches on two dedicated fixtures. You do not need 12 different setups parked in a rack.
If cash is tight, still ask the builder to leave a later pool interface open. Do not assume a retrofit is cheap.
Lean toward a multi-pallet pool when:
- Jobs are 1 to 20 pieces and setups currently tear down on the table. Dedicated pallets in a rack skip that tear-down.
- A pallet finishes in 5 to 25 minutes. One spare pallet dies soon after close. Multiply cut time by staged pallet count and match that to the night you want. At 5 minutes, 18 pallets are about 1.5 hours. At 25 minutes, 18 pallets are about 7.5 hours.
- You cannot staff a second shift, but you can staff one daytime setter who loads the rack.
If the next step is linking two or three machines on one job list, you have left the two-pallet fork. Use the FMS readiness test and the NEXTAS FMS product page for software scope. Those pages do not replace the machine builder’s cell controller.
Send cycle time, mix, and fixture photos
NEXTAS can review the workholding side: pallet faces, zero-point plates, vises, and how jobs move off the table. We cannot approve an OEM rack, magazine, or cell program from this article. Send this brief so a quote talks about the same machine.
- Machines: count, model, table or pallet size, and current magazine size. Write “unknown” if a field is open.
- Time: cut time per pallet face for the top 20 jobs. Note waiting by cause: load, setup, tools, chips, inspection.
- Mix: active part numbers, batch size, and whether fixtures can stay built on pallets.
- Night goal: hours you want after close, and who can answer an alarm.
- Interface: photos or drawings of today’s vises, tombstones, and any 52 mm or 96 mm plates.
Ask for the pallet-face layout, plate model, and open questions. The machine builder still owns how the rack moves and docks pallets, magazine options, and cell software. The process owner still has to prove chips, probes, and first-part checks on the real mix.
Questions before you freeze the pallet count
Is a two-pallet APC enough for lights-out work?
One staged extra pallet adds its measured cycle time; 20 minutes or two hours are hypothetical examples. This is a queue estimate, not permission for unattended work. Accept the complete cell, including guarding, load retention, tool life, chips, inspection, fault response, safe states and authorized restart before that run.
How many pallets should a 1–3 machine shop buy first?
There is no fixed count. Add the measured cycle times of the jobs you will actually queue and compare that total with your target unattended hours. Check the tools, fixtures and budget for those jobs. Agree the pallet count with the builder, and accept the complete cell, fault response and restart plan before unattended operation.
Do I need a 240-pocket magazine with a 12-pallet pool?
240 pockets is a hypothetical count, not a 12-pallet requirement. Build the actual inventory of shared tools, job-specific tools and sister tools. Include oversized-tool and blocked-pocket restrictions, then quote the builder’s magazine options against that list.
Can I add a pallet pool later to a two-pallet machine?
Sometimes, if the machine was ordered with the automation interface, spare machine signals (I/O), and space. A later rack is not a drop-in. Ask the builder what the current options include before you treat two-pallet as a cheap first step.
What can NEXTAS review on this decision?
Pallet-face workholding, zero-point plates, vises, and how fixtures move off the table. Send the brief above. The machine builder still owns the rack, magazine, and cell software. NEXTAS is not an OEM cell-controller affiliate.
Pallet buffer review
Send the pallet brief for a workholding review
Send the brief above and name the layout you are considering: two-pallet, a rotary 6-pallet, or a stacked rack pool. NEXTAS can review the workholding interface, plate family, and open fixture questions for your quotation.
Discuss your pallet layout